Bulk Finishing Media Selection Guide for Global Market
Bulk Finishing Media Selection Guide for Global Market Buyers
Quick Answer

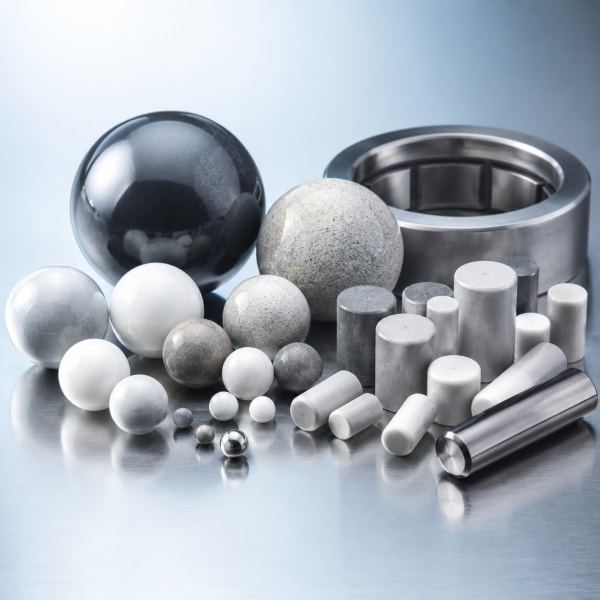
For bulk mass finishing operations in the Global Market, the right grinding and polishing media depends on the material of the workpiece, the desired surface finish, the machine type, the deburring intensity, and the total cost per finished part. Ceramic media is usually preferred for aggressive cutting, deburring, radiusing, and surface preparation of harder metals. Plastic media is often selected for softer metals, aluminum, zinc die castings, and applications where low-density processing reduces part impingement. Steel media, including carbon steel and stainless steel balls, pins, and satellites, is widely used for burnishing, brightening, compacting, and achieving a high-luster surface without heavy stock removal.
A practical selection rule is simple: choose ceramic when you need cut, plastic when you need controlled smoothing, and steel when you need brightness, density, and long service life. Shape selection is equally important. Cones and triangles reach corners and slots, cylinders provide stable edge contact, and balls offer smooth rolling action for burnishing and low scratch risk. In global procurement, the best supplier is not only the one with the lowest media price per kilogram. Buyers should evaluate batch consistency, wear rate, size tolerance, compound compatibility, compliance documentation, packaging strength, lead time reliability, and technical support for process trials.
SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., supports global buyers as both a precision steel ball manufacturer and an integrated supply partner for multi-material spheres and finishing-related media. With manufacturing experience dating back to 1996, three production facilities in Shandong, and supply experience across more than 50 countries, the company serves customers seeking reliable steel balls, stainless steel balls, chrome steel balls, carbon steel balls, and sourcing support for ceramic, plastic, glass, copper, and aluminum spheres. For buyers operating in trade hubs such as Shanghai, Qingdao, Singapore, Hamburg, Rotterdam, Los Angeles, Chicago, Dubai, Mumbai, and São Paulo, a dependable partner helps reduce procurement risk, simplify quality control, and improve landed cost predictability.
The most effective approach is to test media under real process conditions before scaling to bulk shipments. A laboratory result is useful, but production variables such as part loading ratio, water quality, compound concentration, machine amplitude, separation efficiency, and operator handling can change actual performance. Buyers should ask for pilot samples, wear-rate data, safety and compliance documents, and packaging specifications before placing annual contracts.
| Selection Factor | Ceramic Media | Plastic Media | Steel Media | Best Use Case |
|---|---|---|---|---|
| Cutting action | High to very high | Low to medium | Very low | Deburring and edge breaking use ceramic |
| Surface brightness | Matte to semi-bright | Smooth satin | Bright and reflective | Burnishing uses steel |
| Density | Medium | Low | High | Fragile parts often need plastic |
| Wear rate | Moderate | Moderate to high | Very low | Long cycle reuse favors steel |
| Part risk | Medium | Low | Medium to high if misused | Soft alloys often need plastic |
| Typical machine | Vibratory, centrifugal, barrel | Vibratory, barrel | Vibratory burnishing, barrel | Match media to machine energy |
This comparison shows why media choice should be based on process goals rather than catalog names alone. A high-cut ceramic triangle can solve a burr issue but may be too aggressive for decorative aluminum. A polished stainless steel ball can create excellent brightness but cannot replace abrasive media when stock removal is required. The best finishing line often uses several stages: cut-down, smoothing, cleaning, and final burnishing.
Ceramic, Plastic, and Steel Media Choices for Finishing Applications

Mass finishing media is used in vibratory bowls, tub vibrators, centrifugal disc machines, centrifugal barrel systems, rotary barrels, drag finishing units, and automated finishing cells. In the Global Market, these systems are common in automotive component plants in Detroit, Stuttgart, Nagoya, Pune, and Guangzhou; aerospace supply chains around Seattle, Toulouse, Montreal, and Singapore; medical device clusters in Ireland, Switzerland, the United States, and Malaysia; and general hardware manufacturing regions in China, Vietnam, Türkiye, Mexico, Poland, and Brazil.
Ceramic media is made from abrasive grains bonded in a ceramic matrix. Its cutting strength depends on abrasive type, grain size, firing method, porosity, density, and shape. High-cut ceramic media removes burrs quickly and creates consistent edge radii on steel, cast iron, stainless steel, and hard alloys. Fine ceramic media is used for pre-polishing, smoothing, and preparing parts for plating, coating, anodizing, or painting. For large forged or machined components, ceramic media can reduce manual grinding and improve process repeatability.
Plastic media is typically made with polyester, urea, or other resin systems containing abrasive grains. Because it is lighter than ceramic, it reduces impact marks on aluminum, brass, zinc, magnesium, and delicate die-cast parts. Plastic media also helps prevent lodging in certain geometries when the correct shape and size are selected. It is widely used for aerospace aluminum, consumer electronics housings, lighting hardware, plumbing parts, and decorative fittings where a smooth surface is needed without excessive rounding.
Steel media is different because it usually burnishes rather than cuts. Carbon steel balls, stainless steel balls, pins, ballcones, diagonals, and satellites can compact the surface, brighten the part, remove light discoloration, and improve the appearance of stampings, machined components, coin blanks, jewelry findings, and hardware. Stainless steel media is favored where corrosion resistance and clean processing are important. Carbon steel media can be economical, but it requires controlled compound chemistry and drying to prevent rust.
As a precision steel ball manufacturer, SDBALLS has deep experience in steel sphere production, including carbon steel balls, chrome steel balls, and stainless steel balls in grades ranging from G10 to G1000. This precision background is valuable for burnishing and mechanical applications because diameter control, roundness, hardness, surface finish, and material traceability all affect performance. Buyers can review product categories through the company’s steel ball and industrial sphere product range to understand available material options and related supply capabilities.
| Media Type VS Application | Typical Materials Finished | Main Function | Advantages | Limitations |
|---|---|---|---|---|
| Ceramic VS steel machining burrs | Carbon steel, stainless steel, cast iron | Cutting and deburring | Fast burr removal and edge control | May be too aggressive for soft parts |
| Plastic VS aluminum castings | Aluminum, zinc, magnesium | Smoothing and light deburring | Lower impact and reduced part damage | Shorter life than steel media |
| Steel VS decorative hardware | Brass, stainless steel, copper alloys | Burnishing and brightening | Long life and high gloss potential | Not designed for heavy cutting |
| Ceramic fine cut VS pre-plating | Machined components | Surface preparation | Stable satin finish before coating | Needs correct compound control |
| Plastic cone VS aerospace aluminum | Precision aluminum parts | Gentle edge refinement | Reduces peening and distortion | May require longer cycle time |
| Stainless steel ball VS clean burnishing | Medical, food-contact, decorative parts | Polishing and compacting | Clean, corrosion-resistant processing | Higher initial media investment |
The table highlights that each media type has a different operating purpose. A buyer comparing ceramic, plastic, and steel polishing media should define whether the process target is burr removal, surface smoothing, cleaning, brightness, corrosion preparation, or dimensional edge control. Without a clear target, the lowest-cost media can create higher rework, longer cycle time, or inconsistent surface quality.
Selecting the Right Media Shape: Cone, Cylinder, Triangle, or Ball

Shape selection is one of the most underestimated decisions in mass finishing. The media must contact the workpiece surface, flow through the load, separate efficiently, and avoid lodging in holes, slots, threads, and recesses. If the media is too small, it may lodge inside parts and increase labor. If it is too large, it may not reach internal corners. If the shape is too sharp, it can over-cut edges; if it is too round, it may not remove burrs from difficult areas.
Cone-shaped media is useful for holes, corners, recesses, and complex geometries because the tapered end can reach into tighter areas. It is common in both ceramic and plastic formulations. Triangular media provides strong edge contact and is often selected for deburring flat parts, stamped parts, machined edges, and castings. Cylindrical media gives uniform rolling and line contact, making it suitable for general finishing, smoothing, and controlled edge work. Balls are preferred for burnishing, lapping-like rolling action, and applications where low scratch risk and high surface brightness are desired.
Media shape must also be matched with separation equipment. In high-volume plants, automatic screens, magnetic separators, vibratory separation decks, and drying units are used to prevent media carryout. Steel media can often be separated magnetically when carbon steel is used, but stainless steel may require mechanical separation depending on alloy and magnetic response. Plastic and ceramic media require size-based separation, so the media must remain clearly different from part openings and part dimensions.
| Shape | Best Contact Style | Typical Strength | Risk to Watch | Shape VS Alternative |
|---|---|---|---|---|
| Cone | Point and side contact | Reaches recesses and holes | Can lodge if too small | Cone VS ball: better access, less burnish |
| Cylinder | Line contact | Stable general finishing | May bridge in narrow slots | Cylinder VS triangle: smoother, less aggressive |
| Triangle | Edge and face contact | Good deburring of edges | Can over-radius delicate parts | Triangle VS cone: stronger edge action |
| Ball | Rolling point contact | Bright burnishing | Limited cutting ability | Ball VS ceramic: polish, not heavy deburr |
| Satellite | Multiple curved contacts | Good steel burnishing coverage | Geometry must suit parts | Satellite VS ball: more surface interaction |
| Angle-cut cylinder | Edge plus rolling contact | Versatile cutting and finishing | Size selection is critical | Angle-cut VS straight: better corner access |
In practice, buyers should request a lodging analysis before confirming bulk media. This means checking the smallest holes, blind cavities, slots, threads, and channels on the component drawing. For example, if a stamped bracket has a 6 mm slot, a 5 mm cone may lodge, while an 8 mm triangle may separate cleanly. If a machined valve body has multiple cross-holes, media testing should include pressure flushing and inspection after processing. The correct media shape reduces hidden labor, prevents customer complaints, and keeps automated finishing cells running without interruption.
How to Evaluate Suppliers for Consistent Mass Finishing Media Quality
Supplier evaluation for mass finishing media should focus on repeatability. In global purchasing, a supplier may pass the first sample trial but fail during continuous shipments if raw material control, firing conditions, grading, packaging, or inspection systems are weak. Quality consistency is especially important for multinational manufacturers that run the same finishing process in several plants, such as facilities in Mexico, Germany, China, India, and the United States.
Buyers should evaluate technical capability first. A reliable supplier should understand the relationship between media density, abrasive grade, hardness, wear rate, cutting rate, surface roughness, and compound chemistry. For steel media and precision steel balls, supplier expertise should include material selection, heat treatment, grinding, lapping, polishing, grading, and inspection. SDBALLS’ technological capabilities are supported by decades of steel ball manufacturing knowledge, quality systems, and inspection processes used for bearing, automotive, hardware, grinding, and mechanical applications. Its work with grades from G10 to G1000 reflects a manufacturing culture where dimensional consistency and surface quality matter.
Manufacturing capability is the second factor. Buyers should ask whether the supplier operates its own production lines, how it controls capacity, whether it can support annual contracts, and how it handles peak-season demand. SDBALLS operates three production facilities with annual output exceeding 5,000 tons, which gives global customers a more stable supply foundation than purely trading-based sourcing. The company’s location in Tai’an City, Shandong Province, provides access to China’s mature industrial supply chain and export routes through Qingdao, Shanghai, Tianjin, and Ningbo.
Service capability is the third factor. Global buyers need responsive communication, export documentation, sample coordination, after-sales analysis, and support for mixed material sourcing. SDBALLS serves customers in more than 50 countries and provides global sales support, including assistance for customers seeking consolidated procurement of steel, ceramic, plastic, glass, copper, and aluminum spheres. Buyers can learn more about the company’s background through its manufacturer profile and global supply experience.
| Supplier Criterion | Strong Supplier | Weak Supplier | Impact on Buyer | Evaluation Method |
|---|---|---|---|---|
| Batch consistency | Stable size, density, cut, and finish | Large variation between lots | Predictable cycle times | Compare sample and bulk lot data |
| Quality certification | ISO 9001, ISO 14001, automotive systems where relevant | No documented system | Lower audit risk | Request valid certificates |
| Technical support | Helps with shape, media, and process selection | Only quotes price | Fewer trial failures | Review response quality |
| Manufacturing control | Own production and inspection | Unclear subcontracting | Better traceability | Ask for process flow and inspection plan |
| Export experience | Ships to multiple regions | Limited documentation experience | Fewer customs delays | Check references and shipping records |
| Corrective action | Provides root-cause analysis | Offers only replacement without analysis | Long-term improvement | Ask for sample 8D or complaint process |
This supplier comparison is important because finishing media is a process input, not a simple consumable. Inconsistent media can change roughness, brightness, cycle time, scrap rate, and labor cost. A professional supplier should help the buyer protect the entire finishing process rather than only deliver bags, drums, or pallets.
Cost-Per-Part Analysis and Media Consumption Rate Optimization
Bulk finishing media should be evaluated by cost per finished part, not only by purchase price per kilogram. A cheaper media with high wear rate, high sludge generation, poor cutting efficiency, or frequent replacement can cost more in production than a higher-priced media with stable performance. Cost-per-part analysis includes media consumption, compound usage, water and wastewater cost, electricity, machine depreciation, labor, rework, scrap, separation time, drying time, and packaging of finished parts.
Media consumption rate is calculated by measuring how much media is lost or worn down during a defined number of cycles. For abrasive ceramic and plastic media, wear is expected because the media breaks down while cutting. For steel media, wear is usually much lower, but corrosion loss, carryout, and contamination can increase cost. A good production team records media level, cycle time, surface roughness, part weight, compound concentration, and wastewater condition. Over time, this data shows whether the process is stable.
Optimization begins with media-to-part ratio. Too little media can cause part-on-part damage and inconsistent finishing. Too much media can reduce throughput and increase cycle time. Common ratios vary by application, but many vibratory processes use a media-heavy load to protect parts and maintain contact. Machine energy also matters. High-energy centrifugal systems may use smaller media and shorter cycles, while tub vibrators may require longer processing for heavy components.
Another cost driver is wastewater and sludge. Ceramic and plastic media generate fines that enter the process solution. If the plant operates in regions with strict discharge rules, such as the European Union, California, Japan, South Korea, or Singapore, waste treatment cost can be significant. Using the correct media grade and compound can reduce foam, odor, suspended solids, and disposal burden. Steel burnishing media may reduce abrasive sludge, but it still requires cleaning compounds and rust-control management.
| Cost Element | Low-Cost Media Risk | Optimized Media Benefit | Measurement | Cost VS Value Lesson |
|---|---|---|---|---|
| Media wear | Fast breakdown and frequent refill | Lower consumption per batch | Kg lost per 1,000 parts | Cheap purchase can be costly in use |
| Cycle time | Slow cutting requires longer runs | Higher output per machine hour | Minutes per batch | Faster process improves capacity |
| Rework | Inconsistent finish creates rejects | Stable surface quality | Rework percentage | Quality saves labor |
| Wastewater | High sludge and unstable chemistry | Cleaner process solution | Solids and treatment cost | Sustainability affects cost |
| Separation labor | Lodged media increases inspection | Clean separation | Labor minutes per lot | Shape selection affects productivity |
| Machine wear | Overly aggressive media damages liners | Balanced process energy | Liner replacement interval | Total cost includes equipment life |
To optimize media consumption, buyers should run controlled trials using the same part quantity, machine setting, compound concentration, and cycle time. Record initial and final media weight, part finish, burr removal, and wastewater condition. The winning media is the one that meets the surface specification with the lowest total process cost and acceptable lead time. In procurement negotiations, ask suppliers for annual volume pricing, stable packaging units, and technical support for process improvement.
OEM Customization for Specialized Polishing Media Formulations
OEM customization is valuable when standard catalog media cannot meet a specific finishing target. Specialized polishing media formulations may be needed for aerospace parts requiring controlled edge radius, medical components requiring clean processing, electric vehicle parts requiring stable pre-coating surface, jewelry components requiring high brightness, or firearm and outdoor equipment parts requiring corrosion-resistant burnishing. Customization can involve material, abrasive grade, density, hardness, shape, size, color coding, packaging, and documentation.
For ceramic and plastic media, OEM customization often focuses on cutting speed, surface smoothness, wear rate, and residue control. A high-cut formulation may use more aggressive abrasive grains, while a fine finishing formulation may use smaller abrasive particles and a smoother bond structure. For steel balls and steel burnishing media, customization may include carbon steel, chrome steel, stainless steel, hardness range, plating, annealing, passivation, and precision grade. SDBALLS’ background in precision steel ball manufacturing allows it to support technical discussions around steel material selection, surface finish, hardness, and grade requirements for industrial applications.
OEM projects should begin with clear application data. The buyer should provide part drawings, material grade, hardness, burr description, incoming roughness, target roughness, required edge radius, machine type, batch size, compound type, water quality, and current process problems. If the buyer cannot disclose drawings, representative samples or simplified geometry information can still help. For multinational buyers, it is also useful to specify whether the same media will be used in plants across different regions, because water hardness, operator practices, and machine models may differ.
SDBALLS also acts as an integrated supply partner for buyers seeking multi-material sphere sourcing beyond steel balls, including plastic, glass, ceramic, copper, and aluminum options. This is useful for global procurement teams that want fewer supplier interfaces and more consistent communication. Technical buyers can review the company’s quality and technical control approach to understand how inspection and process discipline support long-term supply.
In OEM media development, timelines should include sample design, pilot production, trial shipment, customer testing, feedback, adjustment, and bulk production. Buyers should avoid approving custom media based on visual finish alone. A complete approval should include roughness measurement, burr inspection, dimensional review, corrosion testing where needed, cleanliness testing, wastewater impact, and separation performance. Once approved, specifications should be written into a purchasing document so every shipment follows the same standard.
ISO 14001 and RoHS Compliance in Grinding Media Manufacturing
Compliance expectations are rising across the Global Market. Buyers increasingly ask whether grinding media, polishing media, steel balls, and related process materials align with environmental management systems and restricted substance requirements. ISO 14001 demonstrates that a manufacturer has an environmental management framework for monitoring impacts, improving processes, and maintaining compliance obligations. RoHS relates to restrictions on hazardous substances commonly associated with electrical and electronic equipment supply chains, but many industrial buyers request RoHS statements as part of broader responsible sourcing programs.
SDBALLS maintains ISO 14001 certification together with ISO 9001 and IATF 16949, supporting customers that require structured quality and environmental systems. For buyers serving automotive, electronics, medical, and export-oriented hardware markets, these certifications can simplify supplier qualification. Compliance does not replace product testing, but it shows that the supplier understands controlled documentation, audits, corrective actions, and process management.
Environmental requirements are becoming more important in 2026 and beyond. The European Union continues to strengthen sustainability expectations through carbon reporting, chemical control, and circular economy policies. North American buyers are asking more questions about supply chain transparency and responsible manufacturing. Asian manufacturing hubs such as Japan, South Korea, Singapore, and China are improving wastewater and emissions controls. Global brands are also pushing suppliers to reduce sludge, improve packaging recyclability, and provide clearer material declarations.
For mass finishing operations, sustainability is not only a certificate. It includes lower media consumption, longer service life, reduced wastewater contamination, efficient logistics, recyclable packaging, and safer compounds. Steel burnishing media can offer long life in the right application, while optimized ceramic or plastic formulations can reduce rework and energy use by shortening cycle times. Buyers should request safety data sheets, RoHS declarations where applicable, material composition statements, and information about packaging waste.
The 2026 trend is toward data-backed sustainability. More buyers will expect suppliers to provide measurable indicators such as batch traceability, media wear rate, packaging material details, and transport efficiency. Digital quality records, QR-code traceability, automated inspection, and AI-supported process optimization will become more common in finishing supply chains. Suppliers that combine manufacturing stability with documentation readiness will be better positioned to serve global OEMs.
Lead Time, Packaging, and Logistics for Bulk Media Shipments
Lead time and logistics can determine whether a finishing line runs smoothly or faces costly downtime. Bulk media shipments are heavy, and freight decisions affect landed cost. Buyers importing into North America may use ports such as Los Angeles, Long Beach, Houston, New York, Savannah, or Vancouver. European buyers may route through Rotterdam, Hamburg, Antwerp, Gdańsk, or Valencia. Middle East and Africa shipments may move through Jebel Ali, Dammam, Durban, or Mombasa. Asia-Pacific buyers often use Singapore, Busan, Yokohama, Port Klang, Laem Chabang, Manila, and Sydney. South American customers may receive through Santos, Buenos Aires, Callao, or Cartagena.
Packaging must protect the media from moisture, breakage, contamination, and handling damage. Ceramic and plastic media are often packed in woven bags, cartons, drums, or palletized bulk units. Steel balls and steel media may require oiling, anti-rust paper, sealed bags, drums, cartons, or wooden cases depending on material and route. Stainless steel media is less rust-sensitive than carbon steel, but clean packaging is still important. For ocean freight, humidity control and pallet strength should be considered, especially for long routes crossing tropical climates.
Buyers should confirm packaging unit weight before ordering. Operators must be able to lift, pour, and store media safely. A 25 kg bag may be practical for manual handling, while drums or big bags may suit automated plants with forklifts and cranes. Labels should include product name, size, batch number, net weight, gross weight, country of origin, and handling instructions. For customs clearance, documents may include commercial invoice, packing list, bill of lading, certificate of origin, compliance declaration, and insurance documents.
SDBALLS’ service capabilities include export coordination for global customers, support for bulk shipments, and communication around packaging and delivery requirements. Its Shandong manufacturing base is well positioned for container shipping through major Chinese ports. For urgent requirements, buyers should discuss available stock, partial shipments, air freight for samples, and production scheduling. For annual demand, forecast sharing helps stabilize production and reduce emergency freight cost.
A good logistics plan includes safety stock. Finishing media consumption may increase when part mix changes, machine settings change, or operators extend cycle time. International shipping can also be affected by port congestion, weather, geopolitical disruptions, container shortages, customs inspections, and holiday periods such as Chinese New Year, Golden Week, Christmas, Ramadan, and regional public holidays. Global buyers should maintain a reorder point based on actual consumption and shipping lead time.
Our Company
SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., is a professional precision steel ball manufacturer and integrated supply partner based in Tai’an City, Shandong Province, China. Since 1996, the company has built manufacturing experience in carbon steel balls, chrome steel balls, stainless steel balls, and related industrial sphere products. Its products serve bearing systems, automotive components, caster wheels, sliding systems, ball transfer units, hardware, grinding applications, and outdoor markets.
From a technological perspective, SDBALLS focuses on precision, material control, and application suitability. Steel ball performance depends on roundness, surface finish, hardness, size tolerance, and cleanliness. These details affect noise, wear, rolling performance, burnishing results, and mechanical reliability. The company’s experience with grades from G10 to G1000 allows buyers to select products for high-precision and general industrial uses. For customers requiring finishing media or polishing-related spheres, this technical foundation supports better conversations about application fit.
From a manufacturing perspective, SDBALLS operates three production facilities with annual capacity exceeding 5,000 tons. This scale supports stable supply for distributors, OEMs, and industrial users buying in bulk. The company manufactures core steel ball products while also supporting integrated sourcing for plastic, glass, ceramic, copper, and aluminum spheres. This combined model is useful for purchasing teams that need reliable steel ball production and flexible sourcing of complementary materials.
From a service perspective, SDBALLS supports customers across more than 50 countries with a dedicated global sales team and customer-focused communication. The company provides assistance for product selection, export packaging, documentation, and long-term cooperation. It also offers lead-free steel shot solutions for hunting and outdoor markets, including annealed and plated options designed for CIP-compliant hardness requirements in EU and US markets. For application ideas across industries, buyers can explore industrial applications for steel balls and spheres.
Global buyers choose SDBALLS when they need a supplier that understands both manufacturing discipline and international procurement. Whether the requirement is stainless steel balls for corrosion-resistant burnishing, chrome steel balls for mechanical assemblies, carbon steel balls for hardware, or sourcing support for multi-material spheres, the company aims to provide consistent quality, reliable delivery, and practical support.
Frequently Asked Questions
What is the fastest way to choose between ceramic, plastic, and steel media?
Start with the process goal. If you need burr removal or edge breaking, test ceramic media. If you need gentle smoothing on aluminum, zinc, or soft alloys, test plastic media. If you need brightness, compacting, and long media life rather than cutting, test steel media. Always confirm through production trials before bulk purchasing.
Which media shape is best for preventing lodging?
There is no universal shape that prevents lodging in every part. The safest choice depends on the holes, slots, recesses, and part geometry. Select media larger than critical openings or shaped so it cannot become trapped. A lodging review should be part of every media approval process.
Is steel media better than ceramic media?
Steel media and ceramic media serve different purposes. Steel media is excellent for burnishing and brightening, while ceramic media is better for cutting and deburring. Steel media usually lasts much longer, but it cannot replace abrasive media when significant burr removal is required.
How do I calculate media consumption rate?
Weigh the media before a defined production period, run a known number of cycles or parts, remove contamination and moisture as much as practical, then weigh the remaining media. Divide the loss by the number of finished parts or machine hours. Track this over time to identify process changes.
Why is cost per part more important than price per kilogram?
Price per kilogram ignores cycle time, wear rate, rework, wastewater, labor, separation efficiency, and machine utilization. A higher-priced media may produce a lower cost per part if it finishes faster, lasts longer, and reduces rejects.
What documents should global buyers request from a media supplier?
Common documents include quotation, product specification, safety data sheet where applicable, quality certificate, ISO certificates, RoHS declaration if needed, packing list format, certificate of origin, and batch traceability information. Regulated industries may require additional documentation.
Can one media type work for all parts in a factory?
Usually not. A factory producing different materials and geometries often needs several media types and sizes. For example, machined steel parts may need ceramic cutting media, aluminum housings may need plastic media, and decorative stainless parts may need stainless steel burnishing balls.
What are the most important 2026 trends in mass finishing media?
Key trends include lower sludge processes, longer-life media, improved RoHS and environmental documentation, digital batch traceability, automated finishing cells, AI-supported process optimization, recyclable packaging, and stronger supplier audits focused on sustainability and supply chain resilience.
How should I plan bulk shipment lead time?
Plan lead time by combining production time, packaging time, export customs, ocean or air freight, import clearance, inland transport, and safety stock. For ocean freight, buyers should consider port congestion and holiday periods. Annual forecasts help suppliers reserve capacity and reduce emergency shipping.
Why consider SDBALLS for finishing-related media and steel balls?
SDBALLS combines more than 30 years of manufacturing experience, three production facilities, quality certifications, global export service, and broad steel ball capabilities. It also supports integrated sourcing for multi-material spheres, helping global buyers simplify procurement and improve supply consistency.
About the Author
We are SD Ball, a professional manufacturer dedicated to delivering high-precision steel ball solutions worldwide. With years of expertise, we specialize in advanced production processes, strict quality control, and customized solutions to support diverse industrial applications. From material selection to final inspection, we provide reliable products and consistent performance to help our clients achieve higher efficiency, durability, and product quality.
Share
Product Category
Related Articles
-
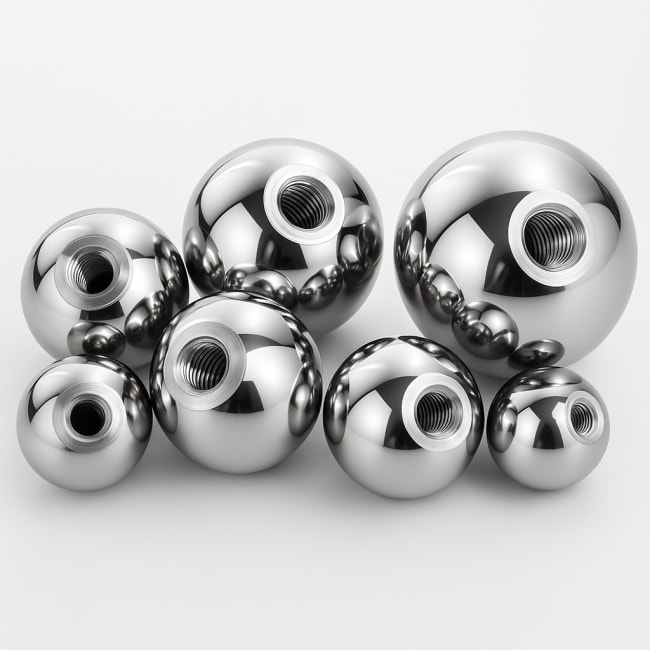
Global Market Guide to Industrial Threaded Ball Sourcing
For buyers in the Global Market, the best threaded ball supplier is not simply the lowest-priced seller of drilled spheres. A reliable partner should understand thread standards from M3 to M20, ball diameter tolerances, concentricity, surface finish, hardness, corrosion resistance, packaging protection, inspection documentation, and the way threaded balls are used in fixture, mounting, automation, positioning, and mechanical assembly systems. The correct supplier should also support both standard and custom production, including internal threads, external threaded studs, blind holes, through holes, tapped holes, cross drilling, special plating, polishing, heat treatment, and multi-material sourcing.Threaded balls are used where a spherical contact surface, pivot point, locating feature, handle end, clamping element, or adjustable mount must be combined with a mechanical thread. In industrial fixtures, they are often selected for modular tooling, welding jigs, inspection gauges, robotic end-of-arm tooling, transfer systems, and machine positioning assemblies. A procurement team should evaluate four factors first: thread specification, ball material, precision grade, and supplier process control.In global trade hubs such as Shanghai, Qingdao, Ningbo, Singapore, Rotterdam, Hamburg, Dubai, Los Angeles, Chicago, and Mumbai, buyers commonly compare suppliers based on repeatability, engineering communication, export experience, quality certification, and the ability to consolidate multiple spherical components. SDBALLS Industry Corp supports this type of sourcing need by combining more than 30 years of precision steel ball manufacturing experience with integrated supply capability for steel, stainless steel, chrome steel, carbon steel, and other sphere materials. Buyers can review the company background through the SDBALLS company profile and evaluate product families through its industrial ball product range.In short, when sourcing threaded balls for industrial fixture and mounting systems, ask the supplier for a clear drawing review, material certificate, thread gauge confirmation, tolerance plan, sample approval process, production capacity statement, packaging method, and realistic lead time. For custom threaded ball orders, also confirm whether the supplier can control drilling depth, thread perpendicularity, thread engagement length, burr removal, plating thickness, and final surface appearance.Thread specification is the foundation of a successful threaded ball assembly. A ball can meet the correct diameter and material requirement, but if the thread is inaccurate, shallow, misaligned, oversized, undersized, or damaged by burrs, the complete fixture may fail during installation. For Global Market buyers, the most common metric thread sizes range from M3 to M20, while inch thread options such as UNC, UNF, and special customer-defined profiles are also used in North America and international machinery projects.M3 to M6 threaded balls are often used in small fixtures, miniature adjustment assemblies, measuring devices, camera mounts, electronics test fixtures, and light-duty handles. M8 to M12 sizes are widely used in industrial clamps, positioning balls, modular jigs, automotive checking fixtures, and machine guards. M16 to M20 threaded balls are selected for heavier load applications, structural mounting, lifting-related positioning components, and large industrial equipment where the connection must resist vibration and repeated adjustment.The choice between a blind tapped hole and a through threaded hole depends on assembly design. A blind hole gives a clean external appearance and prevents the mating screw from passing through the ball. A through hole may be easier to clean, inspect, and assemble, especially where longer bolts are used. For fixture systems, thread engagement length is critical because many failures occur when the thread depth is too short for the applied torque or vibration environment.Thread SizeTypical Ball Diameter RangeCommon UseStandard OptionCustom OptionKey Buying CheckM36 mm to 12 mmMiniature locating and adjustment partsBlind tapped holeMicro through holeCheck thread depth and burr controlM48 mm to 16 mmLight fixture componentsMetric coarse threadFine pitch threadConfirm perpendicularityM510 mm to 20 mmSmall knobs and positioning pointsInternal threadThreaded stud insertedCheck pull-out strengthM612 mm to 25 mmAutomation mounts and clampsBlind or through tapped holeCross-drilled configurationConfirm thread gauge resultM8 to M1218 mm to 40 mmIndustrial fixtures and toolingMetric ISO threadUNC or UNF equivalentReview torque requirementM16 to M2035 mm to 80 mm or largerHeavy-duty positioning assembliesDeep internal threadSpecial pitch or dual threadCheck concentricity and loadThis table shows that thread selection cannot be separated from ball diameter, material strength, and application load. A small ball with a large thread may not leave enough wall thickness after drilling, while a large ball with a shallow thread may fail to provide adequate engagement. For OEM projects, buyers should send 2D drawings or 3D models that identify thread size, pitch, tolerance, hole type, thread depth, chamfer, surface finish, and inspection method.Compared with standard threaded ball items, custom thread options allow better design integration but require stricter engineering review. A standard M8 stainless steel threaded ball may be available faster, but a custom M8 x 1.0 fine pitch ball with passivation, special polishing, and controlled concentricity will need sample production and approval. For buyers serving multiple plants across Europe, the United States, Southeast Asia, and the Middle East, standardization of thread families can reduce inventory complexity and shorten maintenance response time.Material selection affects load capacity, corrosion resistance, machinability, cost, magnetic behavior, wear resistance, surface appearance, and long-term reliability. Threaded balls for fixture applications are commonly produced from carbon steel, chrome steel, stainless steel, brass, aluminum, plastic, and sometimes ceramic or specialty alloys. For industrial buyers, the best material is the one that matches the working environment, not necessarily the hardest or most expensive material.Carbon steel balls are cost-effective and suitable for general fixtures, hardware, knobs, and indoor mounting systems. They can be zinc plated, nickel plated, black oxidized, or otherwise surface treated to improve appearance and corrosion resistance. Chrome steel provides high hardness and wear performance and is often selected where strength and dimensional stability matter. Stainless steel is preferred for food equipment, medical fixtures, marine environments, chemical plants, outdoor systems, and clean assembly areas.Different stainless grades should not be treated as identical. AISI 304 stainless steel offers general corrosion resistance and good availability. AISI 316 stainless steel is better for coastal, marine, chemical, and high-humidity environments because of its molybdenum content. AISI 420 or 440C stainless steel can provide higher hardness, but corrosion resistance and machining behavior differ from 304 and 316. For threaded balls, the drilling and tapping process must also be considered, because very hard materials may require special tooling or pre-machining strategy.MaterialStrengthCorrosion ResistanceMachinabilityBest ForVS AlternativeCarbon steelMedium to highLow without platingGoodCost-sensitive fixturesLower corrosion resistance vs stainless steelChrome steelHighModerate with protectionModerate after hardeningWear-resistant locating partsHarder than carbon steel but less corrosion-resistant than 316304 stainless steelMediumGoodGoodGeneral industrial and clean environmentsLower marine resistance vs 316316 stainless steelMediumVery goodModerateMarine, chemical, outdoor applicationsHigher cost vs 304BrassLow to mediumGood in many environmentsExcellentDecorative, electrical, low-friction componentsSofter than steelAluminumLow to mediumGood with anodizingExcellentLightweight assembliesLower thread strength vs steelPlastic or polymerLowExcellent against many chemicalsGoodLight-duty, non-marring fixturesMuch lower load capacity vs metalThe table highlights a common sourcing decision: carbon steel vs stainless steel. Carbon steel is economical for large fixture fleets in dry workshops, but stainless steel is usually better for environments near ports, food plants, pharmaceutical factories, and outdoor installations. In cities such as Rotterdam, Hamburg, Houston, Singapore, Busan, and Dubai, salt air, humidity, and chemical exposure often justify stainless steel even when the initial price is higher.SDBALLS has long-term experience producing carbon steel balls, chrome steel balls, and stainless steel balls in multiple grades. This manufacturing knowledge is important for threaded ball projects because the base sphere quality affects drilling stability, finished appearance, and final assembly consistency. In addition, SDBALLS can help global buyers consolidate sourcing for other spherical materials when a fixture project needs plastic, glass, ceramic, copper, or aluminum balls together with steel components.Tolerance is not only a drawing number; it is the difference between a fixture that repeats accurately and one that causes alignment problems. For threaded ball assemblies, buyers should define ball diameter tolerance, sphericity, surface roughness, thread tolerance class, hole position, thread depth, perpendicularity, concentricity, and visual acceptance criteria. If the threaded ball is used as a locating element, pivot point, ball transfer contact, or measuring fixture component, the precision level becomes especially important.Steel balls are often described by precision grades such as G10, G16, G25, G40, G100, G200, G500, and G1000, depending on the required dimensional accuracy and surface condition. High precision grades are used in bearing, automotive, and measuring applications. General industrial fixture balls may not require the same grade as bearing balls, but they still need consistent diameter, clean thread formation, and stable surface finish. A very precise ball can lose functional value if the drilled thread is off-center or if a burr remains at the hole entrance.For threaded ball assemblies, the production route usually includes blank ball selection, heat treatment if required, grinding or polishing, drilling, tapping, deburring, cleaning, surface treatment, final inspection, and packaging. Each operation can influence final tolerance. For example, plating can slightly change thread dimensions, so suppliers must decide whether thread inspection is performed before or after plating. For high-value OEM projects, final inspection after all surface processes is preferred.RequirementGeneral GradePrecision GradeInspection MethodRisk If IgnoredRecommended Buyer ActionBall diameterModerate toleranceTight toleranceMicrometer or gaugeLoose fit or assembly interferenceDefine tolerance on drawingSphericityAcceptable for handlesCritical for locatingRoundness measurementPoor contact repeatabilitySelect suitable ball gradeThread accuracyStandard gauge passControlled class fitGo/no-go thread gaugeAssembly failureRequire gauge reportHole concentricityVisual and basic checkMeasured runoutFixture or CMMMisalignment in mountingState datum referenceSurface finishPolished or platedRa-controlled finishVisual or profilometerWear or poor appearanceAgree sample standardBurr controlDeburred edgeControlled chamferVisual magnificationThread jamming and injurySpecify chamfer sizeHardnessMaterial-basedHeat-treatment controlledHardness testerPremature wear or crackingRequest material and hardness recordThis table explains why precision is a system-level issue. A supplier may quote a low price for a standard ball, but if no thread gauge inspection, burr control, or packaging protection is included, the total cost can rise through rework, production stoppages, and field complaints. Buyers should compare standard tolerance vs precision tolerance based on application risk. A ball used as a decorative handle end does not need the same control as a ball used in a robotic positioning fixture.SDBALLS supports precision manufacturing from G10 to G1000 across different steel ball categories. Its quality system, supported by IATF 16949, ISO 9001, and ISO 14001 certifications, gives buyers a structured base for discussing inspection requirements. More detail on quality control and technical standards can be reviewed through the quality and technical capability page.OEM threaded ball projects often require more than a single tapped hole. Custom requirements may include double-ended threaded balls, partial through holes, angled holes, cross holes, combined threaded and smooth bores, press-fit inserts, welded studs, special chamfers, anti-rotation flats, laser marking, color coding, plating, passivation, black oxide, electropolishing, or special packaging for automated assembly lines. Leading suppliers must be able to interpret drawings and advise when a design is difficult to manufacture reliably.A strong OEM supplier will ask practical questions before quoting: What is the ball diameter? What is the thread size and pitch? Is the hole blind or through? What is the minimum thread engagement? What material and hardness are required? Is plating applied before or after tapping? Does the threaded ball need to pass salt spray testing? What is the annual quantity? Will the part be installed manually or by automation? Does the buyer require PPAP, first article inspection, or batch traceability?Technological capability matters because drilling a curved surface is different from drilling a flat plate. The drill must be accurately centered and stabilized to prevent walking. The tapping operation must avoid thread tearing, poor chip removal, or broken taps. For hardened steel balls, suppliers may need special pre-drilling, annealing, EDM, carbide tools, or modified process flow. For stainless steel balls, heat buildup and galling must be controlled during tapping.Custom FeaturePurposeManufacturing ChallengeStandard VS CustomInspection FocusTypical ApplicationBlind internal threadClean external appearanceDepth controlStandard for many sizesThread depthKnobs and fixture ballsThrough threadFlexible bolt lengthBurrs at both openingsMore custom in small ballsDeburring and gauge passMounting assembliesExternal threaded studFast installationStud strength and alignmentCustom assemblyPull-out and runoutHandles and positioning partsCross drillingPinning or lockingHole intersection burrsCustomInternal burr removalLocking fixturesFine pitch threadPrecise adjustmentTool wear and gauge controlCustomPitch accuracyMeasuring and alignment devicesSpecial coatingCorrosion or appearanceThickness on threadCustomPost-coating thread fitOutdoor equipmentLaser markingTraceabilityCurved surface markingCustomReadabilityOEM batch controlThe table shows the difference between buying catalog parts and developing engineered threaded ball components. A standard part may solve basic needs quickly, while a custom part improves design performance but requires technical communication. For Global Market OEM buyers, it is useful to approve samples under real assembly conditions before releasing mass production. Testing should include torque installation, vibration exposure, corrosion exposure where relevant, and repeated assembly cycles.SDBALLS’ manufacturing base in Shandong, China, provides stable steel ball production capacity, while its integrated supply model helps buyers coordinate secondary operations and multi-material sphere requirements. This is especially valuable for OEMs that need one supplier to manage both standard balls and custom drilled or threaded ball projects for global plants.Supplier selection should include an audit of quality systems, production capacity, process control, export documentation, and communication reliability. A threaded ball supplier may look acceptable from product photos, but a deeper audit reveals whether it can maintain repeatability over months and years. For global companies sourcing into Europe, North America, South America, the Middle East, and Asia-Pacific, supplier stability is often more important than one-time pricing.A quality audit should review incoming material control, heat treatment control, ball forming and grinding processes, drilling and tapping equipment, inspection tools, gauge calibration, nonconforming product handling, packaging standards, traceability, and corrective action procedures. If threaded balls are used in automotive, medical, food machinery, or high-reliability automation, buyers may request more formal documentation such as material certificates, dimensional reports, salt spray results, RoHS or REACH declarations where applicable, and process flow charts.Production capacity assessment should not only ask for annual tonnage. Buyers should determine whether the supplier has enough machines, skilled operators, tooling, inspection staff, and subcontractor control for secondary processes. For example, a supplier may have excellent ball grinding capacity but limited tapping capacity. If the project requires 100,000 custom M8 stainless steel threaded balls per quarter, drilling and tapping throughput may become the bottleneck rather than ball manufacturing.Audit AreaWhat to CheckGood Supplier EvidenceWarning SignBuyer BenefitGlobal Market RelevanceCertificationISO and industry systemsValid certificatesExpired or unclear documentsReduced quality riskImportant for multinational buyersMaterial controlSteel grade and sourceTraceable recordsMixed or unidentified stockConsistent performanceNeeded for customs and complianceThread inspectionGo/no-go gaugesCalibrated gaugesNo gauge recordReliable assemblyCritical for OEM programsCapacityMonthly output and bottlenecksClear production planUnrealistic promisesStable deliveryUseful for global rolloutsPackagingRust, impact, and mix protectionLabeled and protected cartonsBulk damage riskLower receiving defectsImportant for sea freightCorrective actionComplaint handlingRoot cause reportsBlame without solutionLong-term improvementSupports strategic sourcingExport experienceDocuments and logisticsShipments to many countriesLimited customs knowledgeSmoother importingEssential for cross-border buyersSDBALLS operates three production facilities with annual capacity exceeding 5,000 tons, serving customers in more than 50 countries. This manufacturing scale helps support both standard ball demand and customized supply programs. The company’s experience with bearing, automotive, hardware, grinding, outdoor, and mechanical systems gives it a broad process background for industrial buyers.When auditing suppliers in China, buyers often consider proximity to ports such as Qingdao, Shanghai, Ningbo, and Tianjin. For SDBALLS in Tai’an, Shandong Province, access to northern China industrial supply chains and Qingdao port supports export logistics to Europe, North America, Southeast Asia, Australia, and the Middle East.Lead time and minimum order quantity depend on material, diameter, thread size, precision grade, surface treatment, sample requirements, and current production schedule. Standard threaded balls may ship quickly if the supplier has stock or can machine from common ball sizes. Custom threaded balls require drawing review, tooling preparation, sample production, inspection, approval, mass production, surface treatment, final inspection, and export packing.For standard carbon steel or stainless steel threaded balls, buyers may see lead times from one to four weeks depending on quantity. For custom OEM parts, four to eight weeks is more realistic, especially when plating, passivation, black oxide, laser marking, salt spray testing, or special inspection reports are required. Very large orders or special materials may require longer planning. Sea freight adds additional transit time, while air freight can solve urgent needs at higher cost.MOQ is usually lower for standard sizes and higher for custom specifications. If a buyer requests a rare ball diameter, special thread pitch, low-volume coating, or nonstandard material, the supplier must cover setup cost, tooling cost, machine adjustment, and inspection time. A practical approach is to start with prototypes or pilot batches, then move to annual blanket orders with scheduled releases.Standard vs custom purchasing should be evaluated by total cost. Standard products reduce lead time and inventory risk, while custom products may reduce assembly labor, improve performance, and protect the buyer’s design. For multinational companies, a dual strategy often works best: use standard threaded balls for maintenance and general fixtures, and use custom threaded ball assemblies for critical production tooling.SDBALLS’ service capability includes export support, engineering communication, stable supply planning, and sourcing consolidation. Its global sales team and US business support help international buyers manage time zone communication, sample feedback, and long-term order planning. This is useful for companies with plants in Detroit, Monterrey, Stuttgart, Milan, Pune, Bangkok, Ho Chi Minh City, and São Paulo that need consistent components across regions.Threaded balls are small components, but they support many important industrial functions. In automation systems, they can be used as adjustable contact points, end stops, sensor mounts, spherical handles, pivot elements, and alignment supports. In positioning systems, they provide repeatable contact surfaces for clamps, gauges, and locating fixtures. In mechanical assembly, they serve as practical connection points where smooth spherical geometry reduces interference and improves handling.In automotive manufacturing, threaded balls may appear in checking fixtures, welding jigs, robotic tooling, inspection arms, and assembly stations. In electronics manufacturing, smaller threaded balls can support test fixtures, adjustable stops, and compact mechanical mounts. In packaging equipment, stainless threaded balls are used where cleaning and corrosion resistance matter. In medical device manufacturing, polished stainless surfaces are preferred for cleanability and appearance. In marine and outdoor equipment, 316 stainless steel or coated carbon steel can improve life in humid and salt-exposed conditions.Case study 1: An automation integrator in Germany needed M8 stainless threaded balls for adjustable stops in a packaging line. The original low-cost parts had inconsistent thread depth, causing installation delays. After switching to a supplier that provided thread gauge inspection and controlled deburring, assembly time improved and maintenance complaints decreased.Case study 2: A fixture builder in Mexico serving automotive plants required custom M10 balls with blind threaded holes and black oxide finish. The key issue was coating thickness inside the thread. The approved process included post-coating gauge checks, which reduced rejected parts at the customer’s receiving inspection.Case study 3: A marine equipment distributor near Rotterdam requested 316 stainless threaded balls for outdoor mounting systems. Although the unit price was higher than 304 stainless steel, corrosion complaints dropped significantly in coastal applications. The project demonstrated why material selection must reflect real working conditions.More examples of mechanical and industrial use can be explored through the SDBALLS application fields, which cover bearing systems, caster wheels, sliding systems, ball transfer units, automotive components, and general mechanical assemblies.SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., is a precision steel ball manufacturer and integrated supply partner based in Tai’an City, Shandong Province, China. Since 1996, the company has developed long-term manufacturing experience in carbon steel balls, chrome steel balls, and stainless steel balls for industrial applications worldwide.From a technological capability perspective, SDBALLS understands the relationship between ball grade, material hardness, surface finish, dimensional consistency, and downstream machining. This knowledge helps support projects involving drilled, tapped, polished, plated, or otherwise customized spherical components. The company’s product grades range from high-precision options such as G10 to general industrial grades such as G1000, allowing buyers to match accuracy with real application needs.From a manufacturing capability perspective, SDBALLS operates three production facilities with annual capacity above 5,000 tons. This scale supports stable delivery for standard steel balls and provides a strong base for customized threaded ball and drilled sphere requirements. The company serves customers in more than 50 countries and supplies industries including bearing production, automotive components, hardware, grinding, caster wheels, sliding systems, ball transfer units, and outdoor equipment.From a service capability perspective, SDBALLS helps global buyers consolidate procurement. In addition to its own steel ball manufacturing, the company can support sourcing for plastic, glass, ceramic, copper, aluminum, and other spherical products. This integrated model is valuable for distributors, OEMs, and fixture builders that want fewer suppliers, clearer communication, and more stable supply chain coordination.The company maintains quality systems supported by IATF 16949, ISO 9001, and ISO 14001 certifications. For buyers in the Global Market, this means SDBALLS can support discussions about quality documentation, environmental management, inspection procedures, and long-term cooperation. Its customer-focused sales structure, including global sales and US business support, helps international buyers communicate efficiently from sample development to repeat production.Looking ahead to 2026, threaded ball sourcing will be influenced by digital inspection, automated drilling and tapping, AI-supported quality analysis, stricter sustainability requirements, lower-carbon logistics, recyclable packaging, and greater traceability expectations. Buyers will increasingly prefer suppliers that can provide stable documentation, responsible production, and flexible customization rather than simple commodity supply. Trade policy changes, regional inventory strategies, and port congestion risks will also encourage buyers to work with experienced suppliers that understand global shipping routes through Qingdao, Shanghai, Singapore, Rotterdam, Hamburg, Los Angeles, and Jebel Ali.A threaded ball is a spherical component with an internal or external thread. It may have a blind tapped hole, through threaded hole, inserted stud, or custom drilled feature. It is used in fixtures, handles, positioning systems, mounting assemblies, and automation equipment.Metric sizes from M3 to M20 are common in industrial applications. M6, M8, M10, and M12 are especially popular for fixture and mounting systems. Inch threads such as UNC and UNF can also be produced for North American equipment or special OEM requirements.Carbon steel is cost-effective for dry indoor fixtures. Chrome steel is useful where hardness and wear resistance matter. 304 stainless steel is suitable for general corrosion resistance, while 316 stainless steel is better for marine, chemical, outdoor, and high-humidity applications.Yes. Custom options include special thread pitch, blind holes, through holes, cross drilling, threaded studs, special chamfers, polishing, plating, passivation, black oxide, laser marking, and controlled inspection requirements. Buyers should provide drawings for accurate quotation.Inspection should include ball diameter, thread gauge fit, thread depth, surface finish, burr control, material verification, hardness where required, and visual appearance. For precision applications, concentricity, perpendicularity, and roundness may also be measured.Standard threaded balls use common materials, sizes, and thread forms, so they usually have shorter lead times and lower MOQ. Custom threaded balls are made to specific drawings and may include special materials, tolerances, coatings, or inspection reports.Standard orders may take one to four weeks depending on stock and quantity. Custom OEM orders often require four to eight weeks or more because of sample approval, special machining, surface treatment, inspection, and packaging requirements.An RFQ should include ball diameter, material, thread size, pitch, thread depth, blind or through hole type, tolerance, surface finish, coating, quantity, annual demand, inspection requirements, packaging needs, destination country, and preferred delivery method.Yes. They are widely used in automation as adjustable contact points, locating elements, pivot components, end stops, sensor mounts, handles, and fixture parts. Precision requirements depend on whether the ball is used for simple support or accurate positioning.SDBALLS combines decades of steel ball manufacturing experience, large production capacity, global export service, quality certifications, and integrated sourcing capability. This makes it suitable for buyers seeking standard balls, custom drilled balls, threaded ball components, and multi-material sphere procurement. -
Copper Ball Supplier Guide for Global Market OEM Buyers
For industrial OEM buyers in the global market, the best copper ball supplier is not simply the company with the lowest unit price. The right partner must match material grade, conductivity requirement, size tolerance, surface finish, batch traceability, packaging, export capability, and long-term supply stability. Copper balls are used in electrical contacts, switchgear components, conductive assemblies, grounding systems, thermal transfer devices, valves, instrumentation parts, decorative hardware, and some chemical or plating applications. Because these uses differ sharply, a single “standard copper ball” specification is rarely enough for serious procurement.If your application requires high electrical conductivity, C11000 electrolytic tough pitch copper is often the first grade to evaluate. If machinability, cost control, or corrosion behavior in a less conductivity-critical application is more important, brass alloy balls may be considered. If the product operates in high-current assemblies, EV systems, battery packs, distribution cabinets, or telecom grounding systems, the supplier should provide conductivity testing, chemical composition reports, and dimensional inspection records. For valve seats, flow control, and mechanical contact parts, sphericity, hardness, surface roughness, and corrosion resistance may be more important than the highest IACS conductivity value.A practical short list for OEM sourcing should include three categories of suppliers: direct copper ball manufacturers, precision ball manufacturers with multi-material sourcing capability, and integrated industrial supply partners. Direct manufacturers can be attractive for repeated high-volume orders. Precision ball specialists understand grading, tolerance, lapping, inspection, and packaging disciplines. Integrated supply partners are valuable when global buyers need copper, steel, stainless steel, ceramic, plastic, glass, or aluminum balls under one procurement program. This is especially relevant for buyers in Chicago, Stuttgart, São Paulo, Singapore, Dubai, Rotterdam, Mumbai, and Shenzhen who coordinate multiple plants across regions.When time is limited, use this decision rule: choose C11000 copper balls for conductivity-driven OEM parts; choose brass balls for moderate conductivity with better cost balance or mechanical convenience; choose a supplier that can document material origin, test results, and dimensional capability; and avoid any quotation that does not define grade, diameter tolerance, surface finish, inspection method, packaging, lead time, and Incoterms. A low price without these details can create expensive line stoppages, failed incoming inspection, and customer warranty claims.Buying QuestionPreferred ChoiceAlternative ChoiceVS Decision PointRisk if IgnoredOEM RecommendationNeed maximum conductivity?C11000 pure copper ballBrass alloy ballCopper VS brassHigher resistance and heat buildupSpecify conductivity and test reportNeed lowest stable cost?Brass alloy ballC11000 copper ballCost VS performanceOverpaying for unused conductivityMatch material to actual loadNeed tight diameter control?Precision ball manufacturerGeneral metal parts traderPrecision VS commodityPoor fit or leakageRequest tolerance capability dataNeed global delivery?Export-experienced supplierLocal small workshopGlobal logistics VS local availabilityCustoms delay and missed launchConfirm HS code, packing, and documentsNeed long-term traceability?Certified manufacturer or supply partnerSpot market resellerTraceability VS one-time purchaseUncontrolled material variationAudit batch control before approvalNeed multiple sphere materials?Integrated sourcing partnerSingle-material supplierConsolidation VS specializationFragmented purchasing workloadUse one qualified partner for familiesThe table shows why copper ball sourcing is a technical purchasing decision rather than a simple catalog purchase. A correct supplier comparison should connect application, grade, tolerance, inspection, and logistics. In the global market, ports such as Shanghai, Qingdao, Ningbo, Rotterdam, Los Angeles, Hamburg, Jebel Ali, Busan, and Singapore influence freight time and landed cost. Buyers should ask whether the supplier can support both sea freight for bulk orders and air freight for urgent pilot runs.Copper ball material selection begins with the distinction between commercially pure copper and copper alloy. C11000, often called electrolytic tough pitch copper, is widely recognized for high electrical and thermal conductivity. It is commonly used where current transfer, heat dissipation, and stable conductive performance are critical. Brass, typically a copper-zinc alloy, offers different advantages: improved machinability, attractive color, moderate corrosion resistance, and often better cost control depending on metal prices. However, brass is not a direct substitute for pure copper when a drawing or standard requires high conductivity.For OEM engineers, the question is not “which material is better?” but “which material is correct for the duty cycle?” A copper ball used as a current-carrying contact in a battery connector has different requirements from a brass ball used in a valve, decorative knob, or low-load positioning mechanism. In high-current electrical assemblies, contact resistance can cause temperature rise. Even small variations in material composition, oxidation level, and surface cleanliness can affect performance. In valves or mechanical assemblies, wear behavior, sealing surface, and dimensional repeatability may dominate.C11000 copper balls usually require careful handling because pure copper is softer than many steels and some brass compositions. During production, polishing, storage, and packaging must prevent dents, contamination, and surface oxidation. Brass alloy balls may tolerate handling slightly better in some cases, but alloy composition must still be controlled. Lead-containing brass may be restricted for some markets and applications. With tightening environmental rules in the European Union, California, and many electronics supply chains, buyers should confirm RoHS, REACH, and customer-specific substance requirements.Material FactorC11000 Pure Copper BallBrass Alloy BallC11000 VS BrassBest Application FitProcurement NoteElectrical conductivityVery highModerate to low depending on alloyPure copper winsElectrical contacts, grounding, busbar partsAsk for IACS value or conductivity testThermal conductivityHighLower than pure copperPure copper winsHeat transfer and thermal managementConfirm operating temperature and surface finishMachinabilityLowerOften betterBrass winsValve parts and mechanical assembliesCheck lead-free requirementMaterial costUsually higherOften lowerBrass may winCost-sensitive noncritical conductive partsCompare total landed cost, not only unit priceSoftness and dent riskHigher dent sensitivityGenerally more robustBrass may winBulk handling or nonprecision partsSpecify packaging density and separatorsCompliance riskUsually simpler if pure gradeDepends on alloying elementsC11000 may be simplerElectronics and regulated export marketsRequest RoHS and REACH declarationsAppearanceReddish copper toneYellow-gold toneApplication dependentDecorative and visible hardwareDefine acceptable oxidation and color rangeThis comparison is important because many RFQs use the phrase “copper ball” casually while the drawing may allow brass, bronze, or another copper alloy. Suppliers should not guess. A professional response will ask for the drawing, grade, applicable standard, diameter, tolerance, hardness, conductivity, surface finish, quantity forecast, and end-use environment. If the buyer cannot disclose the final product, at least the operating condition should be shared: dry or wet environment, current load, repeated contact cycles, chemical exposure, and assembly method.Global buyers also need to watch regional terminology. In North America, UNS designations such as C11000 are common. In Europe, EN material numbers or CW designations may appear. In China, GB/T copper grades may be referenced. Japanese, Korean, and Indian specifications may also appear in multinational programs. A competent supplier should help cross-reference standards but should not replace engineering approval. For safety-critical or electrical-certified assemblies, the final material approval should remain with the OEM engineering team.Electrical OEMs have stricter supplier expectations than general hardware buyers. Their components may enter switchgear, energy storage systems, industrial sensors, power tools, charging infrastructure, telecom cabinets, smart meters, medical devices, railway equipment, or automation platforms. Failures can cause heat, signal instability, corrosion, arcing, warranty returns, or certification problems. Therefore, supplier evaluation should focus on five critical factors: material control, precision capability, testing discipline, production stability, and commercial responsiveness.The first factor is material control. A supplier should know whether the balls are made from certified copper wire, rod, slug, or other input forms. Material certificates should be linked to production batches. The second factor is dimensional capability. Diameter tolerance, roundness, surface defects, and sorting method all influence assembly performance. The third factor is testing discipline. Conductivity, hardness, chemical composition, visual inspection, and sample retention may be needed depending on application. The fourth factor is production stability. OEMs need repeatability across months and years, not just a good first sample. The fifth factor is communication and service. Fast quoting, drawing review, export documentation, and corrective action response can determine whether a supplier is suitable for a global supply chain.For buyers in major industrial regions such as the U.S. Midwest, Germany’s Baden-Württemberg and Bavaria, Northern Italy, Mexico’s Bajío region, Guangdong, Jiangsu, Tamil Nadu, Ontario, and the ASEAN electronics corridor, dual sourcing is common. A supplier that can provide stable samples, production PPAP-like documents when required, and clear shipment schedules will be preferred over a low-cost factory that cannot communicate risk. Electrical OEM purchasing teams should also involve quality engineers early. Copper balls may look simple, but their failure modes often appear only after assembly, cycling, or environmental exposure.Supplier FactorStrong Supplier BehaviorWeak Supplier BehaviorStrong VS WeakAudit EvidenceBuyer ActionMaterial controlProvides grade certificates and batch linksOnly states “red copper” or “brass”Traceable VS vagueIncoming material recordsReject unclear material descriptionsDimensional precisionDefines tolerance and measurement toolsQuotes size without toleranceControlled VS approximateInspection reports and gauge calibrationInclude tolerance in POConductivity testingCan test or outsource verified testingAssumes conductivity from gradeVerified VS assumedTest reports and equipment recordsSet test frequency by riskSurface protectionUses clean packing and anti-oxidation controlShips loose in unsuitable bagsProtected VS damagedPacking photos and trial shipmentApprove packaging before bulk orderExport serviceHandles invoices, packing list, origin dataDelays documents after shipmentPrepared VS reactivePast export recordsConfirm documents before dispatchCorrective actionUses root cause and containmentOffers discount onlySystem improvement VS price excuse8D or corrective action examplesEvaluate response during sample stageThe explanation behind this table is simple: copper ball supplier selection should reduce technical and supply-chain uncertainty. A strong supplier behaves like a manufacturing partner, not just a seller. For electrical OEMs, it is reasonable to request samples from multiple lots, inspect incoming parts under real assembly conditions, and run thermal or contact-resistance testing before releasing a mass-production order.Future trends in 2026 will make these five factors even more important. Electrification, AI data centers, renewable energy, and high-density power electronics are increasing demand for reliable conductive components. At the same time, regulations on restricted substances, carbon reporting, and responsible sourcing are expanding. OEMs may ask suppliers to provide not only material certificates but also energy-use data, packaging reduction plans, recycled content information, and evidence of ethical metal sourcing. Suppliers that prepare for digital traceability and sustainability reporting will have an advantage in global programs.Conductivity testing verifies whether a copper ball can meet electrical performance expectations. For C11000 copper, conductivity is commonly discussed as a percentage of IACS, the International Annealed Copper Standard. Exact requirements depend on the end-use and the applicable engineering standard. In some cases, chemical composition certification is enough. In higher-risk programs, buyers may require direct conductivity measurement, contact resistance testing after assembly, salt spray testing, thermal cycling, or accelerated aging. The right level of testing should match the cost of failure.Quality control for copper balls also includes dimensional inspection. Diameter can be measured by micrometer, comparator, air gauge, optical system, or specialized ball gauges depending on precision level. Roundness and surface defects require additional control. Since copper is softer than steel, visual inspection is important for dents, flats, scratches, embedded particles, staining, and oxidation. Surface contamination can affect electrical contact and plating behavior. If copper balls will be plated with silver, tin, nickel, or another finish, the base ball surface condition becomes even more critical.Quality documentation may include material certificate, chemical analysis, conductivity report, hardness test, dimensional inspection report, surface inspection record, packaging approval, and certificate of conformity. For automotive or high-reliability electrical applications, customers may ask for control plans, process flow charts, PFMEA, sample submission documents, and lot traceability. Not every copper ball application needs automotive-level documentation, but the supplier should be able to scale quality support according to buyer risk.SDBALLS Industry Corp has built its reputation in precision steel balls, with quality systems including IATF 16949, ISO 9001, and ISO 14001. While copper balls may be supplied through integrated sourcing depending on specification, the same disciplined mindset is relevant: clear grade definition, inspection planning, controlled packaging, and long-term supplier cooperation. Buyers can review the company’s quality philosophy through its quality and technical capability information when evaluating whether a procurement partner understands precision ball requirements beyond simple trading.Quality ItemTypical MethodHigh-Risk RequirementBasic VS Advanced ControlWhy It MattersBuyer TipChemical compositionMaterial certificate or lab analysisLot-specific verificationCertificate VS verified chemistryConfirms C11000 or brass alloyRequire grade on quotation and invoiceConductivityIACS measurement or approved testBatch conductivity reportAssumed VS measuredPrevents overheating and resistance issuesDefine minimum acceptable conductivityDiameterMicrometer or gauge inspectionStatistical inspection and capability dataSpot check VS process controlEnsures fit and functionState tolerance and sampling planRoundnessRoundness tester or precision comparatorControlled by grade and applicationGeneral VS precision gradeAffects sealing, rolling, and contactRequest roundness if assembly is sensitiveSurface finishVisual inspection or roughness testDefined roughness and defect limitsVisual VS measurableInfluences contact and platingUse approved samples as referenceHardnessMicrohardness or suitable scaleLot control after forming or treatmentOptional VS controlledIndicates deformation resistanceSpecify only when function requires itPackaging integrityPacking inspectionDrop test or transport simulationStandard VS validatedPrevents dents and oxidationApprove labels, bags, and cartonsThe table highlights a common sourcing mistake: buyers often over-focus on diameter and under-specify conductivity or surface cleanliness. For conductive applications, a ball with correct size but poor surface condition may still fail. Conversely, for mechanical valve use, conductivity may be irrelevant while roundness and corrosion behavior are essential. A helpful supplier will challenge incomplete specifications and help the buyer select appropriate inspection items.Custom size capability is one of the main reasons OEMs search beyond standard catalog suppliers. Copper balls may be needed in small diameters for electrical contacts or sensors, medium diameters for valves and assemblies, or larger diameters for thermal mass, decorative hardware, or specialized industrial systems. Diameter is only one part of customization. Buyers may also request tolerance class, surface polish, hardness range, cleaning, plating preparation, special packaging, mixed-size kits, or private labeling.In precision ball manufacturing, tighter tolerances usually require more process control, sorting, and inspection. This increases cost and lead time. For a low-speed noncritical application, an overly tight tolerance may waste money. For a sealing valve, electrical contact nest, or automated assembly feeder, loose tolerance may create jams, leakage, or inconsistent performance. Buyers should discuss the functional tolerance, not just copy a generic tight number. If the application has a mating seat, spring, contact cup, or guide track, sharing the related drawing can help the supplier recommend a realistic specification.Custom orders also require clear agreement on sample approval. A good approach is to request an engineering sample batch, inspect it internally, perform assembly trials, and then freeze the specification before mass production. If color, surface brightness, or oxidation appearance matters, the buyer should approve visual standards under defined lighting. Copper naturally oxidizes, so packaging and storage conditions should be controlled. Vacuum packaging, anti-tarnish paper, sealed bags, desiccants, or oil-free protective packing may be considered depending on downstream use.Leading manufacturers and sourcing partners also support export labeling. For global programs, labels may need customer part number, supplier lot number, material grade, diameter, quantity, net weight, gross weight, country of origin, and date code. Plants in Monterrey, Detroit, Prague, Pune, Penang, and Ho Chi Minh City may use the same part number but require different label formats. Early alignment prevents receiving delays at warehouses and bonded logistics zones.Customization AreaStandard OptionCustom OptionStandard VS CustomCost ImpactBest PracticeDiameterCatalog sizesDrawing-specific sizeFast VS engineeredCustom tooling or sorting may add costConfirm annual forecast before toolingToleranceGeneral commercial toleranceTight precision toleranceEconomy VS performanceTighter tolerance raises inspection costSpecify only what function needsSurface finishGeneral polished surfaceDefined roughness or visual gradeBasic VS controlled appearanceAdditional finishing may be neededUse approved limit samplesMaterial gradeCommon copper or brassC11000 or specified alloyAvailable VS certifiedCertified material may cost moreState UNS or equivalent standardPackagingBulk bags or cartonsSmall packs, trays, anti-tarnish packingBulk VS protectedPackaging can significantly affect landed costBalance protection with logistics efficiencyDocumentationInvoice and packing listFull inspection and traceability packageCommercial VS quality-controlledDocumentation adds time and laborDefine documents before quotationPlating preparationNo special cleaningCleaned surface for downstream platingGeneral VS process-readyCleaning and handling add costCoordinate with plating supplierThis table shows that customization should be treated as value engineering. The cheapest ball may not be the lowest-cost solution if it causes assembly rejects. At the same time, the most precise ball may not be economically justified for a simple weight, decorative insert, or low-stress valve component. Good supplier communication helps find the middle point.A factory audit for copper ball production should be practical, not ceremonial. Buyers should verify whether the supplier can consistently produce or source the required material, maintain clean handling, inspect key characteristics, protect the product during transport, and trace each shipment to a defined batch. The audit may be on site, remote by video, or document-based depending on order size and risk. For strategic programs, an on-site visit is ideal. For smaller global orders, a structured remote audit may be enough.The audit should begin with company legitimacy and production scope. Does the supplier actually manufacture copper balls, outsource them, or act as an integrated procurement partner? All three models can be acceptable if transparent. Problems begin when a trader presents itself as a factory but cannot control material or inspection. The audit should then review incoming material control, production flow, forming or machining process, polishing or finishing, sorting, inspection, nonconforming product control, packaging, warehouse conditions, and shipment documents.Material traceability is especially important for electrical OEMs and regulated industries. Each lot should have a record of material source, production date, inspection data, quantity, and shipment destination. If a quality issue occurs in Hamburg, Houston, Dubai, or Melbourne, the supplier must identify affected batches quickly. Without traceability, a small defect can turn into a global recall or broad containment action. Buyers should also ask how long records are retained and whether sample retention is available.SDBALLS’ manufacturing experience is rooted in more than three decades of precision ball production in Shandong, with multiple production facilities and high annual capacity for its core steel ball portfolio. This manufacturing background matters because ball products require repeatable forming, grading, polishing, inspection, and packing routines. Buyers looking for copper balls, copper alloy balls, or multi-material sphere packages can also explore the company’s broader industrial ball product range to understand how procurement programs may be consolidated.Audit AreaWhat to CheckAcceptable EvidenceFactory VS Trader IssueRed FlagRecommended ActionBusiness scopeManufacturing or sourcing modelLicense, website, references, facility photosTransparent VS hidden outsourcingRefuses to explain production sourceRequire written supply modelMaterial receivingGrade verification and supplier approvalCertificates, incoming inspection recordsControlled VS uncontrolled inputNo grade recordMake material certificate mandatoryProcess controlForming, polishing, cleaning, sortingProcess flow and work instructionsStable process VS ad hoc productionNo documented processAudit process before bulk orderInspection systemTools, calibration, samplingCalibration certificates and reportsMeasured VS guessedUncalibrated toolsRequest third-party inspection if neededTraceabilityLot number and record retentionBatch card, label, shipment recordTraceable VS mixed lotsMixed material binsUse lot-based packagingWarehouse controlCleanliness, humidity, separationStorage photos and proceduresProtected VS exposedOxidized or dented stockDefine storage and packing rulesExport readinessDocumentation and logistics experiencePast bill of lading, commercial documentsExport-capable VS domestic-onlyIncorrect customs dataConfirm Incoterms and HS code earlyThe audit table provides a simple roadmap. Buyers do not need to demand unnecessary paperwork from every small order, but they should never ignore traceability for electrical, automotive, energy, or safety-related components. A supplier that welcomes reasonable audit questions usually has better internal discipline than one that treats questions as a nuisance.Minimum order quantity and pricing are influenced by material grade, diameter, tolerance, finishing, inspection, packaging, and market metal prices. Copper is a globally traded commodity, so quotations may change with copper price movement on major exchanges and regional premiums. Brass alloy pricing also depends on copper and zinc markets. Buyers should understand whether a quotation is valid for a fixed period, tied to a metal index, or based on spot inventory.MOQ negotiation is easiest when the buyer can share realistic annual volume, release schedule, and forecast confidence. Suppliers may accept a lower trial MOQ if there is credible future demand. For custom sizes, tooling, special sorting, or strict documentation, suppliers need enough volume to justify setup. A common strategy is to place a pilot order at a slightly higher unit price, then negotiate tiered pricing after approval. Another method is blanket order with scheduled releases, allowing the supplier to plan material and production while the buyer avoids excessive inventory.Bulk pricing should be compared on total landed cost rather than unit price alone. Freight, customs duty, insurance, packaging, inspection fees, bank charges, local trucking, and inventory carrying cost can change the real cost dramatically. A buyer in Los Angeles may prefer ocean freight through Long Beach for high-volume shipments. A buyer in Central Europe may compare Hamburg, Rotterdam, Koper, and rail routes from China. A buyer in the Middle East may use Jebel Ali as a redistribution hub. A buyer in South America may compare Santos, Callao, and Cartagena depending on final plant location.Packaging affects MOQ and freight cost. Copper balls are dense, and excessive small packaging raises labor and carton volume. However, insufficient packaging can cause dents and oxidation. For precision or visible-surface balls, the cost of protective packing is often justified. For robust nonappearance applications, bulk packing may be acceptable. The buyer should request both options during quotation and test packaging through a sample shipment.Negotiation should also cover payment terms, lead time, inspection responsibility, quality claim window, replacement policy, and currency. Some suppliers quote EXW, while global OEMs may prefer FOB Qingdao, FOB Shanghai, CIF Rotterdam, DAP warehouse, or other Incoterms. The cheapest EXW price may become expensive if the buyer lacks reliable freight consolidation. Integrated suppliers can sometimes combine copper balls with other industrial balls, reducing administrative and logistics burden.Copper balls and brass balls appear in many industries, but each application has a different performance logic. In electrical contacts, the key concerns are conductivity, contact resistance, surface cleanliness, oxidation, and mechanical stability under repeated engagement. In valves, the concerns may be roundness, corrosion, sealing, hardness, and compatibility with fluid. In thermal management, the focus may be thermal conductivity, surface area, heat transfer efficiency, and compatibility with the surrounding structure. Using one generic specification across these applications is a common mistake.Electrical contact applications may include switches, relays, connectors, battery modules, grounding devices, test fixtures, and conductive transfer systems. C11000 copper is often considered because of its strong conductivity. However, pure copper can oxidize, so some designs use plating or controlled contact pressure. Brass may be used in less demanding electrical functions or where mechanical characteristics and cost matter more than conductivity. The supplier should understand whether the ball is a primary current path or a secondary positioning/contact element.Valve applications may use brass or copper alloy balls depending on fluid, pressure, and sealing design. Brass is common in plumbing and fluid control components, but alloy compliance is important for potable water and environmental regulations. Lead-free brass may be required in many markets. For chemical equipment, compatibility must be reviewed carefully. A copper ball may not be suitable for every fluid environment. Buyers should confirm standards for water, gas, oil, refrigerant, or specialty chemicals.Thermal management uses may include heat transfer media, thermal interface assemblies, heat exchangers, experimental cooling systems, and electronics-related heat spreading. Copper’s thermal conductivity is valuable, but surface condition and oxidation still matter. In 2026 and beyond, demand for thermal materials will continue to grow because EV charging, power electronics, data centers, and high-performance industrial automation generate increasing heat density. Copper ball suppliers that can support clean, consistent, and well-documented products will be better positioned for these emerging applications.For industry selection examples, buyers can review how precision balls support different mechanical and industrial systems through SDBALLS’ application overview for industrial balls. Although every copper ball program should be validated by the buyer’s engineering team, application-based thinking helps avoid over-specification and under-specification.Case study one: an electrical equipment OEM in Germany needed conductive balls for a spring-loaded contact assembly. The original supplier provided low-cost copper-colored alloy balls without conductivity documentation. During thermal testing, several assemblies exceeded the allowed temperature rise. The buyer revised the specification to C11000, added conductivity reporting, and required sealed anti-oxidation packaging. The unit price increased, but assembly rejects dropped and certification testing stabilized.Case study two: a valve component buyer in Mexico used pure copper balls because the internal purchasing description said “copper.” The engineering team later found that brass alloy balls provided better machinability and sufficient corrosion behavior for the actual medium. After changing to a controlled brass specification, the buyer reduced cost and improved handling durability. This case shows why copper VS brass comparison should be application-based.Case study three: a thermal equipment developer in Singapore needed small batches of copper balls for prototype heat transfer experiments. MOQ was a problem with direct factories. An integrated supply partner helped source pilot quantities, then supported larger production once the design was approved. The value was not only product supply, but also flexible procurement during development.SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., is a precision ball manufacturer and integrated supply partner headquartered in Tai’an City, Shandong Province, China. Since 1996, the company has developed strong manufacturing experience in carbon steel balls, chrome steel balls, stainless steel balls, and related spherical products. Its core production grades range from high-precision bearing applications to general industrial and grinding uses. For global buyers, this background provides a practical foundation for understanding tolerance, surface quality, inspection, packaging, and export expectations.From a technological capability perspective, SDBALLS works with precision ball standards, grading requirements, dimensional inspection, and quality system thinking. Copper balls are different from steel balls in material behavior, but the discipline of ball procurement remains similar: clear grade, controlled dimension, reliable surface, correct packaging, and documented batch information. When customers need copper, brass, aluminum, glass, ceramic, or plastic balls alongside steel balls, SDBALLS can act as an integrated sourcing partner, helping reduce the number of suppliers that purchasing teams must manage.From a manufacturing capability perspective, SDBALLS operates multiple production facilities and has built stable capacity in its core steel ball categories. This manufacturing culture supports practical communication with factories and subcontracted material partners when multi-material spheres are required. Buyers benefit because the team understands production constraints, inspection realities, and packaging risks. Instead of treating copper balls as simple merchandise, the company can support specification review, sample coordination, and supply chain planning.From a service capability perspective, SDBALLS serves customers in more than 50 countries and supports international purchasing teams with export communication, documentation, and consolidated procurement options. For buyers in North America, Europe, the Middle East, Southeast Asia, and Latin America, the company can help evaluate whether direct production, integrated sourcing, or combined shipment is the best approach. Its global sales support and customer-focused model are particularly useful when OEMs need repeated communication across engineering, purchasing, quality, and logistics departments.Buyers who want to understand the company’s background can visit the SDBALLS company profile. For procurement teams, the best next step is to send a drawing or specification, expected annual volume, target application, required documents, and destination port or delivery address. With this information, the supplier can advise whether C11000 copper balls, brass alloy balls, or another sphere material is the most suitable option.In the global market, SDBALLS is not positioned merely as a catalog seller. Its value is strongest when customers require stable communication, multi-material sourcing, technical discussion, and long-term cooperation. This is important for OEMs that manage complex bills of materials and need one partner to coordinate precision balls for bearings, automotive parts, caster wheels, sliding systems, ball transfer units, outdoor applications, and special conductive or nonconductive sphere requirements.If the ball is part of a primary electrical or thermal path, start with C11000 copper and verify conductivity. If the ball is mainly mechanical, decorative, or used in a moderate-conductivity role, brass may be suitable. Always confirm the application environment and compliance requirements before approval.Not always. Low-risk or non-electrical applications may only need material certification. Electrical OEMs, high-current systems, and safety-related assemblies should consider batch conductivity testing or at least periodic verification. The test frequency should reflect risk, volume, and customer requirements.Copper naturally oxidizes when exposed to air, humidity, and handling contamination. Color variation does not always mean functional failure, but it can matter for electrical contact, plating, or visible parts. Buyers should define acceptable appearance, storage condition, and packaging method.Sometimes, but not automatically. Brass has lower conductivity than pure copper. It may work in low-current or mechanical-contact roles, but it should not replace C11000 copper where high conductivity is specified unless engineering approves the change after testing.A strong RFQ should include material grade, diameter, tolerance, quantity, annual forecast, application, required test reports, surface requirement, packaging, destination, Incoterms, and target lead time. If possible, attach a drawing and approved standard.MOQ depends on size, material, stock availability, tolerance, and documentation. Standard or available sizes may allow lower MOQ. Custom grades, tight tolerances, and special packaging normally require higher MOQ. Trial orders can often be negotiated before mass production.China, Europe, India, Japan, Korea, North America, and Southeast Asia all have relevant industrial supply bases. For export logistics, ports and hubs such as Qingdao, Shanghai, Ningbo, Singapore, Busan, Rotterdam, Hamburg, Los Angeles, Jebel Ali, and Santos can affect delivery time and landed cost.Buyers should ask suppliers about recyclable packaging, restricted substance compliance, responsible metal sourcing, energy management, and carbon reporting readiness. Sustainability is becoming part of supplier approval, especially for electronics, automotive, energy, and European market programs.SDBALLS is primarily a precision steel ball manufacturer and also acts as an integrated supply partner for multi-material spheres, including copper and brass balls depending on specification. Buyers should submit drawings and requirements so the team can confirm the best supply route.Buyers can begin by reviewing SDBALLS’ product and quality information, then sending a detailed RFQ. The most efficient inquiry includes application, grade, tolerance, quantity, destination, and required documents. This allows the supplier to respond with a technically meaningful quotation.Choosing copper ball suppliers for the global market requires a balance of engineering judgment and purchasing discipline. The most reliable result comes from defining the material correctly, comparing C11000 pure copper with brass alloy based on function, verifying conductivity and quality controls, approving realistic tolerances, auditing traceability, negotiating MOQ with forecast data, and matching the product to the actual application. With global electrification, sustainability expectations, and supply chain complexity increasing through 2026, OEMs should favor suppliers and integrated partners that communicate clearly, document consistently, and support long-term cooperation. -
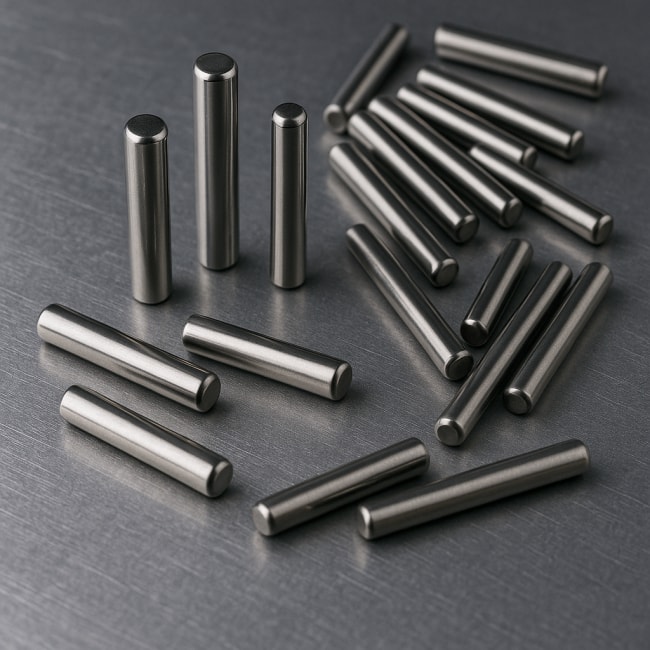
Needle Roller Sourcing Guide for the Global Market 2026
For procurement teams sourcing needle rollers in the Global Market, the best supplier is not simply the lowest-price factory. A reliable needle roller supplier should demonstrate stable dimensional control, traceable materials, certified quality systems, repeatable heat treatment, controlled surface finish, packaging discipline, and responsive export service. Automotive, gearbox, power tool, industrial automation, agricultural machinery, and precision bearing OEMs should evaluate suppliers through a combined review of technical specifications, production capability, quality certification, audit results, MOQ flexibility, inventory support, and long-term engineering communication.Needle rollers are compact cylindrical rolling elements used where high load capacity must fit into limited radial space. Compared with balls, needle rollers provide a larger line-contact area and can support higher radial loads in compact assemblies. They are commonly used in drawn cup needle roller bearings, cage assemblies, thrust needle rollers, planetary gearboxes, automotive transmissions, compressors, pumps, starter motors, steering systems, and small mechanical modules. Because a single defective roller can affect noise, torque, wear, fatigue life, and gearbox efficiency, procurement should treat needle rollers as precision functional components rather than commodity metal parts.In 2026, global sourcing is shaped by tighter quality expectations, carbon reporting, trade uncertainty, reshoring strategies, and dual-source supply chain design. Buyers in Detroit, Stuttgart, Milan, Birmingham, Pune, Monterrey, São Paulo, Istanbul, Osaka, Busan, Shanghai, Shenzhen, Singapore, Dubai, Rotterdam, and Los Angeles increasingly request more than a quotation. They expect APQP thinking, PPAP documents for automotive projects, batch-level traceability, salt spray or corrosion data when relevant, packaging validation for sea freight, and clear escalation procedures. A supplier that understands port logistics through Qingdao, Shanghai, Ningbo, Hamburg, Rotterdam, Long Beach, Jebel Ali, and Singapore can reduce avoidable delays in international programs.For buyers who also procure precision steel balls, bearing balls, or multi-material spherical components, working with an integrated supplier can simplify vendor management. SDBALLS Industry Corp, headquartered in Tai'an City, Shandong Province, China, has built more than three decades of precision rolling element manufacturing experience since 1996. While its core production focus is precision steel balls, the company also supports global customers through consolidated sourcing and technical supply chain coordination for related rolling components. Buyers can review its manufacturing background through the company overview and assess its broader component portfolio through the product center.Buyer QuestionRecommended AnswerWhy It MattersBuyer Risk if IgnoredWhat is the first specification to confirm?Diameter, length, end shape, grade, hardness, surface roughness, and material.These define fit, load capacity, and bearing life.Noise, seizure, uneven wear, or failed assembly.Which certificate is essential?ISO 9001 is baseline; IATF 16949 is preferred for automotive supply.It proves process-based quality management.Unstable batches and poor corrective action.Is low price enough?No; compare total cost including scrap, inspection, freight, and downtime.Precision rollers influence system performance.Higher hidden cost than the purchase saving.What should be audited?Material control, heat treatment, grinding, inspection, packing, and traceability.Needle roller quality depends on process control.Unverified capability and inconsistent shipments.How should lead time be managed?Use forecast sharing, safety stock, and agreed reorder points.Bearings and gearboxes often have long production cycles.Line stoppage and emergency air freight.What is the 2026 trend?More digital inspection, carbon data, supplier dualization, and custom engineering.Global OEMs need resilient and transparent supply chains.Loss of preferred supplier status.This quick overview should be used as the starting point. The sections below provide detailed sourcing standards, supplier evaluation methods, certification expectations, MOQ planning, audit checklists, customization guidance, material comparisons, company capability notes, and practical FAQ support for buyers in the Global Market.Needle roller procurement begins with a precise technical drawing or a well-structured specification sheet. A vague request such as “standard needle rollers” is not enough for serious purchasing. Buyers should define nominal diameter, roller length, diameter tolerance, length tolerance, cylindricity, roundness, surface roughness, chamfer or crowned-end geometry, hardness range, metallurgical structure, residual magnetism, cleanliness, corrosion protection, and packaging method. For OEM programs, the drawing should also specify inspection method, sampling plan, and approval documents.The most common materials for needle rollers include chrome bearing steel such as GCr15, SAE 52100, or 100Cr6; stainless steels such as AISI 440C, 304, or 316 for corrosion resistance; and ceramics such as silicon nitride or zirconia for special environments. In conventional gearbox and bearing applications, chrome steel remains the main choice because it offers high hardness, excellent fatigue performance, and favorable cost. Stainless steel is used where moisture, chemicals, food processing, or outdoor exposure is important. Ceramic needle rollers are used selectively in high-speed, electrical insulation, low-density, or aggressive media applications, but they require careful design validation.Dimensional tolerance should be discussed with the supplier early. For high-performance automotive or transmission applications, buyers may require very tight diameter variation within a batch, controlled end radius, and precise surface finish. For general machinery, a wider tolerance may be acceptable. Over-specifying tolerance can increase cost unnecessarily, while under-specifying tolerance can create field failures. The best procurement approach is to match tolerance to the actual working condition, assembly clearance, shaft hardness, raceway condition, lubrication system, and expected duty cycle.Surface finish is particularly important because needle rollers operate with line contact. A rough surface increases friction and wear, while a poorly controlled grinding or polishing process may create defects that initiate fatigue. Hardness must also be consistent. Excessive hardness variation may lead to uneven load distribution. In many applications, heat treatment control, retained austenite control, and microstructure verification are as important as nominal hardness values.Specification ItemStandard RequirementHigh-Precision RequirementChrome Steel VS Stainless SteelDiameter toleranceSuitable for general bearing and machinery use.Controlled tightly for low-noise gearboxes and automotive assemblies.Chrome steel is often easier to control at high volume; stainless may need added process attention.Length toleranceDefined according to bearing cage or raceway design.Critical for thrust needle rollers and compact assemblies.Both can meet requirements, but stainless cost is usually higher.RoundnessMust support smooth rolling contact.Required for low vibration and long fatigue life.Chrome steel normally offers better economic fatigue performance.Surface roughnessFine ground or polished surface.Extra-fine finish for high-speed and low-noise systems.Stainless may need special finishing to balance corrosion and surface quality.HardnessUsually high hardness after heat treatment.Narrow hardness band with metallurgical verification.Chrome steel offers strong bearing hardness; stainless provides corrosion advantage.CleanlinessFree from burrs, rust, cracks, and contamination.Strict visual, magnetic, and automated inspection.Both require clean packing; stainless better resists storage corrosion.PackagingAnti-rust oil, sealed bags, cartons, or drums.Batch-separated, labeled, traceable, export-ready packaging.Chrome steel needs stronger rust prevention for long sea freight routes.For the Global Market, tolerance requirements may also vary by region and end customer. European gearbox buyers often emphasize technical drawings, measurement reports, and process capability. North American automotive buyers usually focus on PPAP, supplier corrective action, and continuity planning. Japanese and Korean customers may place strong emphasis on appearance, batch consistency, and detailed inspection discipline. Indian, Southeast Asian, Turkish, and Brazilian buyers often balance cost, availability, and application-specific performance. A capable supplier should communicate across these expectations without forcing every buyer into a single standard.Procurement teams should request sample inspection reports before placing bulk orders. A practical first order may include pilot samples, small-batch validation, endurance testing, and then controlled mass production. If the needle roller will be used in a safety-related gearbox, steering component, braking support mechanism, or high-speed motor assembly, the buyer should not skip validation. The cost of early testing is small compared with warranty claims, recall risk, or production shutdown.Automotive and gearbox OEMs require a deeper supplier evaluation process than general industrial buyers. A qualified needle roller supplier must prove that it can consistently produce parts to specification, maintain process stability, react quickly to quality issues, and support long-term program management. The evaluation should combine commercial review, engineering review, quality review, logistics review, and risk review.The first evaluation stage is technical capability. Buyers should ask whether the supplier understands bearing load, raceway interaction, lubrication sensitivity, noise requirements, and application-specific failure modes. A supplier that only quotes from size and material may not be suitable for OEM projects. Strong suppliers can discuss diameter grouping, heat treatment distortion, grinding burn prevention, end-profile control, surface defect detection, and anti-rust protection. They should also know how to handle engineering changes after production approval.The second stage is manufacturing capability. Buyers should review production equipment, process flow, capacity, bottlenecks, tool maintenance, and in-process inspection. Needle roller manufacturing generally includes wire or rod preparation, cutting, heat treatment, grinding, superfinishing, cleaning, inspection, oiling, and packaging. Each step can create defects if poorly controlled. For example, cutting may create burrs, heat treatment may create distortion or decarburization, grinding may create burns or dimensional variation, and poor washing may leave abrasive residue.The third stage is quality system maturity. A supplier may have excellent machines but weak documentation. Automotive and gearbox customers should look for control plans, PFMEA, inspection instructions, calibration records, nonconforming product procedures, traceability labels, corrective action records, and customer complaint history. The presence of ISO 9001 or IATF 16949 certification is important, but certification alone is not enough. The buyer should verify whether the system is actively used on the shop floor.The fourth stage is logistics resilience. Global buyers should ask about export experience, Incoterms, shipping lanes, customs documents, pallet standards, moisture protection, port selection, and emergency shipment options. For example, a buyer in Germany may prefer shipment through Qingdao or Shanghai to Hamburg or Rotterdam; a buyer in Mexico may use Long Beach, Houston, or Manzanillo; a buyer in the United Arab Emirates may rely on Jebel Ali; and a buyer in Southeast Asia may route through Singapore, Laem Chabang, or Port Klang. Understanding these trade hubs helps reduce delivery uncertainty.Evaluation AreaStrong Supplier SignalWeak Supplier WarningLocal Supplier VS Global SupplierEngineering supportCan review drawings and recommend practical tolerance ranges.Only provides price without technical questions.Local suppliers may respond faster; global suppliers may offer broader capacity.Quality controlUses documented inspection, calibrated gauges, and traceability.Relies mainly on final visual checks.Global suppliers should provide digital reports for remote buyers.CapacityShows stable production planning and backup equipment.Cannot explain monthly output or bottlenecks.Local suppliers may suit urgent orders; global suppliers may handle large programs.Cost structureExplains material, tolerance, packing, and logistics cost drivers.Offers unusually low price with no technical basis.Global sourcing may reduce unit cost but requires stronger inventory planning.CommunicationProvides fast, clear, technical responses.Gives inconsistent answers between sales and factory teams.Local suppliers may share time zones; global suppliers need disciplined project management.Risk managementMaintains contingency plans and alternative material channels.Has no plan for shortages or port delays.Dual sourcing often combines local security with global cost efficiency.ComplianceSupports certificates, material reports, and customer audits.Cannot provide updated documents.Global suppliers must satisfy multiple regulatory expectations.OEMs should also consider supplier behavior during the quotation phase. A professional supplier asks about application, annual volume, inspection level, target life, raceway material, lubrication, packaging, and delivery schedule. A weak supplier may push standard stock items without confirming whether they match the application. For long-term programs, the quality of early communication often predicts the quality of later cooperation.For buyers consolidating rolling element procurement, SDBALLS can support technical coordination across precision steel balls and related rolling component sourcing. Its long history in precision ball manufacturing gives it practical experience in material control, forming, heat treatment, grinding, surface finishing, and batch inspection. This manufacturing background is useful when procurement teams need one communication channel for multiple rolling element categories.Certification is a key filter in needle roller supplier selection. ISO 9001 is the global baseline for quality management systems, while IATF 16949 is the automotive quality management standard widely required by vehicle manufacturers and Tier 1 suppliers. For general industrial bearing supply, ISO 9001 may be sufficient if the supplier also provides strong inspection reports and stable process records. For automotive transmissions, electric vehicle gearboxes, steering systems, seat mechanisms, powertrain auxiliaries, and safety-sensitive assemblies, IATF 16949 or equivalent automotive quality discipline is strongly preferred.ISO 9001 focuses on process control, customer requirements, documentation, risk-based thinking, corrective action, and continual improvement. It helps ensure that the supplier has a structured system rather than relying only on individual operator experience. IATF 16949 builds on ISO 9001 and adds automotive-specific requirements such as defect prevention, variation reduction, traceability, contingency planning, embedded customer-specific requirements, and stronger production approval discipline.Buyers should request current certificates and verify scope, validity, issuing body, and factory address. A common mistake is accepting a certificate that covers a trading company office but not the manufacturing site. Another mistake is assuming that all products made by a certified company are automatically qualified. The buyer should confirm whether needle rollers or related bearing components fall within the audited scope and whether the production line follows the documented process.For automotive sourcing, buyers may request APQP, PPAP, control plan, PFMEA, MSA, SPC data, material test reports, dimensional layout reports, appearance inspection records, and packaging approval. Not every project needs the full package, but high-volume gearbox OEMs should not rely on informal sample approval. The documentation level should match risk and customer requirements.SDBALLS maintains internationally recognized quality management capabilities, including ISO 9001 and IATF 16949 systems for its precision manufacturing operations. Buyers can explore its quality philosophy and technical control approach through the quality and technical resources. The important point for procurement teams is to match supplier certification with actual project requirements rather than treating certificates as decorative documents.RequirementISO 9001 ExpectationIATF 16949 ExpectationIndustrial VS Automotive UseProcess documentationDefined procedures and records.Detailed automotive control plans and customer-specific requirements.Industrial projects may accept simpler documents; automotive projects need more depth.Risk managementRisk-based thinking across processes.Formal PFMEA and preventive action.Gearbox and vehicle programs require stronger failure prevention.Production approvalCustomer approval based on agreed evidence.PPAP submission may be required.Automotive approval is more structured and document-heavy.Measurement systemCalibrated equipment required.MSA and gauge R&R often expected.Precision rollers need verified measurement reliability.TraceabilityProduct identification and records.Enhanced batch traceability and recall support.Automotive supply needs faster containment capability.Continual improvementCorrective action and improvement process.Defect reduction, variation control, and customer scorecard focus.Automotive customers monitor long-term supplier performance closely.Contingency planningRecommended through risk controls.Explicit plans for disruptions and emergencies.Global supply chains need contingency for port delays, energy limits, and material shortages.Certification should also be connected to sustainability and compliance trends. In 2026, more OEMs are asking suppliers to provide environmental management evidence, carbon footprint data, responsible sourcing declarations, and recyclable packaging proposals. ISO 14001, although not always mandatory for needle rollers, can strengthen supplier credibility. Buyers serving European markets should also watch evolving requirements related to carbon reporting, chemical restrictions, and responsible supply chain disclosure.MOQ and lead time can determine whether a technically qualified supplier is commercially practical. Needle rollers may be ordered as standard catalog sizes, customized dimensions, or application-specific grouped batches. Standard sizes usually have lower MOQ and faster delivery. Customized rollers require tooling review, production scheduling, sample approval, and sometimes dedicated inspection fixtures. Buyers should clarify MOQ at three levels: sample MOQ, trial order MOQ, and mass production MOQ.Lead time depends on material availability, production capacity, heat treatment scheduling, inspection load, packaging requirements, and international freight. A typical standard item may ship faster if stock exists, while a custom automotive-grade roller may require several weeks for production and approval. Sea freight from China to Europe, North America, South America, or the Middle East adds additional time. Air freight can solve emergencies but is not suitable for routine cost control.Inventory management is especially important for bearing and gearbox supply chains because demand may fluctuate with vehicle production, agricultural seasons, construction activity, and industrial investment cycles. Buyers should combine forecast sharing, rolling purchase orders, safety stock, supplier-held inventory, and minimum stock agreements. For high-volume OEM projects, vendor managed inventory or regional warehouse support may reduce risk. For lower-volume spare parts, a scheduled replenishment plan may be more economical.Global buyers should consider regional buffer strategies. A European distributor may hold safety stock near Rotterdam, Antwerp, Hamburg, or Milan. A North American customer may position stock near Chicago, Dallas, Detroit, Monterrey, or Los Angeles. A Middle East buyer may use Dubai or Jebel Ali as a regional hub. Southeast Asian buyers may use Singapore, Bangkok, Ho Chi Minh City, or Port Klang. The best design depends on annual volume, demand volatility, shelf life, and freight cost.Supply Chain ItemRecommended PracticeLow-Cost ApproachResilient Approach VS Lowest InventorySample orderOrder enough pieces for inspection, assembly, and life testing.Minimum sample quantity only.Resilient validation reduces later risk; lowest sample cost may hide defects.Trial orderUse controlled batch production with full inspection report.Buy small mixed lots without process approval.Controlled trials support PPAP and process learning.Mass production MOQNegotiate by annual forecast and packaging efficiency.Push for very small lots every time.Stable MOQ improves price and production priority.Lead timePlan production plus inspection plus freight buffer.Assume factory time only.Realistic lead time prevents line stoppage.Safety stockSet by demand volatility and replacement time.Keep almost no stock to reduce cash use.Safety stock protects production against port and customs delays.Forecast sharingProvide rolling 3-month, 6-month, or 12-month forecasts.Order only when inventory runs out.Forecasts help suppliers reserve material and capacity.Packaging stockUse labeled, sealed, rust-protected, batch-separated packaging.Use generic bags or mixed cartons.Proper packaging protects quality during long storage and sea freight.In 2026, inventory planning is also affected by geopolitical uncertainty, port congestion, shipping rate volatility, and regional manufacturing incentives. Some OEMs are moving from single low-cost sourcing to “China plus regional backup” or “global dual source” models. This does not mean abandoning efficient Asian supply chains. It means designing a smarter network with qualified suppliers, transparent communication, and planned buffers. A supplier with export experience and flexible service can help buyers adjust without panic purchasing.SDBALLS supports global customers with export-oriented service capabilities, English communication, packaging coordination, and consolidated procurement assistance. Its sales and support teams work with buyers across more than 50 countries, helping customers coordinate specifications, documents, and delivery planning for rolling elements and related products.A supplier audit is one of the most effective ways to identify real manufacturing capability. If an on-site audit is not possible, buyers can request a remote audit with video review, document sharing, process photos, equipment lists, and live production discussion. The audit should not be limited to a showroom or certificate file. It should follow the actual production path from incoming material to final packing.The audit should begin with management responsibility and quality culture. Does the factory understand customer requirements? Are quality objectives visible? Are operators trained? Are nonconforming products separated? Are corrective actions closed effectively? A clean and organized factory is not a guarantee of precision, but poor organization is often a warning sign.Incoming material control is critical. Buyers should verify steel supplier approval, material certificates, chemical composition checks, batch identification, and storage conditions. For chrome steel needle rollers, material quality directly affects fatigue life. For stainless steel rollers, composition and corrosion resistance must be confirmed. For ceramic rollers, powder quality, sintering control, and surface integrity are essential.Heat treatment audit points include furnace control, temperature records, quenching medium management, tempering parameters, hardness testing, microstructure inspection, and distortion control. Grinding and finishing audit points include machine condition, wheel dressing, coolant control, burn prevention, diameter grouping, surface finish measurement, and automated defect detection when available. Final inspection should include dimensional measurement, visual inspection, crack detection if required, hardness checks, cleanliness inspection, and packing verification.Audit AreaWhat to CheckEvidence to RequestPass VS Risk SignalIncoming materialApproved steel source, batch identification, and certificates.Material reports and warehouse labels.Pass: traceable lots; risk: mixed material without records.Heat treatmentTemperature control, hardness, microstructure, and quenching records.Furnace charts and hardness logs.Pass: controlled parameters; risk: no documented settings.Grinding processDiameter control, surface finish, coolant, and burn prevention.SPC records and inspection sheets.Pass: process data; risk: final sorting only.Inspection roomGauge calibration, measurement environment, and operator skill.Calibration certificates and work instructions.Pass: reliable measurement; risk: uncalibrated tools.TraceabilityBatch number from raw material to shipment.Traveler cards, labels, and ERP records.Pass: quick trace; risk: impossible containment.PackingRust prevention, labeling, sealing, and export pallet quality.Packing photos and shipment checklist.Pass: seaworthy packing; risk: corrosion during transit.Corrective actionComplaint handling and root cause analysis.8D reports or corrective action records.Pass: verified prevention; risk: repeated issues.Auditors should also compare what is written in the control plan with what happens on the shop floor. If the control plan says inspection every hour but operators cannot show records, the system is not reliable. If nonconforming parts are stored near approved parts without clear labeling, mix-up risk is high. If measuring equipment is not calibrated, even attractive inspection reports may be questionable.For remote global buyers, a practical audit package may include a factory profile, certificate copies, equipment list, process flow chart, control plan, sample inspection report, packing photos, export references, and a live video meeting. Buyers should also request a trial shipment and inspect the arrival condition after sea freight. Packaging that looks fine at the factory may fail after humidity, vibration, container temperature changes, and long transit.OEM customization is common when standard needle rollers do not fully meet space, load, noise, life, or assembly requirements. Custom services may include non-standard diameter, special length, end crowning, chamfer modification, diameter grouping, special heat treatment, corrosion-resistant material, low-noise surface finishing, special oiling, clean-room packaging, private labeling, and documentation packages for production approval.Drawn cup needle roller bearings use thin-walled outer rings and needle rollers to provide high load capacity in compact spaces. They are common in automotive transmissions, power tools, pumps, appliances, and light industrial equipment. The roller must match the drawn cup geometry, cage design, and shaft condition. If the roller surface or size variation is poor, the bearing may create noise, heat, or premature wear.Thrust needle roller assemblies support axial loads in compact designs. They are used in transmissions, torque converters, clutches, compressors, gear sets, and industrial machinery. In thrust applications, roller length, end geometry, and surface finish influence contact stress and sliding behavior. A small inconsistency may become significant under repeated axial loading.Customization should follow a controlled development process. The buyer provides drawings, application details, target annual volume, and performance requirements. The supplier reviews manufacturability and recommends practical tolerances. Samples are produced and inspected. The buyer tests assembly fit and performance. After approval, production documents are locked. Any change to material, heat treatment, equipment, or inspection method should be communicated before implementation.For many OEMs, the ideal supplier is not only a manufacturer but also a technical partner. A good partner can explain the cost impact of tighter tolerance, recommend rust prevention for ocean shipping, suggest packaging for automated feeding, and support failure analysis. This service capability is especially valuable for global teams where design is in Europe, purchasing is in North America, production is in Mexico, and suppliers are in Asia.SDBALLS has developed service capabilities through long-term support of international customers in precision rolling elements. Its team can help buyers coordinate drawings, sample communication, packaging requests, and sourcing consolidation. Customers working in caster wheels, sliding systems, ball transfer units, bearings, automotive components, and mechanical systems can also explore application insights through the application resources.Material choice has a direct impact on life, corrosion resistance, price, noise, density, and application suitability. Chrome steel is the default choice for most high-load bearing and gearbox applications. It provides excellent hardness and fatigue strength after proper heat treatment. Its weakness is corrosion susceptibility, so it requires appropriate oiling, packaging, and lubrication. In humid routes such as ocean freight through tropical ports, anti-rust protection is not optional.Stainless steel needle rollers are selected when corrosion resistance is more important than the lowest cost. AISI 440C can be hardened and used in bearing-like applications, while 304 and 316 are more corrosion-resistant but not equivalent in hardness for high-load rolling contact. Buyers must avoid assuming that all stainless steels are interchangeable. The correct grade depends on load, corrosion medium, temperature, and expected life.Ceramic needle rollers are used for special applications where low density, electrical insulation, high hardness, or chemical resistance is beneficial. Silicon nitride is common in high-performance rolling applications, while zirconia offers toughness and corrosion resistance in certain environments. Ceramic rollers are generally more expensive and require careful mating material design. They are not a universal upgrade; they are a specialized solution.For 2026 and beyond, material trends include cleaner bearing steels, improved heat treatment consistency, hybrid bearing designs, advanced coatings, lower-carbon steel production, and recyclable packaging. Electric vehicles also create new requirements, including reduced friction, higher rotational speed, improved NVH behavior, and resistance to electrical damage in some systems. Industrial automation and robotics demand compact, low-maintenance components with predictable life.Procurement should always connect material selection to the operating environment. A low-cost chrome steel roller may be excellent inside a sealed lubricated gearbox but unsuitable for a wet outdoor mechanism. A stainless roller may resist corrosion but fail under high contact stress if the wrong grade is chosen. A ceramic roller may solve electrical or speed issues but create cost or compatibility challenges.SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., is a precision rolling element manufacturer and integrated supply partner based in Tai'an City, Shandong Province, China. Since 1996, the company has built manufacturing experience in precision steel balls and related supply chain services for customers across the Global Market. Its facilities support large-scale production, stable quality control, and export service for buyers in more than 50 countries.From a technological capability perspective, SDBALLS focuses on material selection, forming accuracy, heat treatment control, grinding and polishing quality, grade management, inspection discipline, and application understanding. Its core product range includes carbon steel balls, chrome steel balls, and stainless steel balls from precision grades to general-purpose grades. This technical foundation is relevant for buyers who require consistent rolling element performance, controlled surfaces, and traceable batches.From a manufacturing capability perspective, SDBALLS operates multiple production facilities with significant annual capacity. The company’s experience in high-volume precision steel ball manufacturing supports process stability, cost control, and consistent delivery. While needle rollers have their own production requirements, buyers sourcing related rolling elements often value a partner that understands the broader bearing, automotive, hardware, and mechanical component ecosystem.From a service capability perspective, SDBALLS offers international sales support, export coordination, packaging communication, and integrated sourcing assistance. In addition to its own manufactured steel balls, the company helps customers consolidate procurement for multi-material spheres such as plastic, glass, ceramic, copper, and aluminum. This integrated approach can reduce supplier complexity for global buyers managing multiple components, specifications, and shipping schedules.For companies sourcing needle rollers, bearing balls, steel balls, or related rolling components, SDBALLS can be considered as a practical partner for technical communication and procurement consolidation. The company’s certified quality systems, export experience, and customer-focused support model align with the needs of global manufacturers seeking stable supply, consistent documentation, and long-term cooperation.The most important factor is consistent process control. Price matters, but diameter variation, hardness stability, surface finish, cleanliness, and traceability determine actual performance. A supplier with stable manufacturing and inspection systems is safer than a low-cost supplier with uncertain quality.ISO 9001 can be enough for general industrial applications if the supplier provides reliable inspection and traceability. For automotive, gearbox, and high-volume OEM projects, IATF 16949 or automotive-quality documentation is strongly recommended.Chrome steel is usually better for high-load bearing fatigue performance and cost efficiency. Stainless steel is better for corrosion resistance. The right choice depends on load, lubrication, moisture, chemical exposure, and life requirements.Buyers should request drawings, material certificates, dimensional inspection reports, hardness reports, surface finish data, process flow charts, control plans, packing specifications, and certificates. Automotive projects may also require PPAP, PFMEA, MSA, and SPC records.They can share rolling forecasts, approve samples early, hold safety stock, use scheduled shipments, and agree on reorder points. For critical production, buyers should avoid ordering only after inventory is nearly exhausted.The audit should check material control, heat treatment, grinding, finishing, inspection equipment, calibration, traceability, nonconforming product control, packaging, corrective action, and export readiness. Remote audits should include live video and document review.No. Ceramic needle rollers are useful for special requirements such as low density, electrical insulation, or chemical resistance, but they are more expensive and must be validated carefully. They are not automatically better for every gearbox or bearing design.Important trends include digital inspection, AI-supported quality monitoring, cleaner steel, carbon footprint reporting, recyclable packaging, dual-source strategies, regional warehousing, electric vehicle drivetrain requirements, and stricter supplier transparency.Yes, if the supplier has manufacturing experience, technical understanding, and integrated sourcing capability. This approach can reduce communication cost and simplify supplier management, especially for buyers sourcing steel balls, bearing components, and related precision parts.SDBALLS combines decades of precision steel ball manufacturing experience, certified quality systems, export service, and integrated supply support. For global buyers, this can help simplify procurement, improve communication, and support stable long-term cooperation.Needle roller sourcing in the Global Market requires a balance of engineering precision, supplier verification, certification review, logistics planning, and cost control. Buyers who define specifications clearly, audit suppliers carefully, validate samples properly, and manage inventory proactively will achieve more reliable bearing and gearbox performance. In 2026, the strongest procurement strategies will combine technical discipline with supply chain resilience, sustainability awareness, and long-term supplier partnerships. -
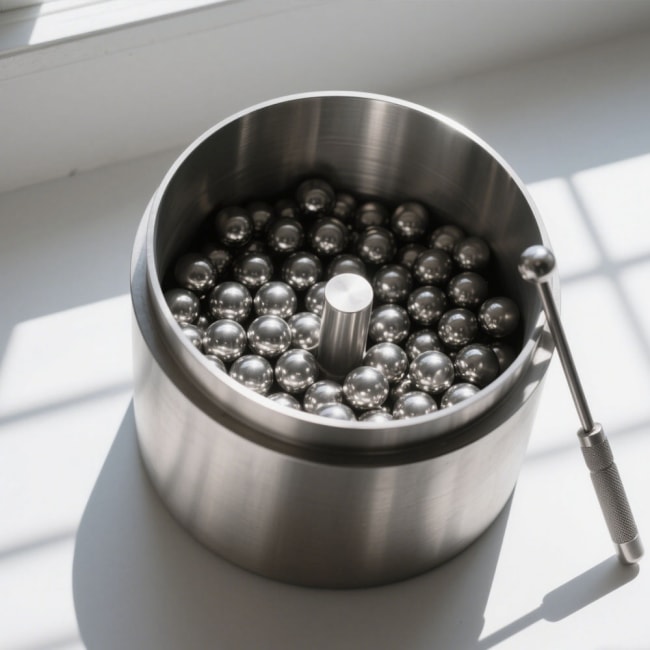
Global Market Bearing Cage Supplier for Precision OEMs
A reliable ball bearing cage manufacturer for the Global Market should combine material expertise, precision forming or machining capability, certified quality systems, engineering support, and stable delivery performance. Buyers should evaluate whether the supplier can produce brass, steel, polyamide, bronze, and aluminum cages; whether it can support taper, spherical, cylindrical, and custom window-type cage designs; and whether it operates under recognized systems such as IATF 16949:2016 and ISO 9001. For critical bearing assemblies, supplier selection should not be based on unit price alone. Cage dimensional accuracy, pocket geometry, fatigue resistance, surface finish, traceability, and batch consistency directly affect bearing noise, friction, temperature rise, load distribution, and service life.For OEMs, distributors, bearing plants, automotive component manufacturers, electric motor producers, industrial gearbox builders, and maintenance supply chains, the most practical sourcing approach is to define the application first: speed, load, lubrication, temperature, vibration, corrosion exposure, assembly method, and target service life. The cage material and design should then be matched to those conditions. Brass and bronze are often chosen for strength, machinability, and demanding industrial service. Steel cages are widely used for cost-effective strength and mass production. Polyamide cages can provide low weight and low friction in many moderate-temperature applications. Aluminum cages are attractive where reduced rotating mass is important. Custom window-type cages are used when standard geometry cannot meet assembly, lubrication, or performance requirements.Global Market buyers also need to consider logistics. Bearing cage procurement frequently involves cross-border supply chains moving through trade hubs such as Shanghai, Qingdao, Ningbo, Shenzhen, Singapore, Rotterdam, Hamburg, Dubai, Los Angeles, Chicago, Houston, and Mexico City. A supplier with strong lead time management, export documentation experience, stable packaging standards, and long-term supply agreement structures can reduce production risk. For a buyer seeking a long-term partner rather than a one-time vendor, the best choice is a manufacturer or integrated supply partner that can participate early in design, manage tooling, provide inspection records, support volume pricing, and maintain consistent communication across time zones.SDBALLS Industry Corp is known globally for precision steel ball manufacturing and integrated supply support. While its core manufacturing strength is in carbon steel balls, chrome steel balls, stainless steel balls, and related spherical products, its broader supply chain service model helps international buyers consolidate sourcing for precision components used in bearings, automotive systems, sliding systems, caster wheels, ball transfer units, and industrial assemblies. For cage buyers, this type of integrated supplier mindset is valuable because cage performance must be aligned with rolling elements, raceways, lubrication, and assembly conditions.Material selection is one of the most important decisions in bearing cage procurement. The cage separates rolling elements, guides their motion, reduces contact between adjacent balls or rollers, and supports stable lubrication distribution. Even when the cage does not carry the main radial or axial load, its failure can cause catastrophic bearing damage. Therefore, buyers in the Global Market should evaluate cage materials according to mechanical strength, heat resistance, weight, corrosion behavior, manufacturability, cost, and compatibility with lubricants.Brass cages are frequently used in applications requiring good strength, wear resistance, machinability, and dimensional stability. They are common in industrial bearings, heavy-duty rotating equipment, pumps, compressors, marine systems, mining machinery, and rail-related applications. Brass performs well under many lubricated conditions and is often selected when buyers need a robust cage for medium to high loads. However, brass costs more than many stamped steel alternatives, and its weight may be a disadvantage in extremely high-speed applications.Steel cages are among the most widely used options due to their strength, availability, and cost efficiency. Stamped steel cages are common in high-volume ball bearings, automotive bearings, electric motors, household appliances, agricultural machinery, and general industrial equipment. Machined steel cages may be used when higher strength or special geometry is required. Steel cages require careful attention to surface treatment, burr control, corrosion protection, and dimensional consistency. For global OEM supply, steel cage suppliers should demonstrate strong process control because small deviations in pocket size or rivet quality can affect bearing noise and vibration.Polyamide cages, especially reinforced engineering plastics, are used where low weight, low friction, low noise, and efficient high-speed performance are desired. They are common in electric motors, automotive auxiliary systems, power tools, light industrial equipment, and certain precision assemblies. Polyamide cages can reduce rotating mass and support smoother operation, but buyers must check operating temperature, chemical exposure, lubricant compatibility, and aging behavior. For applications exposed to high heat, aggressive oils, or long-term thermal stress, metal cages may be safer.Bronze cages provide excellent wear resistance and are often used in heavy industrial bearings, marine systems, large machinery, and applications with shock loads or difficult lubrication conditions. Bronze may be selected when brass is not sufficient or when buyers need specific friction and wear characteristics. Aluminum cages offer low weight, good machinability, and corrosion resistance in selected environments. They are considered in aerospace-related equipment, high-speed rotating assemblies, lightweight industrial mechanisms, and custom designs where mass reduction is important.The following table compares common cage materials from a procurement and engineering perspective.MaterialTypical StrengthSpeed SuitabilityCost PositionBest-Fit ApplicationsVS Main AlternativeBrassHighMedium to highMedium to highIndustrial bearings, pumps, compressors, heavy equipmentVS steel: better machinability and wear behavior, but higher material costSteelHighMedium to highLow to mediumAutomotive bearings, electric motors, machinery, appliancesVS brass: more economical for volume production, but requires corrosion controlPolyamideMediumHigh in suitable temperaturesLow to mediumLow-noise bearings, motors, tools, light-duty assembliesVS steel: lighter and quieter, but less suitable for high heatBronzeHighMediumHighMarine, mining, large industrial machinery, shock-load conditionsVS brass: stronger wear performance in selected applications, but more expensiveAluminumMediumMedium to highMediumLightweight rotating systems, custom precision assembliesVS brass: lower weight, but lower wear resistance in many heavy-duty casesHybrid or coated designsApplication-dependentApplication-dependentMedium to highSpecial OEM projects, high-value assemblies, harsh environmentsVS standard material: better tailored performance, but longer development timeThis comparison shows that no single material is best for every bearing cage. A buyer should not simply request the cheapest cage material. Instead, the supplier should help translate application requirements into cage design criteria. For example, a low-noise electric motor exported to Europe may prioritize polyamide cage stability and low vibration. A mining gearbox operating in Australia, Chile, South Africa, or Canada may need brass or bronze cages with proven fatigue resistance. A high-volume automotive bearing program in Germany, Mexico, the United States, China, India, Japan, or Thailand may require steel cages with IATF documentation and strong production repeatability.Ball bearing cages and related rolling bearing cages are produced in many geometries. The cage type depends on bearing structure, rolling element shape, load direction, assembly method, lubrication method, and speed requirement. A professional cage supplier should understand how cage geometry interacts with rolling elements and raceways. For buyers in the Global Market, this capability is especially important when sourcing from overseas suppliers because drawings alone may not fully communicate functional requirements.Taper cage designs are commonly associated with tapered roller bearings or special angular load applications. Their geometry must support accurate roller guidance and stable load distribution. Spherical cage designs are used in spherical roller bearings or self-aligning bearing structures where misalignment accommodation is important. Cylindrical cage designs support cylindrical roller bearing applications, including motors, gearboxes, construction machinery, wind energy systems, and heavy industrial equipment. Custom window-type designs are created when pocket shape, lubrication flow, assembly process, or rolling element retention requires non-standard features.In precision assemblies, the cage window is not merely an empty space. Window size, edge radius, bridge thickness, pocket clearance, surface roughness, and forming accuracy affect friction and rolling element guidance. Poor cage design can cause skidding, cage instability, heat generation, abnormal noise, lubricant starvation, and premature failure. Therefore, cage manufacturers should use design review, prototyping, tooling simulation, inspection, and functional testing to confirm performance before mass production.Cage TypeCommon Bearing MatchKey Design FocusManufacturing ChallengeTypical Market UseVS Standard CageTaper cageTapered roller bearingRoller guidance and axial load stabilityMaintaining pocket angle and bridge strengthAutomotive hubs, gearboxes, heavy vehiclesVS flat cage: better suited for combined radial and axial loadsSpherical cageSpherical roller bearingMisalignment tolerance and roller stabilityComplex geometry and high machining accuracyMining, paper mills, marine shafts, wind equipmentVS cylindrical cage: better for self-aligning conditionsCylindrical cageCylindrical roller bearingHigh radial load and roller separationControlling pocket parallelism and roundnessMotors, gearboxes, pumps, machine toolsVS spherical cage: simpler for aligned shafts and high radial loadsCustom window-type cageSpecial ball or roller bearingLubrication, retention, assembly, and noise controlTooling development and validation testingOEM equipment, robotics, automation, aerospace-related assembliesVS catalog cage: optimized for exact operating requirementsRibbon or crown cageDeep groove ball bearingHigh-volume assembly and low frictionBurr control and stamping consistencyAppliances, motors, fans, small machineryVS machined cage: lower cost for mass productionMachined solid cageHeavy-duty bearingRigidity and long service lifeMaterial removal, balance, and dimensional precisionSteel mills, marine propulsion, energy equipmentVS stamped cage: stronger but more expensiveThe table highlights an important purchasing principle: cage type must be selected according to functional need, not only bearing size. For example, a high-load conveyor bearing used near Rotterdam port logistics, a wind turbine bearing installed in North Sea conditions, and an automotive wheel bearing assembled in Monterrey may all require different cage structures even if their outer dimensions appear comparable. Global Market buyers should ask suppliers to review application data, not only drawings.For custom window-type cage projects, early supplier involvement is valuable. Tooling experts can advise on whether a pocket shape is stampable, machinable, moldable, or better produced through a hybrid process. They can also suggest bridge thickness changes, corner radius improvements, relief angles, or surface treatment changes that reduce fatigue risk without changing the bearing envelope. Such practical design-stage feedback often prevents costly tooling revisions after prototype testing.Certification is not a guarantee of perfect parts, but it is an important baseline for supplier qualification. For bearing cage suppliers serving automotive, industrial, and precision assembly customers, ISO 9001 demonstrates a structured quality management system, while IATF 16949:2016 is especially relevant for automotive supply chains. Buyers should confirm not only that a certificate exists, but also that the certified scope covers the processes used for the cage product, such as stamping, machining, molding, heat treatment, surface treatment, inspection, and assembly support.Automotive OEMs and Tier suppliers usually require process documentation such as APQP, PPAP, FMEA, control plans, MSA, SPC data, material traceability, and change control. Even non-automotive buyers can benefit from suppliers that understand these tools because they promote disciplined risk management. A cage supplier that can provide dimensional reports, material certificates, process flow charts, inspection records, and batch traceability is easier to integrate into global procurement systems.For ISO 9001 cage suppliers, buyers should evaluate document control, nonconforming product management, corrective action systems, calibration records, training records, supplier management, customer complaint handling, and continuous improvement practices. For IATF 16949 suppliers, buyers should additionally review automotive-specific requirements such as contingency planning, embedded software exclusion when applicable, product safety awareness, special characteristic control, and customer-specific requirements.RequirementISO 9001 FocusIATF 16949:2016 FocusBuyer Verification MethodRisk if MissingVS Uncertified SupplierQuality management systemProcess-based quality controlAutomotive process disciplineCheck certificate scope and audit reportsInconsistent management of defectsCertified supplier offers clearer accountabilityTraceabilityBatch records and document controlPart-level or lot-level automotive traceabilityRequest sample lot recordSlow containment after defect discoveryStronger recall and root-cause responseAPQP and PPAPNot always requiredCore automotive requirementReview PPAP package capabilityDelayed OEM approvalBetter launch readiness for new programsMeasurement systemCalibration and inspection controlMSA and special characteristic controlReview gauge R&R and calibration recordsFalse acceptance or rejectionMore reliable inspection decisionsProcess capabilityGeneral performance monitoringSPC and capability evidenceAsk for Cp and Cpk dataDimensional drift in mass productionBetter high-volume consistencyChange managementControlled documented changesCustomer approval for relevant changesReview change notice procedureUnexpected material or process variationLower risk for long-term programsIn the Global Market, certification requirements may vary by industry and region. German automotive groups, Japanese bearing producers, American equipment manufacturers, Korean electronics suppliers, Indian industrial exporters, and European rail suppliers may all ask for different documentation formats. A capable supplier should be able to communicate in a structured way and adapt documentation to customer requirements. It should also be transparent about what it can and cannot certify. If a supplier claims compliance but cannot provide process records, inspection data, or change control evidence, buyers should proceed cautiously.SDBALLS maintains recognized quality systems including IATF 16949, ISO 9001, and ISO 14001 for its precision steel ball operations and supply chain services. This quality culture matters because rolling elements and cages work together inside bearing assemblies. When sourcing precision components, buyers benefit from partners who understand tolerance control, batch consistency, inspection discipline, and international customer expectations. More information about the company’s standards can be found through its quality and technical support resources.OEM co-development means the cage supplier participates before mass production begins. Instead of receiving a finished drawing and quoting only a price, the supplier helps evaluate material, geometry, process feasibility, tooling approach, inspection method, assembly compatibility, and production risk. This is especially important for new bearing programs, upgraded platforms, localized replacement parts, electric vehicle components, robotics assemblies, industrial automation equipment, and high-speed motor applications.Design-stage involvement can reduce total cost even if it increases early engineering discussion. A tooling engineer may identify that a pocket corner is too sharp for stamping without cracking, that a bridge is too thin for fatigue life, or that a polymer cage needs a different gate position to reduce warpage. A quality engineer may suggest special characteristic controls for critical pocket dimensions. A production engineer may advise whether the projected annual volume justifies progressive die tooling, CNC machining, injection molding, or a staged production approach.Tooling expertise is particularly important for custom window-type cage designs. Tooling cost, tooling life, maintenance intervals, cavity balance, trimming accuracy, and setup repeatability all affect long-term economics. Buyers should ask the supplier to explain the tooling concept, expected life, spare parts plan, maintenance responsibilities, and ownership terms. If a buyer pays for tooling, the contract should define whether the tooling is customer-owned, supplier-owned, transferable, or restricted to exclusive use.The Global Market has become more demanding because OEMs need faster product launches and more resilient supply chains. Automotive electrification, warehouse automation, renewable energy equipment, rail modernization, medical devices, and compact industrial machinery all place new demands on bearing systems. Cage suppliers must therefore support not only drawings but also application problem-solving. Early engineering communication across cities and trade hubs such as Detroit, Stuttgart, Nagoya, Seoul, Pune, Shanghai, Milan, São Paulo, and Istanbul can help align technical expectations before production begins.A practical co-development process usually includes application review, drawing analysis, material proposal, tolerance discussion, prototype manufacturing, sample inspection, functional testing, tooling design, pilot production, PPAP or first article approval, and mass production launch. For critical assemblies, the supplier should also support failure analysis if testing reveals wear marks, cage deformation, abnormal noise, or lubrication issues. The goal is to establish a stable product and process before volume production commitments are made.Quality control for bearing cages must be both dimensional and functional. CMM inspection can verify key geometry such as pocket position, pitch accuracy, roundness, concentricity, flatness, bridge width, and reference datum relationships. Optical inspection may be used for burrs, edge quality, surface defects, and window shape. Material testing verifies chemistry, hardness, tensile properties, and heat treatment condition where applicable. Fatigue testing and endurance testing evaluate whether the cage can survive repeated loading, vibration, speed, and temperature cycles.Dimensional accuracy is critical because rolling elements need controlled clearance inside cage pockets. Excessive clearance may cause noise, impact, skewing, and unstable motion. Insufficient clearance may increase friction, heat, and seizure risk. Pocket surface finish also matters because rough surfaces can damage lubricant films or create wear debris. For stamped cages, burr direction and trimming quality should be controlled. For machined cages, tool marks, sharp edges, and residual stress should be reviewed. For molded polyamide cages, shrinkage, warpage, moisture conditioning, and fiber orientation may affect performance.A robust quality plan should define incoming material inspection, in-process checks, final inspection, sampling frequency, acceptance criteria, nonconformance handling, and records retention. For high-volume automotive or bearing plant supply, statistical process control is often required. For lower-volume custom cages, first article inspection and 100% checks on critical features may be justified. Buyers should also confirm whether the supplier can provide CMM reports in formats compatible with their engineering systems.Inspection ItemMethodPurposeTypical FrequencyImportant forVS Visual Check OnlyPocket size and positionCMM, optical measurement, gaugesEnsure rolling element guidanceFirst article and periodic production checksNoise, friction, speed stabilityProvides measurable accuracy instead of subjective judgmentRoundness and concentricityCMM, roundness testerMaintain cage balance and smooth rotationBatch sampling or critical part inspectionHigh-speed bearings and precision assembliesDetects geometry errors that eyes cannot seeBurr and edge conditionMicroscope, tactile inspection, optical systemPrevent wear debris and assembly damageIn-process and final inspectionStamped steel and brass cagesMore reliable than quick visual scanningMaterial compositionSpectrometer or material certificate verificationConfirm correct alloy or polymer gradeIncoming lot inspectionAll cage materialsPrevents substitution and performance variationFatigue performanceEndurance rig, vibration and load cyclingValidate long-term durabilityPrototype, validation, and periodic auditsHeavy-duty and safety-related applicationsReveals service risk not visible in static inspectionSurface finishProfilometer, optical analysisControl friction and wear behaviorProcess qualification and samplingMachined and high-speed cagesQuantifies finish instead of estimating by appearanceQuality control is also linked to supplier culture. A supplier that records problems honestly and responds quickly is often more valuable than a supplier that claims zero defects without evidence. Buyers should ask for examples of corrective action reports, root-cause analysis methods, containment procedures, and improvement projects. In global supply chains, communication speed matters. If a bearing assembly line in Poland, Mexico, Vietnam, or Ohio faces a cage-related issue, the supplier must help identify affected lots and respond with practical containment actions.SDBALLS has built its reputation in precision steel balls by controlling grade, surface quality, hardness, and dimensional consistency across large production volumes. These capabilities reflect an understanding of precision rolling contact components. The company operates multiple production facilities and supports global customers with technical communication, inspection discipline, and export experience. Buyers interested in related precision component capability can review the company’s product portfolio.Minimum order quantity, volume pricing, and supply agreement structure are commercial issues, but they have strong technical and operational implications. A custom bearing cage may require dedicated tooling, special material procurement, fixture design, and inspection programming. Therefore, the MOQ for a custom cage is usually higher than for a standard cage. Conversely, if the cage is made from existing tooling or belongs to a common size range, the supplier may offer lower MOQ or faster delivery.Buyers should distinguish between sample MOQ, pilot MOQ, production MOQ, and annual volume commitment. A sample order may be used for prototype testing and design approval. A pilot order verifies process stability and assembly compatibility. Production MOQ reflects efficient manufacturing batch size. Annual commitment supports volume pricing, material planning, and capacity reservation. Long-term supply agreements may include price breaks, forecast windows, safety stock, tooling amortization, raw material adjustment formulas, and quality performance targets.Volume pricing should be analyzed beyond unit price. Buyers should include tooling cost, inspection cost, packaging cost, freight, customs duties, inventory carrying cost, payment terms, defect risk, and communication efficiency. A slightly higher unit price may be more economical if the supplier provides stable quality, fewer line stoppages, better documentation, and shorter response time. For bearing assembly plants, the cost of production interruption can exceed the savings from low-cost cages.Commercial ModelBest ForBuyer AdvantageSupplier AdvantagePotential RiskVS Spot BuyingSample orderPrototype testing and supplier evaluationLow initial commitmentOpportunity to prove capabilityUnit price may be highMore controlled than buying unknown stockPilot production orderPre-launch validationChecks real production processConfirms tooling and workflowSchedule pressure before approvalReduces mass production surprisesStandard MOQ orderRegular replacement or small programsBalances cost and inventoryEfficient batch planningLess price leverageMore stable than random purchase ordersAnnual blanket orderRecurring OEM demandBetter price and capacity planningForecast visibilityForecast accuracy requiredImproves delivery reliabilityLong-term supply agreementStrategic componentsSecures quality, price structure, and supplySupports investment in tooling and stockRequires contract managementFar stronger than short-term negotiationVendor-managed inventoryHigh-volume assembly plantsLower stockout riskCloser customer relationshipNeeds data transparencyMore resilient for critical production schedulesFor the Global Market, payment and logistics terms also affect total cost. Common trade terms may include EXW, FOB, CIF, DAP, or DDP depending on buyer capability and destination. Ports such as Qingdao, Shanghai, Ningbo, Shenzhen, Busan, Singapore, Jebel Ali, Rotterdam, Antwerp, Hamburg, Long Beach, and Savannah are frequently involved in global industrial component logistics. Air freight may be justified for urgent prototypes or line-down situations, but sea freight is typically more economical for regular cage supply.Long-term agreements should define quality expectations, inspection documentation, packaging, labeling, delivery windows, forecast updates, raw material change notices, engineering change control, confidentiality, and dispute resolution. If tooling is involved, the agreement should specify ownership, storage, maintenance, replacement, and end-of-life handling. Buyers should also include contingency plans for sudden demand increases, port congestion, geopolitical disruptions, raw material volatility, or supplier capacity constraints.Lead time management is essential for bearing cage procurement because cages are often small components with large consequences. If cages arrive late, bearing assembly lines may stop even if rolling elements, rings, seals, grease, and packaging are ready. For critical production schedules, buyers should evaluate supplier lead time in stages: engineering review time, quotation time, tooling time, sample production, sample inspection, customer approval, raw material procurement, mass production, final inspection, packing, inland transport, export clearance, international freight, customs clearance, and local delivery.Standard cage products may have short lead times if material and tooling are available. Custom cages can require several weeks or months, especially when tooling, mold flow analysis, heat treatment validation, or endurance testing is involved. Buyers should avoid unrealistic launch schedules that skip validation. A fast but poorly validated cage can create failures after assembly, leading to warranty costs and reputation damage.Forecast sharing is a practical way to improve delivery stability. Instead of issuing urgent purchase orders without visibility, buyers should provide rolling forecasts, firm order windows, and expected seasonal changes. Suppliers can then reserve capacity, purchase material, and arrange labor. For high-volume programs, safety stock may be stored at the supplier, buyer, regional warehouse, or third-party logistics center. In North America, warehouses near Chicago, Dallas, Los Angeles, Toronto, or Monterrey may support faster distribution. In Europe, hubs near Rotterdam, Hamburg, Milan, or Katowice can serve multiple countries. In Asia, Shanghai, Qingdao, Shenzhen, Singapore, Bangkok, and Ho Chi Minh City are important logistics nodes.Lead time risk is not only about transport. Engineering delays, unclear drawings, missing material specifications, late approval of samples, and slow payment confirmation can all extend schedules. Buyers can reduce risk by providing complete technical documents, clear revision control, realistic annual volumes, target dates, packaging requirements, and inspection expectations. Suppliers can reduce risk by confirming feasibility early, communicating production status, and alerting customers to potential delays before they become urgent problems.The 2026 sourcing environment is expected to place even more emphasis on resilient lead time management. Policy changes, carbon reporting requirements, regional trade rules, port congestion, and geopolitical uncertainty may affect cross-border procurement. At the same time, digital tools such as supplier portals, electronic quality records, AI-assisted demand forecasting, digital twins for tooling, and automated inspection data exchange will improve transparency. Buyers should prioritize suppliers that are willing to modernize communication and provide data-driven production updates.SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., serves global industrial customers as a precision steel ball manufacturer and integrated supply partner. Founded in 1996 and headquartered in Tai'an City, Shandong Province, China, the company has accumulated more than three decades of manufacturing experience. Its main production strength is in carbon steel balls, chrome steel balls, and stainless steel balls, with precision grades from G10 to G1000. These products are used in bearing assemblies, automotive components, caster wheels, sliding systems, ball transfer units, hardware, grinding applications, and other mechanical systems.From a technological capability perspective, SDBALLS understands the importance of rolling contact performance, dimensional precision, hardness control, surface finish, and batch consistency. These factors are also central to bearing cage sourcing because cages must work in harmony with steel balls, bearing rings, lubricants, and seals. The company’s quality systems, technical support, and inspection discipline allow it to communicate effectively with buyers that require stable precision components for demanding assemblies. Its experience with international standards helps customers manage supplier qualification and documentation requirements.From a manufacturing capability perspective, SDBALLS operates three production facilities with annual capacity exceeding 5,000 tons. This scale supports stable supply for customers across more than 50 countries. In addition to steel balls, the company manufactures lead-free steel shot for hunting and outdoor markets, including annealed and plated solutions designed to meet relevant hardness expectations for EU and US markets. This combination of volume production, precision control, and material processing experience gives SDBALLS a strong foundation for supporting global procurement programs related to bearings and mechanical assemblies.From a service capability perspective, SDBALLS acts not only as a manufacturer but also as an integrated supply partner. The company helps buyers consolidate sourcing for multi-material spheres including plastic, glass, ceramic, copper, and aluminum products. This service model is useful for global procurement teams that need fewer suppliers, clearer communication, and more coordinated logistics. For customers sourcing bearing cages, rolling elements, or related precision components, the same integrated approach can help align technical requirements, quality expectations, and delivery schedules. To learn more about its background, buyers can visit the SDBALLS company overview.The company serves customers in many sectors, including bearing manufacturing, automotive systems, industrial equipment, outdoor shooting products, hardware, material handling, and precision mechanical assemblies. Its dedicated global sales team and US business support help international customers communicate more efficiently across time zones. Buyers can also explore typical use cases through the company’s application information, which shows how precision spherical components support real-world mechanical performance.For bearing cage buyers, SDBALLS is relevant as a supply chain partner because successful bearing assembly depends on more than one component. Steel ball grade, cage geometry, ring accuracy, lubricant quality, and assembly cleanliness all contribute to final performance. A partner experienced in precision rolling elements can help procurement teams think more systematically about component compatibility, inspection expectations, and long-term cooperation.What is the fastest way to qualify a ball bearing cage manufacturer for the Global Market?The fastest responsible way is to combine document review, technical discussion, sample inspection, and pilot production. Buyers should check ISO 9001 or IATF 16949 certification, material capability, drawing interpretation, inspection equipment, CMM reporting, tooling experience, and export performance. For critical applications, do not skip prototype testing or fatigue validation.Which cage material is best for high-speed bearings?There is no universal answer. Polyamide cages can be excellent for many high-speed, low-noise, moderate-temperature applications. Brass or machined metal cages may be preferred when strength, heat resistance, or heavy-duty stability is required. Aluminum can be considered when low weight is important. The final choice should consider speed, load, temperature, lubricant, and service life.Are brass cages better than steel cages?Brass cages are often stronger in wear behavior and machinability for demanding industrial applications, but steel cages are highly cost-effective and widely used in mass production. Brass is not automatically better; it is better for certain operating conditions. Steel may be the better choice for high-volume automotive or general industrial bearings when properly designed and protected.When should an OEM choose a custom window-type cage?An OEM should consider a custom window-type cage when standard cage geometry cannot meet requirements for rolling element retention, lubrication flow, assembly method, noise reduction, speed stability, or fatigue life. Custom designs are also useful when a bearing must fit a special envelope or work under unusual load, vibration, or temperature conditions.Why is CMM inspection important for bearing cages?CMM inspection verifies critical dimensions and geometric relationships that affect cage function. Pocket size, pocket position, concentricity, flatness, and roundness can influence bearing noise, friction, heat generation, and rolling element stability. Visual checks alone cannot confirm these precision features reliably.What documents should a cage supplier provide for automotive projects?Automotive projects often require APQP records, PPAP packages, process flow diagrams, control plans, FMEA, material certificates, dimensional inspection reports, MSA, SPC data, and traceability records. Customer-specific requirements may also apply. IATF 16949:2016 capability is strongly preferred for automotive supply chains.How can buyers reduce lead time risk for custom cages?Buyers can reduce risk by providing complete drawings, material specifications, annual volume forecasts, sample approval timelines, packaging instructions, and realistic launch schedules. They should also confirm tooling lead time, material availability, inspection requirements, logistics routes, and contingency stock plans before placing production orders.What MOQ should buyers expect for bearing cages?MOQ depends on material, design, tooling, production method, and whether the cage is standard or custom. Standard cages may have lower MOQ, while custom cages with dedicated tooling usually require higher batch quantities. Buyers should discuss sample MOQ, pilot MOQ, production MOQ, and annual commitment separately.What 2026 trends will affect bearing cage sourcing?Key trends include electrification, low-noise bearing demand, lightweight cage materials, automated inspection, digital quality records, AI-based forecasting, carbon reporting, recyclable materials, regionalized supply chains, and stricter supplier transparency. Sustainability and traceability will become more important in both automotive and industrial markets.How does SDBALLS support global procurement teams?SDBALLS supports global buyers through precision steel ball manufacturing, quality-certified operations, international sales service, export experience, and integrated sourcing for related spherical components. Its manufacturing and service model helps buyers consolidate procurement, improve communication, and support long-term cooperation across global markets.