S110 Steel Shot Specs and Buying Guide for Global Market
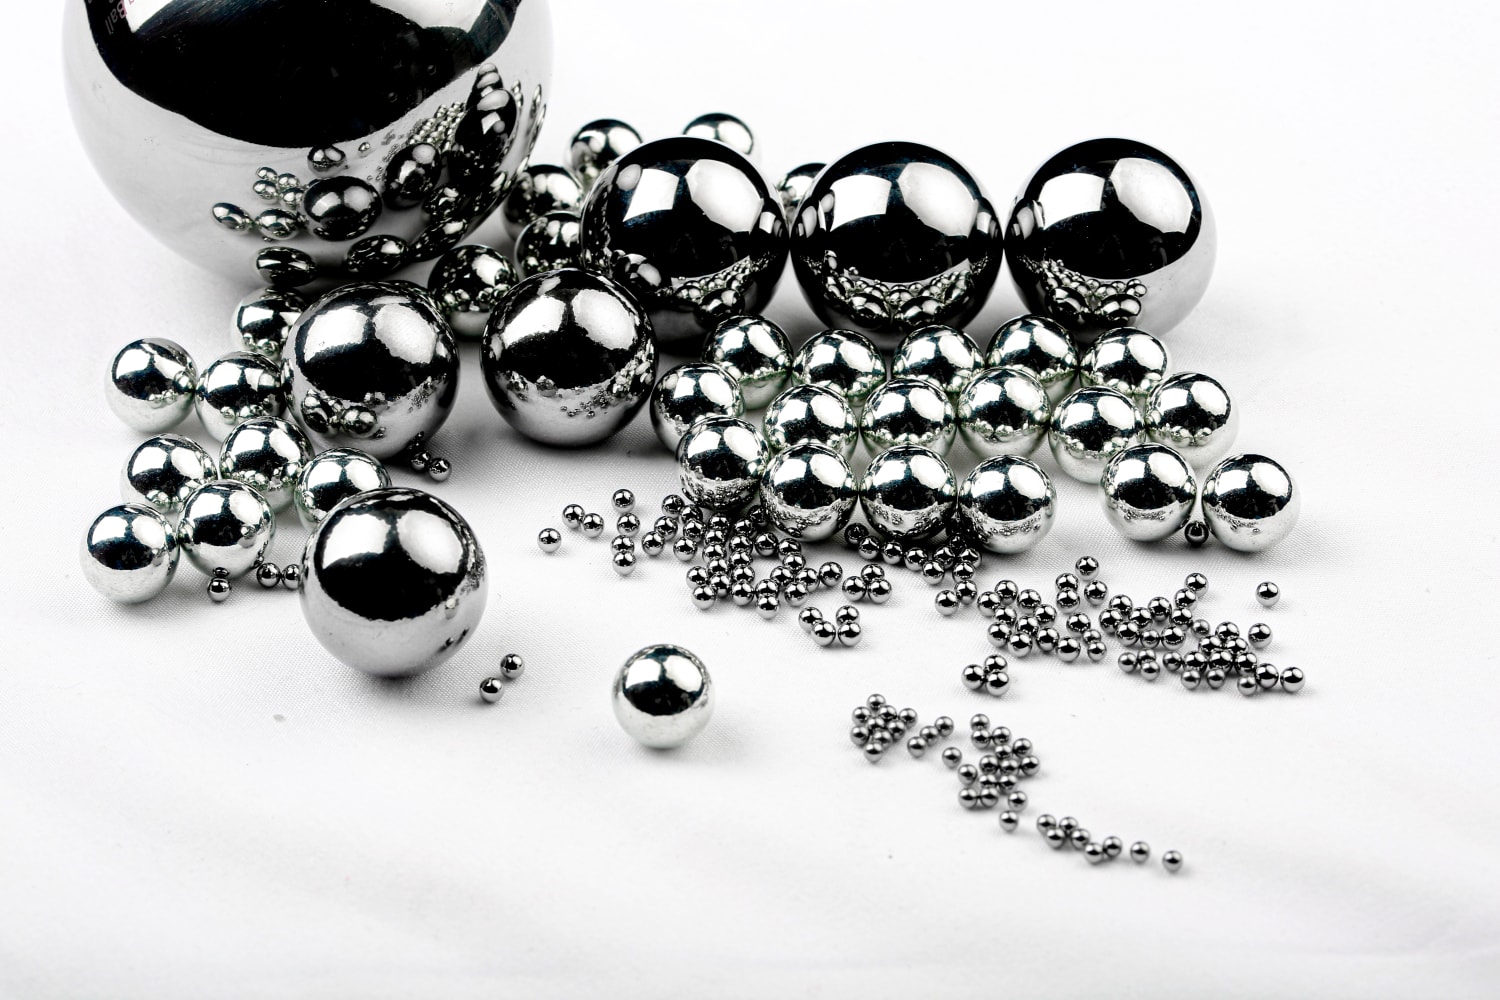
S110 Steel Shot Technical Specifications and Buying Guide for the Global Market
Quick Answer

S110 steel shot is a small, spherical, cast steel abrasive with a nominal diameter of about 0.3 mm, commonly used for light blast cleaning, precision surface preparation, deburring, descaling, and controlled shot peening. For buyers in the Global Market, the most important points are size distribution, chemical composition, hardness grade, microstructure, cleanliness, durability, and consistency from batch to batch.
In practical purchasing terms, S110 is selected when the workpiece needs a fine, uniform impact profile rather than aggressive cutting. It is often used on small castings, automotive components, springs, gears, aluminum die castings, precision machined parts, and delicate surfaces where larger shot such as S170 or S230 may create excessive roughness. A typical S110 specification references SAE J444 for size and SAE J827 or equivalent standards for steel shot quality, while shot peening applications may also reference SAE AMS 2431, AMS 2430, or customer-specific aerospace and automotive standards.
The nominal diameter of S110 is generally understood as approximately 0.3 mm, but buyers should not rely only on a single nominal number. Actual acceptance depends on sieve distribution, oversize limits, undersize limits, and operating mix stability. A high-quality S110 steel shot should have controlled carbon, manganese, silicon, sulfur, phosphorus, and sometimes chromium content, with a sound martensitic or tempered martensitic structure, low hollow particle percentage, low crack ratio, and high resistance to breakage.
For hardness, S110 steel shot is usually supplied in three commercial groups: GP, GL, and GH. GP is general-purpose and comparatively softer, GL is medium-hard and commonly used where higher cleaning energy is required, and GH is hard shot used in more demanding peening or surface preparation situations. The overall hardness range can be around 40 to 68 HRC, depending on grade and specification. Choosing the wrong hardness can increase dust, reduce fatigue performance, damage parts, or shorten abrasive life.
Global buyers sourcing through ports and trade centers such as Shanghai, Qingdao, Ningbo, Singapore, Rotterdam, Hamburg, Los Angeles, Houston, Jebel Ali, and Mumbai should evaluate not only the quoted price per ton but also consumption rate, recyclability, blast machine compatibility, technical documentation, packaging integrity, and supplier quality systems. SDBALLS Industry Corp supports international buyers with precision steel ball manufacturing knowledge, abrasive-related supply capability, quality control systems, and export service experience across more than 50 countries.
| Buyer Question | Quick Answer | Why It Matters | VS Risk If Ignored |
|---|---|---|---|
| What is S110 size? | About 0.3 mm nominal diameter | Controls surface profile and impact energy | Wrong size may over-roughen or under-clean parts |
| Which standard is commonly used? | SAE J444 for size classification | Creates common language between buyer and supplier | Unclear standard leads to disputes |
| Which hardness should I choose? | GP, GL, or GH depending on cleaning or peening need | Determines durability and surface effect | Wrong hardness increases breakage or part damage |
| Is S110 suitable for shot peening? | Yes, when verified by peening requirements | Fine shot can treat small radii and precision areas | Uncontrolled shot may reduce fatigue reliability |
| What should be checked before shipment? | Size, chemistry, hardness, microstructure, packaging | Reduces import and production risk | Poor inspection may cause machine downtime |
| How is value measured? | Cost per cleaned area or cycle life, not only price per ton | Better shot lasts longer and creates less dust | Cheap abrasive may cost more in operation |
The table above shows why S110 steel shot purchasing should be treated as a technical sourcing decision. A low unit price can be attractive, but if the shot breaks quickly, creates too much dust, or fails to maintain a stable operating mix, the real cost becomes higher through labor, disposal, rework, and equipment wear.
S110 Steel Shot Size and Diameter Guide: 0.3 mm Nominal

S110 steel shot is one of the finer commercial steel shot sizes. The “S” identifies steel shot, while “110” indicates a size class rather than an exact diameter for every particle. In common industry communication, S110 is described as having a nominal diameter of about 0.3 mm. However, because shot is produced by atomizing molten steel into spherical particles and then screening, the final product always contains a controlled distribution of particle sizes.
For surface preparation, the small diameter of S110 produces a fine surface texture. It is useful when a buyer needs to remove light scale, clean small castings, or prepare a component for coating without creating a deep anchor profile. In shot peening, smaller shot can reach fillets, gear roots, spring surfaces, turbine-related features, and precision areas where large shot cannot deliver uniform coverage. The fine impact also helps reduce the risk of dimensional distortion on thin or delicate parts.
Size specification should include sieve analysis. Buyers should request a certificate showing retained percentage on relevant sieves, oversize content, and undersize content. A good supplier will control production so that the distribution remains stable from lot to lot. Stable size distribution is especially important in automated blast machines, air blast cabinets, wheel blast systems, and closed-loop peening machines. If the incoming shot contains too many fines, dust loading increases and cleaning efficiency drops. If it contains too many large particles, the workpiece may receive a rougher surface than intended.
In global supply chains, S110 may be packed in 25 kg bags, 1 metric ton big bags, drums, or customized export pallets. Buyers shipping through ports such as Qingdao, Tianjin, Busan, Klang, Antwerp, and Long Beach should ensure moisture-resistant packaging and clear batch labeling. Small shot has a larger surface area per unit mass, so packaging protection is important for preventing rust and contamination during ocean freight.
| Shot Size | Approximate Nominal Diameter | Relative Impact Energy | Typical Surface Profile | S110 VS Other Sizes |
|---|---|---|---|---|
| S70 | About 0.18 to 0.20 mm | Very low | Very fine | S110 gives more cleaning energy than S70 |
| S110 | About 0.30 mm | Low to moderate | Fine and uniform | Balanced for delicate cleaning and fine peening |
| S170 | About 0.43 mm | Moderate | Medium-fine | S170 cleans faster but creates more profile than S110 |
| S230 | About 0.60 mm | Higher | Medium | S230 is more aggressive and less suitable for delicate parts |
| S330 | About 0.85 mm | High | Coarser | S330 is mainly for heavier scale and larger castings |
| S390 and above | About 1.0 mm and larger | Very high | Coarse | Much stronger impact, usually not a substitute for S110 |
This comparison demonstrates that S110 is not simply a smaller version of large blasting media. It fills a specific technical role where surface finish, coverage, and dimensional protection are more important than maximum cleaning aggression. When choosing between S110 and larger sizes, buyers should test on real parts rather than relying only on catalog descriptions.
SAE J444 Chemical Composition Requirements: C, Si, Mn, Cr, S, and P

Chemical composition strongly influences hardness, toughness, microstructure, fatigue performance, and recyclability. Although SAE J444 is widely known for shot size classification, buyers often combine it with steel shot material standards and internal purchase specifications that define chemistry. The elements most often reviewed are carbon, silicon, manganese, chromium, sulfur, and phosphorus.
Carbon is central to hardenability and martensitic structure. Too little carbon may result in insufficient hardness and poor cleaning efficiency. Too much carbon may increase brittleness and breakage. Silicon is commonly used as a deoxidizer and contributes to strength. Manganese improves hardenability and supports toughness when properly balanced. Chromium may be present in controlled amounts to improve wear resistance or hardenability, although not all steel shot is high-chromium material. Sulfur and phosphorus are generally controlled as undesirable elements because excessive levels can reduce toughness and increase cracking.
For international procurement, buyers should ask for a chemical analysis certificate for each heat or batch. The certificate should identify test method, batch number, production date, and traceability. In high-reliability industries such as aerospace, automotive, energy equipment, and precision machinery, chemical composition should be verified as part of supplier qualification. Large importers in Germany, the United States, Mexico, Brazil, India, Thailand, Turkey, and the UAE often require initial samples, production part approval documents, and periodic third-party testing.
In real operations, chemistry is not judged alone. A shot with acceptable chemical composition but poor heat treatment can still fail. Similarly, a shot with good hardness but high crack percentage will generate dust and lose working efficiency. The best evaluation combines chemistry, hardness, microstructure, particle shape, density, and field life.
| Element | Technical Role | Typical Buyer Concern | Good Control Result | Poor Control VS Good Control |
|---|---|---|---|---|
| Carbon, C | Supports hardness and martensite formation | Too high may cause brittleness | Balanced hardness and durability | Poor control increases fracture risk |
| Silicon, Si | Deoxidation and strength support | Excess may affect toughness | Cleaner steel and stable performance | Poor control may reduce impact life |
| Manganese, Mn | Improves hardenability and toughness | Imbalance can affect structure | Better resistance to repeated impact | Good Mn balance improves recyclability |
| Chromium, Cr | May improve wear resistance | Needs consistency by grade | More stable hardness response | Unclear Cr content creates batch variation |
| Sulfur, S | Usually restricted impurity | High sulfur reduces toughness | Lower crack tendency | High S causes more dust and breakage |
| Phosphorus, P | Usually restricted impurity | High phosphorus increases brittleness | Improved impact reliability | High P shortens service life |
The table explains why chemical composition requirements should be written clearly in purchase orders. When a buyer simply orders “steel shot S110” without chemistry expectations, the supplier may ship material that is acceptable for low-cost cleaning but unsuitable for controlled peening or premium surface preparation.
Hardness Grades Explained: GP, GL, and GH Across the 40–68 HRC Range
Hardness grade is one of the most important selection factors for S110 steel shot. The common commercial categories are GP, GL, and GH. GP is often considered general-purpose shot and is usually selected for standard cleaning where long life and reduced equipment wear are desired. GL is harder and provides stronger cleaning action. GH is the hardest category and is used when high impact intensity or special peening effects are needed, but it may also increase machine wear and shot fracture if misapplied.
The broad hardness range of steel shot can extend from about 40 HRC to 68 HRC depending on grade, process, and standard. The right choice depends on substrate material, surface condition, target roughness, machine type, and whether the operation is cleaning or shot peening. For example, a foundry cleaning small castings may choose GP or GL for productivity and durability. A spring manufacturer may require harder shot for controlled compressive stress, but only after validating Almen intensity and coverage. A coating line cleaning thin sheet metal may prefer a softer or medium grade to avoid distortion.
Hardness should be measured by accepted methods and reported with a representative sample size. Because S110 particles are small, testing requires careful sample preparation and proper equipment. Buyers should avoid comparing supplier certificates unless the testing method is understood. A certificate showing an HRC range without method detail is less useful than a certificate with sample count, preparation method, and quality control limits.
Hardness also interacts with machine configuration. Wheel blast machines produce high media velocity and can amplify the effect of hard shot. Air blast systems offer more flexible pressure control but may require careful nozzle selection. In closed-loop peening systems, shot hardness, size, and flow rate must be controlled with separators and classifiers to maintain intensity.
| Grade | Approximate Hardness Range | Best Use | Main Advantage | GP VS GL VS GH |
|---|---|---|---|---|
| GP | About 40–51 HRC | General cleaning and light surface preparation | Good durability and lower equipment wear | Softer than GL and GH |
| GL | About 50–60 HRC | More demanding cleaning and moderate peening | Higher cleaning energy | Balanced middle option |
| GH | About 60–68 HRC | High-intensity applications and harder surfaces | Strong impact effect | Hardest but may wear equipment faster |
| Low hardness shot | Below normal grade target | Limited use | May reduce part damage | Often poor cleaning efficiency |
| Excessively hard shot | Above required range | Special cases only | High intensity | Can fracture and create dust |
| Controlled hardness mix | Within buyer specification | Automated production | Stable process output | Preferred over uncontrolled variation |
The comparison shows that no hardness grade is universally best. The correct grade is the one that achieves the required surface result with the lowest total operating cost and acceptable part safety. Buyers should request sample testing before switching from GP to GL or GH, especially in production lines serving automotive, aerospace, rail, shipbuilding, and energy customers.
S110 vs S170 vs S230: Size Comparison and Application Differences
S110, S170, and S230 are often compared because they are all relatively common steel shot sizes for industrial blasting and peening. The main difference is diameter, which directly affects impact energy, coverage rate, surface roughness, and ability to reach small features. S110 is finer and creates a smoother finish. S170 provides a stronger cleaning effect while still being suitable for moderately detailed parts. S230 is more aggressive and is often selected for heavier scale, larger castings, and stronger anchor profiles.
For a buyer operating in multiple markets, the choice may vary by product type. A plant in Detroit making automotive transmission components may prefer S110 for fine cleaning and peening of precision parts. A foundry near Monterrey may use S170 for general castings. A ship repair facility near Singapore or Busan may choose S230 or larger media for heavy corrosion removal on steel structures. In coating preparation, the final choice must match coating manufacturer requirements, surface cleanliness grade, and roughness profile.
Substitution should be approached carefully. Moving from S110 to S170 may improve cleaning speed but increase surface roughness. Moving from S230 to S110 may improve finish but reduce productivity on heavy scale. In shot peening, changing shot size can change Almen intensity, coverage behavior, and compressive stress distribution. Any substitution should be validated with test coupons, surface roughness measurement, coverage inspection, and fatigue testing when relevant.
Equipment design also matters. Media separators, screens, reclaim systems, and dust collectors must be suitable for the selected size. Fine shot such as S110 requires efficient separation to remove broken particles and maintain a healthy operating mix. Poor separation allows fines to accumulate, which reduces impact energy and increases dust. For global buyers, spare parts availability for separators and classifiers should be considered before scaling up S110 usage.
| Application | S110 Performance | S170 Performance | S230 Performance | Best Practical Choice |
|---|---|---|---|---|
| Small precision castings | Fine finish and low damage risk | Faster cleaning but rougher | May be too aggressive | S110 or S170 |
| Automotive gears | Good for fine peening areas | Useful for stronger intensity | Often too large for fine roots | S110 after validation |
| Heavy foundry scale | May clean too slowly | Moderate productivity | Strong cleaning power | S230 |
| Aluminum die castings | Gentle and uniform | Can be acceptable | Higher denting risk | S110 |
| Thin sheet components | Lower distortion risk | Higher impact | Possible deformation | S110 |
| General structural steel | Fine profile only | Medium profile | Better for stronger profile | S170 or S230 |
This table makes the practical differences clear. S110 is preferred where finish, precision, and controlled impact matter. S170 and S230 are preferred where cleaning productivity and stronger profile are more important. A professional supplier should help the buyer compare these options through samples and trial data rather than promoting only one size.
Microstructure Standards: Martensite, Hollow Particles, and Crack Limits
Microstructure determines whether S110 steel shot can survive repeated impact. High-quality shot is expected to have a sound structure, commonly martensitic or tempered martensitic, with controlled carbide distribution and limited defects. The structure should be strong enough to resist flattening but tough enough to avoid rapid fracture.
Hollow particles are a critical defect. They may form during atomization when gas is trapped inside molten droplets. A hollow particle can break quickly under impact, creating dust and fines. Excess hollow content reduces effective abrasive life and increases cleaning system contamination. Crack limits are equally important. Surface cracks, internal cracks, and severe irregularities can cause premature breakage. For fine shot like S110, crack control requires stable melting, atomization, heat treatment, screening, and inspection.
Particle shape should be predominantly spherical. Angular fragments act differently from shot: they cut rather than peen, increase roughness, and may damage surfaces. In operating mix, some broken particles are normal over time, but the incoming product should not contain excessive broken media. Buyers should request microstructure reports, metallographic photos, and defect limits when the application is critical.
In shot peening, microstructure quality becomes even more important because the process is used to improve fatigue life. If the shot breaks excessively, intensity becomes unstable and coverage may be inconsistent. Aerospace, automotive, wind power, and rail industries often require strict control of media condition during production, including regular checks for size, shape, and contamination.
SDBALLS’ technological capabilities are built on decades of precision sphere manufacturing knowledge. While the company is widely known for carbon steel balls, chrome steel balls, stainless steel balls, and multi-material sphere supply, the same attention to roundness, surface condition, metallurgical consistency, and batch control supports its ability to understand steel shot requirements. Buyers can learn more about the company’s quality systems through the technical quality resources available online.
Density, Recyclability, and Fatigue Life Performance Data
Density affects impact energy and blast efficiency. Cast steel shot typically has high density compared with mineral abrasives, which allows it to transfer significant kinetic energy at a given velocity. For S110, the small size reduces individual particle energy, but the large number of particles improves coverage. This makes it effective for uniform treatment of small or detailed surfaces.
Recyclability is one of the main economic advantages of steel shot. Unlike single-use abrasives such as some slags or sand-type media, steel shot can be reclaimed, cleaned, and reused many times in closed blast systems. The number of cycles depends on hardness, microstructure, machine velocity, workpiece hardness, separator efficiency, and maintenance practice. A premium shot with low defect content normally lasts longer and produces less dust.
Fatigue life performance is especially relevant in shot peening. The purpose of peening is not just to clean the surface; it is to introduce compressive residual stress that helps resist crack initiation and propagation. Springs, gears, shafts, connecting rods, aircraft components, and turbine-related parts may benefit from properly controlled shot peening. However, fatigue improvement depends on validated parameters: shot size, hardness, intensity, coverage, angle, velocity, and media condition.
Buyers should ask suppliers for practical performance data where available. This may include durability index, breakdown rate, dust generation comparison, operating mix recommendations, and case-based consumption data. Because machines and parts vary widely, the most reliable data comes from plant trials. A trial should measure media consumption per hour, cleaned area per kilogram, dust collector loading, surface roughness, and part acceptance rate.
| Performance Factor | High-Quality S110 | Low-Quality S110 | Operational Impact | Value Comparison |
|---|---|---|---|---|
| Density | Consistent and suitable for efficient impact | May vary due to hollows or defects | Affects cleaning power | Higher consistency improves process control |
| Breakdown rate | Low under correct use | High, with many fines | Changes operating mix quickly | Low breakdown reduces total cost |
| Dust generation | Lower | Higher | Affects visibility and filtration | Cleaner operation improves safety |
| Recyclability | Many reuse cycles | Short life | Increases replacement frequency | Long life beats low purchase price |
| Fatigue performance | Stable when peening parameters are controlled | Unstable intensity and coverage | May affect component life | Quality supports reliability |
| Machine wear | Predictable | Can increase due to broken particles | Raises maintenance cost | Stable shot protects equipment |
The performance comparison highlights a key buying principle: the cheapest S110 steel shot is not always the most economical. Global buyers should calculate cost by blasting result, maintenance burden, rework rate, and waste disposal rather than purchase price alone.
Surface Preparation and Shot Peening Application Guide
S110 steel shot is used in two broad application families: surface preparation and shot peening. Surface preparation includes cleaning, descaling, deburring, coating preparation, and cosmetic finishing. Shot peening is a controlled mechanical treatment designed to improve fatigue resistance. Although both use steel shot, the process goals and quality controls are different.
For surface preparation, the main questions are: What contaminant must be removed? What surface roughness is required? What base material is being treated? What production speed is needed? S110 performs well on light scale, small parts, aluminum die castings, precision steel components, stainless components where contamination rules allow steel media, and pre-treatment before painting or plating when a fine texture is needed. It may not be the best choice for thick rust, heavy mill scale, or large structural components requiring deep anchor profiles.
For shot peening, the buyer must control intensity and coverage. Almen strips are commonly used to verify intensity. Coverage is checked visually or by fluorescent tracer methods depending on the specification. S110 may be selected for low to moderate intensity peening or areas requiring fine access. In industries such as aerospace maintenance in Toulouse, Seattle, and Singapore, or automotive production in Stuttgart, Nagoya, Detroit, and Pune, peening parameters are often locked by engineering specifications and cannot be changed without approval.
Machine settings must be optimized. In wheel blasting, wheel speed, feed rate, media flow, and part rotation influence the result. In air blasting, nozzle distance, air pressure, angle, and media flow are important. In both systems, separator performance is essential for maintaining usable S110 size distribution. Dust collector maintenance is also important because fine particles and broken shot can affect operator safety and process consistency.
Common industries using S110 include automotive, bearing manufacturing, spring manufacturing, precision casting, aluminum die casting, metal injection molding, hardware, machinery, aerospace subcontracting, medical instrument tooling, and electronics-related metal parts. The fine size makes it useful where uniform coverage and low surface damage are required.
Case study one: An automotive component supplier in Central Europe changed from a larger shot to S110 for small gear-related parts. The original process cleaned quickly but produced excessive surface roughness near root areas. After testing S110 with controlled hardness, the plant achieved a smoother finish and reduced rework. Cleaning time increased slightly, but part acceptance improved.
Case study two: A die casting producer in Southeast Asia used S110 for aluminum housings exported through Singapore and Laem Chabang. Larger media caused visible dents on thin areas. S110 reduced impact marks and improved cosmetic consistency before coating. The buyer selected moisture-protected big-bag packaging to reduce storage problems during humid seasons.
Case study three: A spring manufacturer serving the North American market evaluated S110 GH for controlled peening of small spring components. The engineering team validated intensity and coverage before approval. The final process improved fatigue performance compared with unpeened parts, but only after the operating mix was monitored regularly.
Local supplier selection differs by region. In North America, buyers often value fast warehouse delivery from Chicago, Houston, Los Angeles, or Monterrey. In Europe, technical documentation and compliance are frequently prioritized by buyers in Germany, Italy, France, Poland, and the Netherlands. In the Middle East, supply reliability through Jebel Ali and Dammam is important for oil, gas, and infrastructure work. In Asia-Pacific, buyers in China, Japan, South Korea, Vietnam, Thailand, and India often compare factory-direct pricing, lead time, and technical support.
When comparing local distributors and overseas manufacturers, buyers should evaluate inventory, quality traceability, engineering support, export experience, payment terms, and claim handling. A distributor may provide urgent delivery, while a manufacturer or integrated supply partner can often provide better customization and long-term cost stability. The best model may combine both: local stock for emergencies and direct factory supply for planned production.
For additional examples of use cases across mechanical systems, bearings, automotive components, and outdoor equipment, buyers may review SDBALLS’ application information. This helps procurement teams connect abrasive and sphere-related sourcing with real industrial scenarios.
Our Company
SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., is a professional precision steel ball manufacturer and integrated supply partner headquartered in Tai’an City, Shandong Province, China. Since 1996, the company has developed manufacturing experience that supports global buyers in precision spheres, steel balls, and related steel media supply. Its customer base extends across more than 50 countries, including major industrial markets in North America, Europe, Asia-Pacific, the Middle East, and South America.
Manufacturing capabilities are a core strength. SDBALLS operates three production facilities with annual capacity exceeding 5,000 tons. The company manufactures carbon steel balls, chrome steel balls, and stainless steel balls in grades from G10 to G1000. This background is relevant to S110 steel shot buyers because precision sphere production requires disciplined control of material selection, heat treatment, sorting, surface condition, dimensional inspection, and batch traceability. Buyers who need stable steel media supply can explore available categories through the product center.
Service capabilities are designed for international procurement. SDBALLS works with customers who need factory-direct supply, multi-material sourcing, export documentation, flexible packaging, and coordinated shipments. In addition to steel balls, the company helps buyers source plastic, glass, ceramic, copper, and aluminum spheres, allowing procurement teams to consolidate supply through one reliable partner. This can be valuable for distributors, OEMs, maintenance companies, and industrial buyers managing multiple SKUs across different countries.
The company also serves outdoor and hunting-related markets with lead-free steel shot, including annealed and plated options that support hardness requirements for EU and US markets. This shows its ability to manage different steel shot requirements, from precision mechanical uses to application-specific performance needs. For industrial buyers evaluating S110 steel shot, this experience supports technical communication around hardness, surface finish, packaging, and compliance expectations.
Quality systems are important for global buyers. SDBALLS maintains certifications including IATF 16949, ISO 9001, and ISO 14001, reflecting attention to automotive quality management, general quality control, and environmental responsibility. Buyers seeking long-term cooperation can learn more through the company profile, which introduces the organization’s background and export service approach.
Buying advice from a supplier perspective is straightforward. First, define the application: cleaning, deburring, coating preparation, or shot peening. Second, confirm size and hardness grade. Third, request chemistry, hardness, sieve, and microstructure documents. Fourth, run a sample trial under real machine conditions. Fifth, calculate total cost by media consumption, dust, rework, and maintenance. Sixth, establish a repeatable specification in the purchase order. This process helps avoid misunderstandings and supports stable production in global supply chains.
The 2026 trend for S110 steel shot procurement will focus on smarter process control, sustainability, traceability, and regional supply resilience. More blast rooms and peening systems will use sensors to monitor media flow, dust levels, separator efficiency, and surface roughness. Automotive and aerospace buyers will continue tightening documentation requirements. Environmental policy will push companies toward recyclable abrasives, lower dust generation, and reduced waste. Trade policy and freight volatility will encourage buyers to qualify reliable suppliers before urgent demand arises. For global procurement teams, the winning strategy will be technical qualification plus flexible logistics.
Sustainability is especially relevant. Because steel shot is recyclable in closed systems, it can reduce abrasive waste compared with many disposable media. However, sustainability depends on quality. Shot that breaks quickly creates more dust and waste, while durable shot supports lower consumption. Buyers should include recyclability, packaging recovery, and environmental management systems in supplier evaluation, not just product price.
FAQ
What is S110 steel shot? S110 steel shot is a fine spherical steel abrasive with a nominal size of about 0.3 mm. It is used for light cleaning, finishing, deburring, and controlled shot peening where a fine and uniform impact is needed.
Is S110 the same as 0.3 mm steel shot? It is commonly described as approximately 0.3 mm nominal diameter, but the official purchase requirement should refer to size distribution and sieve limits rather than only one diameter number.
Which standard should buyers mention? SAE J444 is commonly used for size classification. Depending on the application, buyers may also refer to steel shot material standards, AMS peening standards, ISO requirements, or customer-specific specifications.
What is the difference between GP, GL, and GH? GP is general-purpose and softer, GL is medium-hard with stronger cleaning action, and GH is harder for demanding impact or peening applications. The total range may be around 40–68 HRC.
Is S110 better than S170 or S230? Not always. S110 is better for fine finish, delicate parts, and small features. S170 and S230 are better when stronger cleaning and higher surface profile are required.
Can S110 be used for shot peening? Yes, but only when the peening process is validated. Buyers must control Almen intensity, coverage, hardness, size distribution, and media condition.
What chemical elements should be checked? Carbon, silicon, manganese, chromium, sulfur, and phosphorus are commonly reviewed. Sulfur and phosphorus should be controlled because excessive levels can reduce toughness.
Why are hollow particles a problem? Hollow particles break more easily during blasting, creating dust and reducing abrasive life. Low hollow content is a sign of better manufacturing control.
How should S110 be packaged for export? Common options include 25 kg bags, big bags, drums, and palletized packaging. Moisture protection and batch labeling are important for ocean freight and warehouse storage.
How do I compare supplier quotations? Compare size certificate, hardness range, chemistry, microstructure, packaging, lead time, quality system, and expected consumption. Do not compare price per ton alone.
Which industries use S110 steel shot? Automotive, aerospace subcontracting, precision casting, aluminum die casting, spring manufacturing, bearing production, machinery, hardware, and coating preparation lines commonly use fine steel shot.
How can SDBALLS support global buyers? SDBALLS combines precision steel ball manufacturing experience, international service capability, quality certifications, and integrated sourcing support for buyers needing reliable steel media and sphere-related products.
About the Author
We are SD Ball, a professional manufacturer dedicated to delivering high-precision steel ball solutions worldwide. With years of expertise, we specialize in advanced production processes, strict quality control, and customized solutions to support diverse industrial applications. From material selection to final inspection, we provide reliable products and consistent performance to help our clients achieve higher efficiency, durability, and product quality.
Share
Product Category
Related Articles
-
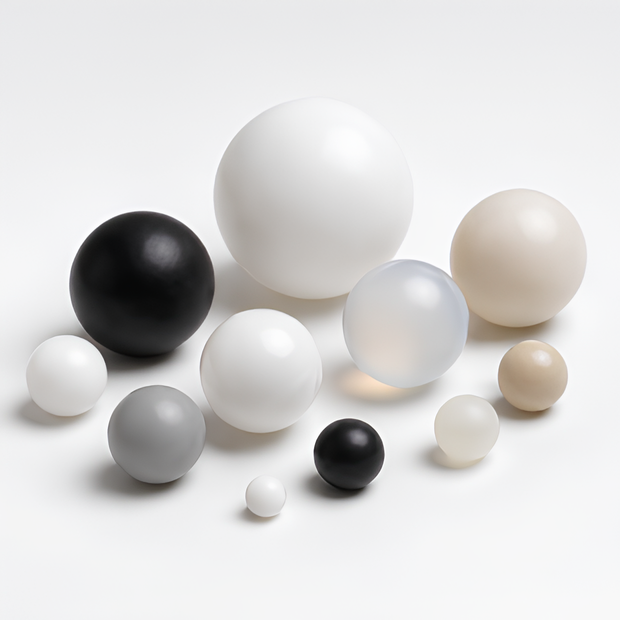
Global Market Guide to 10mm POM Acetal Ball Specs 2026
A 10mm POM acetal plastic ball is a precision-engineered polymer sphere used where low friction, dimensional stability, chemical resistance, and moderate mechanical strength are required. For buyers in the Global Market, the most important specifications are material type, nominal diameter, grade tolerance, surface finish, hardness, moisture absorption, operating temperature, and application environment. POM is also known as acetal, polyacetal, or polyoxymethylene. It is available mainly as POM-H homopolymer and POM-C copolymer, each offering different performance advantages.For most industrial applications, POM-C is selected because it offers excellent chemical resistance, better thermal stability, lower centerline porosity risk, and reliable performance in humid or chemically exposed environments. POM-H is chosen when higher stiffness, slightly higher tensile strength, and better fatigue resistance are more important than chemical resistance. In a 10mm diameter plastic ball, these differences can affect roundness retention, wear behavior, long-term dimensional accuracy, and suitability for bearings, valves, gears, flow meters, medical devices, food equipment, and precision mechanical assemblies.The commonly discussed precision grades for 10mm POM balls include G0, G1, G2, and G3 in many supplier-specific plastic ball systems. Unlike steel ball grades such as G10 or G100, plastic ball grades are often defined by manufacturer tolerance standards rather than a single universal global code. Therefore, buyers should always confirm the exact diameter tolerance, sphericity, surface roughness, lot consistency, and inspection method before ordering. For critical components supplied to manufacturers in Detroit, Stuttgart, Shenzhen, Singapore, Dubai, Rotterdam, Los Angeles, and São Paulo, a written specification sheet is more reliable than relying on grade names alone.In simple terms, choose POM acetal balls when you need a hard, lightweight, low-friction plastic sphere with better dimensional stability than nylon and lower cost than PTFE. Choose nylon when impact toughness and lower price matter more than moisture stability. Choose PTFE when extreme chemical resistance and very low friction are more important than strength and stiffness. Choose stainless steel or chrome steel when high load, high hardness, and very tight precision are required.Buyer QuestionQuick AnswerBest PracticeVS ConsiderationIs POM suitable for 10mm precision balls?Yes, it is widely used for low-friction precision plastic balls.Specify grade, tolerance, and surface quality.POM vs nylon: POM absorbs less moisture.Should I choose POM-H or POM-C?POM-C is more versatile; POM-H is stiffer.Match material to chemical, load, and temperature conditions.POM-H vs POM-C: strength versus chemical stability.What grade is best for bearings?Higher precision grades are preferred for smooth rotation.Confirm sphericity and surface finish.Plastic ball grades differ from steel ball grades.Can POM replace metal balls?Yes in light-load, quiet, corrosion-sensitive systems.Check load, speed, temperature, and wear rate.POM vs steel: lower weight but lower load capacity.Is POM food-contact suitable?Some grades may be suitable if certified.Request FDA, EU, or other compliance documents.POM vs PTFE: PTFE has broader chemical inertness.What is the main purchasing risk?Unclear tolerance definitions and inconsistent material grade.Use drawings, inspection reports, and sample approval.Certified supply vs commodity trading.This guide explains the specifications, differences, testing points, application logic, and sourcing advice for 10mm POM acetal plastic balls for the Global Market. It also places POM balls in context with nylon, PTFE, steel, ceramic, and other sphere materials so that procurement teams, engineers, and distributors can select the correct ball for performance and cost.POM-H, or acetal homopolymer, is produced from formaldehyde polymerization and is known for high crystallinity, excellent stiffness, good fatigue resistance, and strong mechanical performance. POM-C, or acetal copolymer, is produced with comonomers that improve thermal stability and resistance to alkaline chemicals and hot water. Both are engineering plastics with good machinability and excellent sliding characteristics, but their internal structure and long-term behavior are different.For 10mm acetal balls, POM-H can be useful in small mechanical parts requiring stiffness and low creep under repeated motion. It may perform well in precision guides, light-duty bearings, actuator parts, and moving assemblies where chemical exposure is limited. However, POM-H can be more sensitive to strong alkalis and some hydrolysis conditions. It may also have higher risk of centerline porosity in larger extruded stock, although molded ball production and supplier control can reduce this concern.POM-C is usually the safer choice for global industrial buyers because it balances strength, dimensional stability, chemical resistance, and process consistency. It is commonly used in pump components, valves, conveyor parts, food equipment, packaging machinery, and fluid control systems. In humid areas such as Singapore, Ho Chi Minh City, Rotterdam, Hamburg, Houston, and Santos, POM-C’s lower risk in water-contact applications is an important advantage over many nylon materials.When selecting between the two, buyers should avoid asking only for “POM balls” without further clarification. A professional specification should state whether POM-H or POM-C is required, whether natural white, black, colored, antistatic, conductive, medical, food-grade, or modified material is needed, and whether the balls must comply with RoHS, REACH, FDA, EU food contact, or customer-specific standards. For international trade, especially through ports such as Qingdao, Shanghai, Ningbo, Busan, Long Beach, Jebel Ali, Antwerp, and Rotterdam, clear documentation reduces customs, inspection, and quality disputes.Specification FactorPOM-H HomopolymerPOM-C CopolymerPractical Buying NoteMechanical stiffnessGenerally higherSlightly lower but still strongChoose POM-H for stiffness-sensitive designs.Chemical resistanceGood, but weaker against alkalisBetter overall chemical stabilityChoose POM-C for valves and fluid systems.Moisture behaviorLow moisture absorptionLow moisture absorptionBoth outperform nylon in dimensional stability.Thermal stabilityGood in normal useOften better in long-term hot-water exposurePOM-C is safer for humid global markets.Wear resistanceExcellentExcellentBoth suit low-friction sliding applications.Cost and availabilityMay vary by regionWidely availablePOM-C is often easier for stable supply.Application preferencePrecision mechanical motionPumps, valves, food and industrial partsConfirm by operating environment, not only price.The table shows that the material decision is not a question of better or worse in all cases. It is a question of matching performance to application. A 10mm POM-H ball in a dry mechanical guide may outperform a POM-C ball in stiffness. A 10mm POM-C ball in a pump valve exposed to water and cleaning agents may deliver more reliable life. For OEM buyers, it is useful to run comparative sample testing under real operating conditions before freezing the bill of materials.Diameter tolerance is one of the most important specifications for a 10mm POM acetal ball. A nominal 10mm ball is rarely exactly 10.000mm in every measurement direction. The actual specification may include diameter variation, lot diameter variation, spherical error, surface quality, gate mark control, and visual defects. For plastic balls, terms such as G0, G1, G2, and G3 may be used by suppliers to describe relative precision levels, but the numerical meaning can vary by factory.In practical sourcing, G0 often represents a high precision or custom precision level, while G1, G2, and G3 represent progressively broader tolerance classes. However, a buyer should not assume that a G1 plastic ball equals a steel ball G10 or any specific international ball standard. Instead, the purchase drawing should define acceptable minimum and maximum diameter, roundness, surface scratches, color consistency, flash, burrs, parting line, and packaging requirements.A 10mm POM ball used in a flow control valve may allow a wider tolerance than one used in a miniature bearing or measuring device. A ball used in a detent mechanism may need excellent surface finish and consistent hardness but may not require the tightest diameter tolerance. A ball used in an indexing system may need repeatable diameter more than cosmetic appearance. These distinctions matter because over-specifying precision can increase cost, while under-specifying it can cause assembly failure.Precision LevelTypical Use ConceptDiameter ControlSurface ExpectationVS Lower GradeG0Special high-precision plastic ball applicationsVery tight, supplier-definedExcellent finish, strict inspectionHigher cost, better consistency than G1-G3.G1Precision mechanical assembliesTightGood cosmetic and functional qualityBetter assembly fit than G2 and G3.G2General industrial precision useModerateFunctional surface qualityLower cost than G1, more stable than commodity grade.G3Non-critical motion, valves, general componentsStandard commercial toleranceAcceptable for many industrial usesMore economical but less precise than G0-G2.Commodity gradeToys, fillers, non-precision partsBroadMay include visible variationNot recommended for controlled engineering systems.Custom gradeOEM-specific designDefined by drawingDefined by inspection planBest for long-term contracts and critical systems.The most reliable way to buy 10mm POM balls is to request a supplier inspection report. This report may include measured sample diameters, material certificate, visual inspection result, and quantity verification. For high-volume programs serving automotive, medical, consumer equipment, or fluid control markets, buyers may also request PPAP-style documentation, capability studies, traceability, and batch samples. Although these controls are more common in metal ball manufacturing, they are increasingly expected in engineering plastic ball procurement as global supply chains become more quality-driven.Ports and trade hubs influence tolerance control indirectly. Products shipped from factories near Qingdao, Shanghai, Ningbo, Guangzhou, Kaohsiung, Busan, or Osaka may experience long transit to North America, Europe, the Middle East, or South America. POM has good dimensional stability, but packaging should still protect balls from deformation, contamination, and extreme heat. Precision balls should not be loosely packed in oversized cartons where vibration and compression can damage surface quality.The mechanical performance of 10mm POM balls depends on the resin grade, processing method, additives, conditioning, and testing standards. Typical POM has a Shore D hardness around the high 70s to mid 80s, tensile strength commonly in the range of about 60 to 75 MPa, and flexural modulus around 2.4 to 3.2 GPa. These values are general reference ranges, not guaranteed values for every product. For purchasing, the supplier’s datasheet and batch certificate should be used.Hardness affects resistance to indentation, wear, and deformation. A 10mm POM ball is harder than many nylon balls and much harder than many rubber or elastomer balls, but it is much softer than steel, ceramic, or glass. Tensile strength is important for understanding material integrity, but in a ball application, compressive behavior, creep resistance, impact strength, and wear performance may be more directly relevant. Flexural modulus indicates stiffness, which affects deformation under load and ability to maintain geometry.POM performs well in applications where the ball experiences rolling, sliding, intermittent load, and moderate contact stress. It is not designed for high-temperature, high-load, or abrasive environments where steel, ceramic, or special high-performance polymers such as PEEK may be required. In bearing applications, load rating should be carefully calculated because polymer balls deform more than metal balls. In valve applications, the sealing seat material and pressure differential determine whether POM is suitable.For a 10mm ball, weight is also important. POM density is typically around 1.41 g/cm³, far lower than steel at about 7.85 g/cm³. This lower mass reduces inertia, noise, and corrosion risk. It also improves suitability for float-related mechanisms where density matters, although POM is denser than water and will not float in pure water unless combined with a special design.PropertyTypical POM RangeEngineering MeaningPOM vs AlternativeShore D hardnessApproximately 78-85Good resistance to surface indentationHarder than many nylons, softer than steel.Tensile strengthApproximately 60-75 MPaStrong engineering plastic performanceHigher than PTFE, lower than metals.Flexural modulusApproximately 2.4-3.2 GPaGood stiffness for plastic componentsMore stable than nylon in humid conditions.DensityApproximately 1.41 g/cm³Lightweight compared with metalAbout one-fifth the weight of steel.Moisture absorptionLowGood dimensional stabilityMuch lower than nylon.Operating temperatureCommonly around -40°C to 100°C short-term depending on gradeSuitable for many industrial environmentsLower than PTFE and PEEK.Friction behaviorLowSupports sliding and rolling motionLower friction than many common plastics.The table highlights why POM is often called a balanced engineering plastic. It is not the strongest, cheapest, most chemically inert, or most heat-resistant polymer. Its value lies in a practical combination of strength, stiffness, low friction, machinability, and dimensional stability. For buyers, this balance is especially attractive when a ball must be cleaner and quieter than metal but stronger and more accurate than many low-cost plastics.One of the main reasons engineers choose POM acetal balls is low friction. POM has naturally good sliding behavior against metals, plastics, and some elastomers. In many light-duty assemblies, a 10mm POM ball can operate without external lubrication, reducing maintenance, contamination, and noise. This self-lubricating characteristic is valuable in office equipment, packaging machinery, conveyor components, small bearings, guide tracks, valve seats, and consumer product mechanisms.The phrase “self-lubricating” should be understood correctly. It does not mean the ball produces oil or can operate in every dry condition without wear. It means the polymer surface has a relatively low coefficient of friction and can slide with reduced resistance compared with many other plastics. Wear still depends on load, speed, temperature, counterface roughness, dust, chemical exposure, and alignment. A polished stainless steel seat may deliver excellent life, while a rough abrasive metal track may accelerate wear.Friction performance is often application-specific. POM sliding against stainless steel may behave differently from POM sliding against aluminum, brass, rubber, nylon, or another POM part. Additives such as PTFE, silicone, glass fiber, carbon, or lubricants can change friction and wear, but modified materials may also affect food contact compliance, color, strength, and cost. For 10mm balls, unfilled natural or black POM is common, while modified grades are used for special applications.In manufacturing hubs such as Suzhou, Dongguan, Pune, Monterrey, Milan, Chicago, and Istanbul, engineers often choose POM balls to reduce noise in moving systems. Compared with steel balls, POM balls produce softer contact sound and lower vibration transmission. This matters in medical devices, home appliances, furniture hardware, display stands, vending machines, and lightweight automation modules. In automated warehouses near Los Angeles, Hamburg, Dubai, and Singapore, quiet and corrosion-resistant components can improve equipment reliability.For buying decisions, friction data from a datasheet should be treated as a starting point rather than a final answer. Coefficient of friction is measured under specific laboratory conditions. A real assembly may have dust, misalignment, impact load, cleaning agents, and temperature cycles. Therefore, sample testing is recommended before large-volume procurement. Suppliers with experience in multiple sphere materials can help compare acetal, nylon, PTFE, stainless steel, ceramic, glass, and copper balls based on operating conditions.Dimensional stability is a major advantage of POM over nylon. Nylon absorbs moisture from air and water, which can cause swelling, changes in mechanical properties, and variation in diameter. POM absorbs much less moisture, making it more reliable in environments where humidity changes from dry warehouse storage to humid factory floors or marine shipping routes. For 10mm balls, even small dimensional changes can affect valve sealing, bearing clearance, detent force, or indexing accuracy.Global buyers often manage inventory across different climates. A distributor may store POM balls in Houston, Rotterdam, Singapore, Dubai, Mumbai, or São Paulo before supplying local manufacturers. The balls may travel by ocean freight through humid conditions and then enter controlled assembly plants. POM’s low moisture absorption helps maintain more consistent size and mechanical behavior during this journey. This is one reason POM is favored for precision plastic balls in international supply chains.Temperature stability is also important. POM has good dimensional stability within its recommended operating range, but it still expands more than metal. Designers must account for thermal expansion when pairing POM balls with metal housings, seats, or races. A valve designed in a cold European environment may behave differently when used in the Middle East or Southeast Asia. Clearance, sealing force, and contact stress should be calculated with thermal expansion in mind.Creep is another consideration. Under sustained load, plastic materials deform over time. POM has good creep resistance among common engineering plastics, but it is not immune. A 10mm POM ball held under constant high compression in a valve seat, clamp, or fixture may gradually deform, especially at elevated temperature. For critical sealing or load-bearing applications, designers should test long-term compression behavior and compare it with PTFE, nylon, PEEK, stainless steel, or ceramic alternatives.Packaging supports dimensional stability. Precision POM balls should be packed to avoid heavy compression, contamination, and high-temperature exposure. Bulk bags may be acceptable for general-grade parts, but precision grades should use inner bags, reinforced cartons, batch labels, and moisture-protective packaging when needed. For long sea routes from Qingdao or Shanghai to Long Beach, Hamburg, Antwerp, or Jebel Ali, stable packaging reduces transport-related quality issues.POM, nylon, and PTFE are three common engineering plastic ball materials, but they serve different needs. POM offers a balanced combination of strength, stiffness, low friction, dimensional stability, and moderate chemical resistance. Nylon offers toughness, impact resistance, and cost advantages, but it absorbs more moisture and may change size in humid conditions. PTFE offers outstanding chemical resistance and extremely low friction, but it has lower mechanical strength, higher creep, and higher cost.For a 10mm ball in a mechanical guide, POM is often preferred because it maintains size better than nylon and is stronger than PTFE. For a 10mm ball in a highly corrosive chemical valve, PTFE may be the better choice if mechanical load is moderate. For a 10mm ball in a low-cost consumer mechanism where moisture tolerance is not critical, nylon may be adequate. The correct decision depends on actual service conditions rather than general material popularity.Compared with steel balls, POM balls are lighter, quieter, corrosion-resistant, and non-magnetic. Compared with ceramic balls, POM balls are less brittle, lower cost, and easier to use in plastic assemblies, but they cannot match ceramic hardness or high-temperature resistance. Compared with glass balls, POM balls are tougher and less fragile, but glass offers excellent chemical inertness and optical appearance. For multi-material procurement, buyers should evaluate performance, cost, and supply reliability together.MaterialMain AdvantageMain LimitationBest Application FitVS POMPOM acetalBalanced strength, stiffness, low friction, low moisture absorptionLimited high-temperature and strong acid resistanceBearings, valves, gears, precision mechanismsBaseline balanced choice.NylonTough, economical, impact-resistantHigher moisture absorption and dimensional changeGeneral rollers, low-cost parts, impact componentsCheaper but less dimensionally stable.PTFEExcellent chemical resistance and very low frictionLower strength, higher creep, higher costChemical valves, lab equipment, corrosive environmentsMore inert but weaker and more expensive.PEEKHigh temperature and high performanceVery high costAerospace, medical, high-end industrial systemsStronger at heat but far more expensive.Stainless steelHigh strength, hardness, corrosion resistanceHeavy and may be noisyBearings, precision machinery, pumpsHigher load capacity but not lightweight.CeramicExtreme hardness, heat resistance, chemical stabilityBrittleness and costHigh-speed bearings, chemical systemsHarder and hotter-running, but less impact tolerant.GlassChemical resistance and smooth surfaceFragilityLab, cosmetic, decorative, light valvesMore inert visually, less tough mechanically.This comparison shows why POM is often specified as the “practical engineering choice.” It does not dominate every category, but it performs well enough in many categories to reduce design risk and cost. In procurement, a balanced material often wins because it simplifies inventory and supports multiple product lines. For example, a distributor serving manufacturers in Europe, North America, Southeast Asia, and the Middle East may stock 10mm POM balls as a standard item while sourcing PTFE, nylon, glass, ceramic, or metal balls for special projects.10mm POM acetal balls are used in many industries because they combine controlled geometry with engineering plastic performance. In light-duty bearings, POM balls can reduce noise, weight, and corrosion risk. They are suitable for low-load rolling elements, drawer slides, furniture hardware, display systems, packaging equipment, and consumer devices. However, they should not be used as direct replacements for steel bearing balls in high-load or high-speed applications without engineering validation.In gear and indexing systems, POM balls can act as detent balls, positioning elements, or low-friction contacts. Their low noise and smooth feel are useful in knobs, selectors, adjustable arms, latches, and mechanical control devices. A 10mm ball provides a tactile response that can be tuned with spring force and seat geometry. Compared with steel, POM offers a softer engagement and less surface damage to mating plastic or aluminum parts.In valve applications, POM balls may be used as check balls, sealing elements, flow control parts, or floating components in water, fuel, air, and compatible chemical systems. POM-C is often preferred for these applications because of its chemical and hydrolysis stability. The seat design is critical. A well-designed elastomer or plastic seat can seal effectively with a POM ball, while a poorly aligned hard seat may leak or wear quickly. Pressure, temperature, fluid type, and cleaning method must be confirmed.In precision components, 10mm POM balls are used in measuring devices, positioning fixtures, laboratory equipment, medical mechanisms, electrical insulation systems, and automation modules. Their non-magnetic behavior can be useful where steel would interfere with sensors or magnetic fields. Their electrical insulation may also be beneficial in some assemblies. Black POM balls are sometimes selected for optical detection or appearance, while natural white balls are common for food and medical-looking equipment.Real-world case studies demonstrate the selection logic. A packaging machinery manufacturer in Milan replaced metal balls with POM balls in a light indexing unit to reduce noise and eliminate surface corrosion from cleaning spray. A valve distributor in Dubai selected POM-C check balls for water-handling components because nylon swelling caused inconsistent sealing. An automation integrator in Shenzhen used 10mm POM balls in a low-load transfer device to reduce weight and protect aluminum tracks. A North American equipment builder near Chicago evaluated PTFE and POM, then chose POM because the application required better stiffness and lower deformation under spring load.Buying advice for these applications is straightforward. First, define the function of the ball: rolling, sealing, locating, floating, sliding, or spacing. Second, define the environment: dry, humid, submerged, chemical, food contact, outdoor, high temperature, or abrasive. Third, define the tolerance and inspection level. Fourth, request samples and test them in real assemblies. Fifth, choose a supplier that can support long-term consistency rather than only one-time low price.As 2026 approaches, several trends are shaping the Global Market for engineering plastic balls. Manufacturers are asking for better traceability, lower-carbon materials, recyclable packaging, PFAS-related compliance awareness, and digital inspection records. Sustainability policies in the European Union, North America, and parts of Asia are pushing buyers to document material origin, hazardous substance compliance, and waste reduction. At the same time, automation, robotics, electric mobility, medical devices, and smart logistics are increasing demand for lightweight, quiet, corrosion-resistant precision components. POM balls fit many of these trends when specified responsibly and supplied with transparent documentation.SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., supports global buyers with precision sphere manufacturing and integrated sourcing. Headquartered in Tai'an City, Shandong Province, China, the company has more than 30 years of manufacturing experience since 1996 and serves customers in more than 50 countries. While SDBALLS is best known as a professional precision steel ball manufacturer, it also helps customers consolidate procurement of multi-material spheres, including plastic, glass, ceramic, copper, and aluminum balls.From a technological capability perspective, SDBALLS understands precision ball requirements across multiple materials and applications. Its quality systems and technical experience in grades, inspection, hardness control, surface finish, and application matching help buyers communicate specifications clearly. For plastic balls such as 10mm POM acetal balls, this experience is valuable because tolerance definitions and material grade descriptions can vary by supplier. A buyer can use SDBALLS as a technical communication partner to compare POM-H, POM-C, nylon, PTFE, stainless steel, ceramic, and other materials according to function and working environment. More information about technical and quality control support is available through the company’s quality and technical resources.From a manufacturing capability perspective, SDBALLS operates three production facilities with annual capacity exceeding 5,000 tons. Its core production includes carbon steel balls, chrome steel balls, and stainless steel balls in grades ranging from G10 to G1000. This manufacturing base gives the company a strong understanding of precision, inspection discipline, packaging control, and batch consistency. For customers who need both metal balls and engineering plastic balls, this background helps unify sourcing standards. Buyers can review the broader sphere and ball product range through the product center.From a service capability perspective, SDBALLS works as an integrated supply partner for global procurement teams. Many buyers do not need only one material. A bearing manufacturer may require chrome steel balls, stainless steel balls, and POM balls. A valve supplier may need POM-C, PTFE, stainless steel, and ceramic balls. A hardware distributor may need steel, plastic, glass, and aluminum balls in different sizes. Consolidating these requirements through a reliable partner can reduce supplier management time, improve communication, and simplify export documentation. Company background and global service details can be found on the SDBALLS company overview.SDBALLS products and sourcing solutions serve mechanical systems such as caster wheels, sliding systems, ball transfer units, bearings, automotive components, outdoor equipment, valves, and general industrial assemblies. For application planning, buyers can explore the company’s industrial application guidance. The company’s certifications, including IATF 16949, ISO 9001, and ISO 14001, support consistent production management and environmental responsibility. For the Global Market, this combination of manufacturing foundation and flexible sourcing is useful for buyers who need reliable supply from China to North America, Europe, Southeast Asia, the Middle East, South America, and other regions.Local supplier selection should consider both availability and technical support. In major trade hubs such as Rotterdam, Hamburg, Antwerp, Los Angeles, Chicago, Houston, Dubai, Singapore, Mumbai, Istanbul, and São Paulo, distributors may stock standard plastic balls, but custom tolerances and material documentation often require factory-level coordination. Working with a manufacturer or integrated supply partner can improve traceability and reduce the risk of substituting POM-C with unspecified acetal, nylon, or recycled plastic. For OEM programs, a supplier should be able to provide drawings, specifications, sample approval, batch labels, inspection reports, and packaging plans.What is a 10mm POM acetal ball? It is a spherical engineering plastic component made from polyoxymethylene, also called acetal or polyacetal. The nominal diameter is 10mm, and it is used for low-friction, lightweight, corrosion-resistant mechanical functions.Is POM-H better than POM-C? Not always. POM-H usually offers higher stiffness and strength, while POM-C generally offers better chemical resistance and thermal stability. POM-C is often the safer general-purpose choice for valves, water contact, and humid environments.What does G0-G3 mean for plastic balls? These grades usually refer to supplier-defined precision levels for diameter, roundness, and surface quality. Buyers should request actual tolerance values because plastic ball grade systems are not always identical between manufacturers.Can 10mm POM balls be used in bearings? Yes, in light-duty or special bearings where low noise, corrosion resistance, and low weight are important. They are not direct replacements for steel balls in high-load or high-speed bearings unless the design is validated.Are POM balls food safe? Some POM materials may meet food-contact requirements, but compliance depends on the exact resin and additives. Buyers should request FDA, EU, or other relevant certificates when food equipment is involved.How does POM compare with nylon? POM has much lower moisture absorption and better dimensional stability. Nylon can be tougher and lower cost, but it may swell in humid or wet conditions, which can affect a 10mm precision ball’s performance.How does POM compare with PTFE? PTFE has better chemical resistance and lower friction, but it is softer, weaker, more expensive, and more prone to creep. POM is usually better when stiffness and mechanical strength are required.What color is standard for POM balls? Natural white and black are common. Other colors may be available depending on resin, quantity, and application requirements. Color additives should be checked if food, medical, or optical use is involved.What information should I include in an inquiry? Include material type, diameter, tolerance, quantity, color, application, working temperature, chemical exposure, certification needs, packaging preference, and destination country or port.Can POM balls be used in water? Yes, POM has low water absorption compared with nylon. For long-term hot water, chemical water, or cleaning-agent exposure, POM-C is often preferred, but testing is still recommended.What are common reasons for failure? Common causes include excessive load, wrong material selection, chemical attack, high temperature, abrasive counterfaces, poor seat design, unclear tolerance, or inconsistent supplier quality.How should 10mm POM balls be stored? Store them in clean, dry packaging away from high heat, direct sunlight, heavy compression, and contamination. Precision grades should remain in labeled batch packaging until assembly.What are the 2026 purchasing trends? Buyers are focusing on traceability, sustainability, compliance with chemical regulations, digital inspection data, recyclable packaging, and supply chain resilience. Engineering plastic balls with clear documentation will be preferred.Can one supplier provide POM, steel, ceramic, and glass balls together? Yes, an integrated sphere supply partner can help consolidate multiple materials, reduce procurement complexity, and improve specification control across different product categories.What is the best way to confirm quality before bulk orders? Request samples, verify dimensions, test in the real assembly, review material documents, approve packaging, and define inspection criteria in writing before mass production or shipment.For the Global Market, the best 10mm POM acetal plastic ball is not simply the cheapest or the tightest tolerance product. It is the ball that matches the material grade, diameter tolerance, surface finish, mechanical behavior, compliance requirements, and supply reliability required by the application. By comparing POM-H and POM-C carefully, defining G0-G3 tolerance expectations clearly, and testing real operating conditions, buyers can reduce risk and build a stable sourcing program for bearings, gears, valves, and precision components. -
Global Market Guide to TSS #9 Tungsten Shot Loads 2026
TSS #9 shot is a high-density tungsten super shot option widely used in premium turkey hunting and specialized small-bore shotshell applications. In practical terms, it offers a rare combination: very small pellet diameter, very high pellet count, and downrange penetration that can rival much larger lead pellets. For the Global Market, this makes TSS #9 especially important in 12 gauge, 20 gauge, 28 gauge, and .410 bore loads where hunters, ammunition brands, and component buyers want dense patterns without excessive recoil.The most common commercial TSS material is a tungsten alloy with density around 18 g/cc, far above lead at about 11.34 g/cc and steel at about 7.8 g/cc. A #9 TSS pellet is typically about 0.080 inch in diameter, and one ounce contains approximately 362 pellets. Because each pellet is extremely dense for its size, it retains energy better than its small diameter suggests. Many field comparisons treat TSS #9 as broadly comparable to lead #5 in practical turkey-load penetration at suitable distances, while providing far more pellets in the pattern.For buyers, the key decision is not simply “TSS or lead.” It is whether the extra cost of tungsten super shot is justified by the pattern density, range consistency, lighter-gauge possibilities, and environmental or regulatory considerations. In regions such as the United States, Canada, the European Union, Australia, New Zealand, Japan, South Korea, and emerging outdoor markets in Latin America and Southeast Asia, TSS demand is shaped by turkey hunting culture, non-toxic shot policy, supply chain cost, and the rise of small-bore premium loads.ItemTSS #9Lead #5Steel #7Buyer meaningApproximate density18 g/cc11.34 g/cc7.8 g/ccTSS keeps more energy in a smaller pelletTypical pellet diameter0.080 inch0.120 inch0.100 inchTSS #9 is much smaller but heavier than expectedPellets per ounceAbout 362About 170About 420TSS balances pellet count and penetrationPattern characterVery denseModerateDense but lower energyTSS supports compact gauges and tighter patternsTypical usePremium turkey and specialty loadsTraditional turkey loads where legalWaterfowl and non-toxic field loadsApplication determines valueMain limitationHigh costEnvironmental restrictionsLower densitySourcing and regulation drive selectionThis comparison shows why TSS #9 has become a premium option rather than a direct commodity replacement. It is technically superior in density and pattern potential, but it requires careful sourcing, quality control, and responsible use within local hunting regulations.TSS stands for tungsten super shot, a dense tungsten-based alloy shot designed for superior ballistic performance in small spherical pellets. While exact formulas vary by producer, commercial TSS commonly contains more than 95% tungsten by weight, blended with other metals such as nickel, iron, or copper to produce a hard, spherical, and high-density pellet. The target density is often advertised around 18 g/cc, although buyers should confirm actual density through supplier documentation and inspection.The difference between tungsten alloy shot and conventional lead shot is substantial. Lead has been used for generations because it is dense, soft, and easy to form. However, it deforms during acceleration and impact, and its use is restricted in many wetlands and certain hunting zones. TSS, by contrast, is significantly harder and denser. Its hardness helps pellets remain round, reducing flyers and supporting more even patterns. Its density gives smaller pellets enough momentum to penetrate effectively at longer distances than their size would normally imply.From a procurement perspective, composition matters because small variations affect cost, performance, and compliance. A buyer sourcing TSS for the Global Market should ask for material certificates, density range, size tolerance, sphericity standards, surface finish, and batch traceability. For ammunition manufacturers selling into North America or Europe, reliable documentation can reduce disputes and support brand claims. For distributors near trade hubs such as Los Angeles, Houston, Rotterdam, Hamburg, Antwerp, Singapore, Busan, Shanghai, and Dubai, consistent lot quality helps maintain trust across seasonal hunting demand.Material factorPremium TSS expectationLower-grade riskInspection methodCommercial impactTungsten contentUsually 95%+Reduced densitySupplier certificate or lab testAffects advertised performanceDensityNear 18 g/ccLower retained energyMass and volume verificationInfluences load positioningSphericityConsistent round pelletsPattern inconsistencyOptical inspectionImproves customer satisfactionHardnessHigh and stableBarrel or choke concerns if unmanagedHardness testingRequires proper wad and load designSurface conditionSmooth, clean finishFeeding or loading variationVisual and microscopy checksSupports automated loadingBatch traceabilityLot-level recordsDifficult complaint handlingQC documentationEssential for export supply chainsThe table highlights that TSS value is not only about tungsten percentage. A premium pellet must be dense, round, clean, and consistent from lot to lot. This is especially important for buyers serving premium hunting brands, where end users expect repeatable patterns after paying a high price per shell.TSS #9 is popular because it turns a single ounce of payload into a very large number of effective pellets. A typical #9 pellet measures about 0.080 inch in diameter. At approximately 18 g/cc density, one ounce contains about 362 pellets. This pellet count is a major advantage for turkey hunting because ethical field performance depends on both penetration and pattern density in the vital head and neck area.Lead #5 shot, by comparison, has much larger pellets and far fewer pellets per ounce. Traditional hunters often valued larger lead pellets for penetration, but the lower pellet count created a trade-off: more individual pellet energy but fewer strikes in the pattern. TSS #9 changes that equation by using high density to preserve penetration while greatly increasing the number of pellets. The result is a dense pattern that can be especially useful in smaller gauges and carefully tested turkey loads.For manufacturers and buyers, pellet count also affects packaging economics. A 1 5/8 oz load of TSS #9 contains far more projectiles than a comparable lead load. This gives marketers a strong performance story, but it also increases the importance of accurate shot metering, uniform pellet size, and careful shell assembly. Any variation in pellet diameter or density can change pellet count and pattern behavior.Shot typeApproximate sizePellets per ouncePattern densityPenetration outlookTSS #90.080 inchAbout 362Very highStrong for its sizeTSS #80.090 inchAbout 254HighHigher individual pellet energyTSS #70.100 inchAbout 185Moderate to highVery strongLead #50.120 inchAbout 170ModerateTraditional turkey standardLead #60.110 inchAbout 225GoodModerateSteel #70.100 inchAbout 420HighLower due to densityThis table shows the unique position of TSS #9. It does not have the highest pellet count of all shot types, but it combines a high count with exceptional density. That is why it is often selected for premium turkey loads instead of ordinary steel or traditional lead.The common claim that TSS #9 performs like lead #5 should be understood carefully. It does not mean the two pellets are identical in size or mass. Instead, it means that the higher density of TSS allows a much smaller pellet to deliver penetration comparable to a larger lead pellet under appropriate conditions. This is particularly relevant in turkey hunting, where multiple pellet strikes in a small vital zone are more important than a single heavy impact.Penetration depends on pellet diameter, density, velocity, pellet shape, retained energy, distance, target medium, and pattern quality. TSS #9 starts smaller, but because it is dense and hard, it resists deformation and retains energy efficiently. Lead #5 starts larger and carries useful energy, but it may deform during firing and impact. Deformation can increase drag and reduce predictable downrange behavior.In practical performance discussions, responsible suppliers should avoid exaggerated distance claims. TSS can extend effective range compared with many lead or steel options, but ethical range must be proven by pattern testing and local hunting rules. A load that works well in one shotgun, choke, and climate may perform differently in another. For this reason, hunters and ammunition brands should validate performance with real pattern boards rather than relying only on catalog numbers.Comparison pointTSS #9Lead #5AdvantagePractical notePellet diameterSmallerLargerLead #5Larger size does not tell the full storyMaterial densityMuch higherLowerTSS #9Density improves retained energyPellet countAbout 362 per ounceAbout 170 per ounceTSS #9More strikes in the same payloadDeformationVery lowModerateTSS #9Round pellets pattern more consistentlyTraditional acceptancePremium modern optionLong-established standardLead #5Regulation may limit lead useCostHighLowerLead #5Budget influences adoptionThe comparison is best summarized as density versus diameter. Lead #5 remains familiar and affordable where legal, but TSS #9 offers a powerful combination of small pellet size, dense patterns, and hard-pellet consistency. For premium ammunition companies, that combination can justify a higher retail price when supported by transparent testing.Pattern testing is the most important step in evaluating TSS #9 loads. A dense payload is only useful if it places enough pellets in the required target zone at the intended distance. In turkey hunting, many shooters evaluate pellet strikes in a defined circle and also examine the distribution across the head and neck outline. The goal is not simply the highest pellet number; it is an even, reliable pattern without dangerous gaps.For the Global Market, performance testing should be adapted to regional conditions. A brand selling in the southeastern United States may test around humid spring turkey seasons in Georgia, Alabama, and Mississippi. A European distributor may consider cooler conditions in Germany, France, Poland, or the United Kingdom. Exporters shipping through Qingdao, Ningbo, Shenzhen, Singapore, Rotterdam, or Los Angeles should also consider storage conditions, packaging durability, and lot consistency after long transport.Effective range should be described responsibly. TSS #9 can deliver excellent performance at distances where lead or steel may fail, but no supplier should promote careless long-range shooting. Ethical use requires verified pattern density, sufficient penetration, a properly matched choke, and compliance with local law. Buyers should request test data from multiple guns or at least understand the test conditions behind advertised results.Testing factorWhy it mattersTSS #9 expectationLead comparisonBuyer actionPattern countMeasures pellet strikesVery high potentialUsually lower in same payloadAsk for distance-specific resultsPattern evennessPrevents open gapsStrong with quality pelletsCan suffer from deformationReview actual targetsChoke compatibilityControls spreadRequires suitable designMore forgiving with softer leadFollow maker guidanceVelocity stabilityAffects energy and recoilLoad dependentLoad dependentCheck published dataEnvironmental storageAffects shell reliabilityPackaging dependentPackaging dependentTest after shipping and storageLot consistencyProtects brand reputationMust be verifiedMust be verifiedRequire batch QC recordsThis performance matrix confirms that TSS is not magic by itself. The pellet material is only one part of a system that includes hull, wad, buffer, powder, primer, crimp, choke, firearm, and user judgment. For commercial buyers, the best practice is to combine laboratory checks with field-style pattern testing.One of the strongest reasons for TSS #9 growth is its compatibility with smaller gauges. In the past, turkey hunters often favored 12 gauge loads because larger payloads were needed to achieve adequate pellet count and energy. TSS allows 20 gauge, 28 gauge, and even .410 bore platforms to become more practical for skilled hunters using carefully matched loads. This has opened new product categories for youth hunters, recoil-sensitive users, traveling hunters, and minimalist equipment preferences.In 12 gauge, TSS #9 is often used for maximum pattern density and premium long-range capability, though ethical range still depends on testing. In 20 gauge, it offers a strong balance of lower recoil and serious turkey performance. In 28 gauge, it supports lightweight field setups that were once considered niche. In .410 bore, TSS has been particularly influential because the small bore can now deliver pattern performance that older lead .410 turkey loads could not easily match.Gauge compatibility also affects manufacturing and sourcing. Smaller shells leave less room for payload and component tolerance, so shot size consistency matters. Hard TSS pellets require appropriate wad protection to avoid barrel or choke damage. Commercial buyers should not treat TSS pellets as a simple drop-in replacement for lead in all designs. Ammunition loading should follow qualified engineering, regulatory testing, and safe commercial standards.For global distributors, the most attractive gauges vary by region. The United States is a major market for turkey-specific 12 gauge and 20 gauge ammunition. Canada has demand in both hunting and non-toxic shot categories. European interest may be influenced by lead restrictions, game laws, and proof standards. Australia and New Zealand buyers often evaluate availability, import cost, and firearm preferences. In compact markets such as Japan and South Korea, specialty ammunition may be driven by licensed hunting communities and controlled distribution channels.TSS is much harder than lead. This hardness is a major reason for its strong pattern performance. When lead pellets accelerate through a shotshell and choke, they can flatten or become irregular. Deformed pellets experience more air resistance and may separate from the main pattern. TSS pellets are highly resistant to deformation, so more pellets remain spherical, fly predictably, and contribute to a consistent pattern.However, hardness also creates engineering responsibilities. Hard shot must be paired with suitable wad systems and load designs to protect the barrel and choke. Ammunition brands must understand pressure, payload, buffering, and component interaction. Retail buyers should choose reputable factory loads rather than unsafe experiments. For component buyers, hardness testing and size sorting are important quality-control steps.The hardness advantage is not limited to hunting. The same concept matters across precision sphere manufacturing: roundness, grade control, surface quality, and material consistency determine real-world performance. This is where experience in precision ball production becomes relevant. Companies with long histories in steel balls, chrome steel balls, stainless steel balls, and multi-material spheres understand inspection discipline, lot control, and dimensional repeatability. Buyers can review broader production capabilities through the SDBALLS product portfolio to understand how sphere manufacturing expertise supports different industrial and outdoor applications.Reduced deformation also improves the value proposition for premium loads. If a customer pays more for TSS, they expect the shell to pattern better than ordinary options. Hardness helps deliver that result, but only when the entire supply chain is controlled. Poorly sorted or contaminated shot can undermine the advantage. Therefore, serious buyers should evaluate not just price per kilogram, but also tolerance, cleanliness, packaging, traceability, and supplier responsiveness.TSS is expensive because tungsten is expensive, processing is specialized, and high-density spherical shot requires strict manufacturing control. Buyers should expect TSS #9 to cost much more than lead or steel shot. The final retail shell price may be several times higher than conventional turkey loads. Yet the market continues to grow because TSS offers clear performance advantages in premium hunting applications.A cost analysis should include more than raw material price. Import duties, shipping, insurance, packaging, exchange rates, minimum order quantities, inspection fees, and inventory timing can all affect landed cost. Tungsten supply is globally connected to mining, refining, and geopolitical factors. Buyers serving the Global Market should monitor sourcing stability from Asia, Europe, and North America, especially when planning seasonal demand before spring turkey seasons.Major trade hubs matter. TSS components and loaded ammunition may move through Qingdao, Shanghai, Ningbo, Shenzhen, Hong Kong, Busan, Singapore, Rotterdam, Hamburg, Antwerp, Los Angeles, Long Beach, Houston, Savannah, Vancouver, Melbourne, and Dubai. Delays at these ports can affect spring inventory. Premium ammunition brands should build procurement calendars early and avoid last-minute purchasing during peak hunting demand.There is also a difference between sourcing TSS pellets and sourcing complete TSS loads. Pellet sourcing requires ammunition engineering capability and regulatory compliance. Complete load sourcing requires verification of factory licensing, proof testing, packaging rules, labeling, and destination-country restrictions. Buyers should avoid suppliers that make extreme performance promises without documentation. A lower quote may become expensive if pellet density is inconsistent, size distribution is poor, or shipments fail inspection.For 2026, three sourcing trends are likely to shape the market. First, buyers will demand better traceability for tungsten supply chains. Second, non-toxic shot policies may increase interest in alternatives to lead. Third, sustainability claims will require more evidence, including responsible material sourcing and recyclable packaging. Digital quality records, automated optical sorting, and more precise pellet grading are expected to become stronger selling points.SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., supports global buyers with precision sphere manufacturing experience and integrated sourcing capability. Headquartered in Tai’an City, Shandong Province, China, the company has built more than 30 years of manufacturing experience since 1996. Its core products include carbon steel balls, chrome steel balls, and stainless steel balls in grades from G10 to G1000, serving bearing, automotive, hardware, grinding, caster, sliding system, and ball transfer applications.From a technological capability perspective, SDBALLS focuses on dimensional control, material consistency, surface quality, and inspection discipline. These strengths are relevant to any buyer evaluating spherical media, including hunting and outdoor markets where pellet uniformity affects pattern performance. The company’s quality approach is supported by IATF 16949, ISO 9001, and ISO 14001 certifications. Buyers interested in inspection systems and standards can learn more through the SDBALLS quality and technical resources.From a manufacturing capability perspective, SDBALLS operates three production facilities with annual capacity exceeding 5,000 tons. This scale allows the company to serve customers across more than 50 countries while maintaining stable production for different grades, materials, and applications. In addition to its steel ball portfolio, SDBALLS produces lead-free steel shot for hunting and outdoor markets, including annealed and plated options designed to meet CIP-compliant hardness expectations for EU and US markets.From a service capability perspective, SDBALLS acts as an integrated supply partner for buyers who need more than one material category. The company helps source multi-material spheres such as plastic, glass, ceramic, copper, and aluminum, supporting procurement consolidation for international customers. This is valuable for distributors, industrial buyers, and outdoor product brands that want one reliable partner instead of managing many small suppliers. More company background is available on the SDBALLS about us page.For the TSS #9 topic specifically, SDBALLS’ role should be understood accurately. The company’s established expertise is precision ball manufacturing and lead-free steel shot production, while its integrated supply model can help buyers evaluate broader spherical material requirements. For ammunition-related procurement, customers should clarify destination regulations, intended application, required documentation, and whether they need steel shot, tungsten alloy shot sourcing support, or other spherical media. Application examples can be explored through the SDBALLS application guide.No. Hunting ammunition rules vary by country, state, province, and hunting area. Some regions restrict lead, some regulate shot size, and some have specific rules for turkey hunting, wetlands, or public land. Buyers and hunters should check local law before purchasing or using TSS #9 loads.The count comes from the small #9 pellet diameter combined with tungsten alloy density. A typical #9 pellet is about 0.080 inch. Because the pellets are small, many fit into one ounce, while the high density helps each pellet retain useful energy.It can replace lead #5 in some performance roles, but it should not be treated as a simple loading substitute. TSS is much harder and denser, so safe ammunition design requires appropriate components, testing, and manufacturer guidance.For premium turkey loads, TSS #9 often offers denser patterns and strong penetration with more pellets per ounce. Lead #5 remains cheaper and familiar where legal. The better choice depends on regulation, budget, firearm setup, and verified pattern results.TSS #9 is widely used in 12 gauge and 20 gauge, and it has made 28 gauge and .410 bore turkey loads more practical. Smaller gauges benefit because TSS provides high pellet count and density in limited payload space.Tungsten is a costly raw material, and producing consistent high-density spherical shot requires specialized processing and inspection. Shipping, duties, quality documentation, and seasonal demand also influence the final cost.Buyers should compare density, tungsten content, pellet size tolerance, sphericity, cleanliness, hardness, packaging, lot traceability, export experience, and response speed. The lowest price is not always the best value if quality is inconsistent.Key trends include stricter lead policies, more small-bore premium loads, improved optical sorting, better batch traceability, sustainability claims, recyclable packaging, and stronger demand for documented tungsten sourcing.SDBALLS manufactures lead-free steel shot for hunting and outdoor markets, along with precision steel balls for industrial applications. The company also provides integrated sourcing support for multiple sphere materials, depending on buyer requirements.Buy based on verified performance, not claims alone. Request specifications, quality documents, and pattern data, then confirm local regulations and application requirements before committing to large orders. -
Global Market Guide to 1 Inch HDPE Plastic Balls Specs
For most global purchasing teams, a 1 inch HDPE plastic ball means a spherical component made from high-density polyethylene with a nominal diameter of 25.4 mm. It is selected when the application needs low density, floating behavior, good chemical resistance, electrical insulation, low water absorption, and moderate mechanical strength rather than high load-bearing precision. In general use, HDPE balls are not equivalent to chrome steel bearing balls or high-precision ceramic balls; they are economical, lightweight, corrosion-resistant polymer spheres used in valves, floats, fluid control, level indication, check mechanisms, packaging systems, light-duty handling, chemical tanks, and water-related equipment.The quick buying rule is simple: choose HDPE when the ball must resist moisture, many acids and alkalis, saltwater, detergents, and outdoor exposure while remaining light enough to float. Choose another material if the part must operate continuously above about +70°C, carry heavy compressive loads, resist aromatic solvents, or maintain ultra-tight bearing-grade geometry. For international buyers in the Global Market, including importers working through Shanghai, Qingdao, Ningbo, Singapore, Rotterdam, Hamburg, Los Angeles, Dubai, and Mumbai, the main commercial questions are diameter tolerance, surface finish, production grade, certification expectations, packaging, lead time, and whether the supplier can support mixed-material sourcing.ItemTypical 1 Inch HDPE Ball ValueBuyer MeaningNominal diameter1 inch / 25.4 mmUsed for inch-based assemblies and metric drawings with 25.4 mm conversionMaterialHigh-density polyethyleneSemi-crystalline thermoplastic with low density and chemical resistanceDensityAbout 0.94 to 0.96 g/cm³Usually floats in water and many aqueous solutionsOperating temperatureApproximately -30°C to +70°CSuitable for ambient, chilled, and moderate warm serviceWater absorptionVery lowStable in humid, marine, and water-treatment environmentsTypical useFloats, valves, light-duty balls, tank systemsBest where corrosion resistance and low weight matter more than high hardnessThis table is a practical starting point rather than a universal guarantee. Exact values depend on resin grade, molding method, pigment, additives, post-processing, and inspection standard. When buying for safety-critical or regulated equipment, the engineering drawing and supplier test report should take priority over generic data.HDPE is a semi-crystalline thermoplastic. Its molecular structure contains long polyethylene chains with relatively low branching, which allows the chains to pack closely and form crystalline regions. These crystalline regions increase stiffness, chemical resistance, and dimensional stability compared with many lower-density polyethylene materials. At the same time, the amorphous regions provide toughness and impact resistance. This combination explains why HDPE balls are widely used in wet, outdoor, chemical, and low-friction environments.Because HDPE is thermoplastic, it can be molded, machined, welded, and recycled under suitable conditions. It softens with heat and hardens again after cooling, unlike thermoset plastics that cannot be remelted. For plastic balls, manufacturers may use injection molding, compression molding, extrusion followed by machining, or custom finishing depending on the required tolerance and volume. Standard 1 inch balls for industrial use are often supplied as economical molded spheres, while tighter grades may need secondary sizing, polishing, or precision machining.HDPE has a naturally waxy surface feel and a low coefficient of friction compared with many engineering materials. This can be helpful in sliding, rolling, and non-lubricated contact, although it should not be confused with the performance of bearing-grade steel, POM, PTFE, or precision ceramic materials. It is also electrically insulating, non-magnetic, and resistant to many everyday chemicals. These properties make it attractive for water treatment plants, agricultural tanks, marine systems, chemical dosing equipment, and lightweight mechanical devices.From a technical capability perspective, SDBALLS Industry Corp supports customers by matching ball material to use conditions rather than treating every sphere as the same product. The company’s core heritage is precision steel ball manufacturing, but its integrated supply approach allows buyers to source plastic, glass, ceramic, copper, aluminum, and other spheres through one professional channel. For HDPE balls, this means customers can discuss tolerance, function, environment, packaging, and replacement options with a team familiar with both precision ball terminology and industrial procurement practice.PropertyHDPE CharacteristicPractical EffectVS Common AlternativeStructureSemi-crystalline polyethyleneGood balance of stiffness and toughnessMore rigid than LDPE, less rigid than many nylonsDensityLower than waterFloating applications are possiblePVC generally sinksWater behaviorVery low absorptionMaintains weight and dimensions in wet serviceNylon absorbs more moistureChemical resistanceStrong against many acids and alkalisUseful in tanks and dosing systemsSome plastics crack or swell fasterElectrical behaviorInsulating and non-conductiveSuitable for many electrical separation usesMetal balls are conductiveHeat resistanceModerateGood for ambient use, not high-temperature servicePTFE and PEEK tolerate higher temperaturesThe comparison shows that HDPE is a balanced choice, not a universal best choice. Its advantage is cost-effective performance in wet and chemically exposed environments, especially where low weight is useful. Its limitation is moderate heat resistance and lower hardness than metals or high-performance engineering plastics.Diameter tolerance is one of the most important details in a 1 inch HDPE plastic ball order. The phrase “1 inch” only identifies the nominal size. It does not automatically define the permitted size variation, roundness, surface finish, gate mark, parting line, color consistency, or inspection method. For a simple floating cover or tank media application, a broader tolerance may be acceptable. For a valve seat, metering mechanism, or automated assembly, tighter dimensional control may be required.Unlike hardened steel bearing balls, HDPE balls are flexible and can deform slightly under measurement pressure. Therefore, buyers should specify the inspection method, measuring load, sample size, and acceptance criteria when dimensions are critical. A micrometer, optical measurement system, ring gauge, or coordinate measuring method may produce slightly different results if the ball is soft or has a visible molding line. This is why professional suppliers ask about the function of the ball, not only the requested diameter.Precision grades for plastic balls are often commercial grades rather than traditional bearing ball grades such as G10, G25, or G100. Some suppliers use internal tolerance categories such as general grade, selected grade, precision molded grade, or machined grade. For international trade, it is best to confirm the tolerance in millimeters or inches instead of relying only on a grade name. For example, a buyer may ask for 25.4 mm diameter with ±0.10 mm tolerance, selected roundness, white color, smooth surface, and bulk packaging.Grade TypePossible Diameter ToleranceSurface ExpectationTypical UseGeneral molded gradeBroad commercial toleranceVisible gate or parting line may existFloats, covers, tank fillers, low-cost usesSelected molded gradeModerate toleranceBetter visual selectionValve balls, dispensers, simple mechanismsPrecision plastic gradeTighter sorted toleranceSmoother and more consistentMetering, OEM assemblies, controlled fitMachined HDPE ballDrawing-based toleranceTooling marks possible but controlledCustom engineering partsPolished or finished gradeApplication-specificImproved appearance and rolling feelVisible products, demonstration devicesBearing substitute claimRequires careful reviewNot equal to hardened steel bearing qualityOnly for low-load, non-critical rollingThis table highlights a common purchasing risk: a low-cost molded ball may be perfectly suitable for floating service but unsuitable for a sealed valve seat. Buyers should attach drawings, assembly photos, or old sample details whenever possible. If the ball interfaces with an O-ring, spring, seat, groove, or tube, the tolerance should be verified before mass production.HDPE is valued for light weight and toughness. A 1 inch HDPE ball is much lighter than a steel, glass, ceramic, PVC, or acetal ball of the same diameter. Its density is typically around 0.94 to 0.96 g/cm³, which means it normally floats in water. This density also reduces shipping weight and can lower transportation cost for high-volume orders moving through global logistics hubs such as Qingdao Port, Shanghai Port, Port Klang, Jebel Ali, Long Beach, Antwerp, and Felixstowe.Hardness is moderate. Depending on resin and test method, HDPE may fall around Shore D 60 to 70. It is harder than soft elastomers but softer than POM, nylon, PVC, ceramic, and metal. Its mechanical strength is suitable for many low to medium stress tasks, but it should not be used where the ball carries high point loads, high-speed bearing loads, heavy crushing forces, or abrasive grinding duty. Under constant load, HDPE may creep over time, especially at elevated temperature.The mechanical performance of an HDPE ball also depends on wall integrity if it is hollow, or internal uniformity if it is solid. Solid balls are stronger and more dimensionally stable under compression, while hollow balls may provide enhanced buoyancy and lower weight. For check valves and floating valves, the difference between solid and hollow construction can be decisive. Buyers should not assume that all 1 inch HDPE balls are solid unless the quotation confirms it.SpecificationTypical HDPE Ball BehaviorBuying AdviceDensityAbout 0.94–0.96 g/cm³Confirm if the liquid is denser or lighter than waterHardnessModerate Shore D rangeAvoid heavy impact or high-pressure sealing without testingTensile strengthModerate for plasticSuitable for light mechanical contactImpact resistanceGood at normal temperatureUseful for handling and outdoor systemsCreep resistanceLimited under long-term loadDo not design as a highly loaded structural bearingWear resistanceFair in clean conditionsUse alternatives for abrasive slurry or high-speed motionFor mechanical design, the safest method is application testing. A specification sheet can indicate likely performance, but it cannot fully predict the behavior of a ball moving in a real valve, tank, pump, chute, or actuator. Fluid chemistry, pressure, temperature, seat geometry, and cycle frequency all affect service life.A practical operating range for many HDPE balls is approximately -30°C to +70°C. At the low end, HDPE generally maintains toughness better than some more brittle plastics, which helps in cold storage, winter agriculture, marine equipment, and outdoor water systems. At the high end, the material gradually softens, becomes more flexible, and may show greater creep. Continuous service near the upper limit should be reviewed carefully, especially if the ball is loaded, compressed, or required to maintain a tight seal.Temperature must be considered together with chemicals and stress. A chemical that is acceptable at 20°C may become more aggressive at 60°C. A ball that works well in an open tank may deform in a hot valve seat under spring pressure. In tropical markets, outdoor black plastic parts may become hotter than ambient air under sunlight. In cold markets, impact testing may be needed if the ball is dropped, cycled, or struck at subzero temperature.For logistics, HDPE balls are generally easy to ship and store. They do not need rust prevention like carbon steel balls, and they are not fragile like glass balls. However, cartons should be protected from excessive heat, direct flame, sharp compression, and contamination. For sea freight, exporters often use plastic bags inside cartons, woven bags, or drums depending on quantity and cleanliness requirements.Chemical resistance is one of the leading reasons to choose HDPE. The material performs well against many dilute acids, alkalis, salts, alcohols, detergents, and water-based solutions. It is widely used in chemical containers, agricultural sprayers, wastewater treatment, swimming pool systems, aquaculture, marine equipment, and industrial fluid handling. Low water absorption helps maintain predictable buoyancy, dimension, and weight after long exposure to water.However, HDPE is not resistant to every chemical. Strong oxidizing agents, some hydrocarbons, chlorinated solvents, aromatic solvents, and high-temperature chemical mixtures may cause swelling, stress cracking, softening, or loss of mechanical performance. Environmental stress cracking is a real concern when chemical exposure, tensile stress, and time combine. For critical chemical service, buyers should request compatibility review and conduct immersion testing with the actual liquid.In water treatment markets from Singapore and Dubai to São Paulo and Johannesburg, HDPE balls may be used as floating covers to reduce evaporation, limit odor, reduce light exposure, or separate liquid surfaces. In such applications, UV stability may be important. Natural HDPE can degrade over long outdoor exposure, so black, UV-stabilized, or additive-modified grades may be recommended. If the project is government-funded or infrastructure-related, documentation and traceability requirements should be clarified at the quotation stage.HDPE, PP, and PVC are all common plastic ball materials, but they serve different needs. HDPE is usually chosen for toughness, water resistance, floatation, and broad chemical compatibility at moderate temperatures. PP is also lightweight and chemically resistant, often with better heat tolerance in some conditions, but it can be more brittle in cold environments. PVC is denser, generally sinks in water, offers good rigidity and chemical resistance in many systems, but is heavier and may not be the best choice for floating applications.ApplicationHDPE BallPP BallPVC BallFloating in waterExcellent because density is below waterExcellent because density is also lowPoor because PVC usually sinksCold outdoor useGood toughness in many casesMay become more brittleModerate, grade dependentWarm chemical serviceModerate temperature limitOften better at higher temperatureGood rigidity but temperature limitedLow-cost tank mediaVery suitableVery suitableSuitable when sinking is acceptableRigid valve ballUseful for light seatingUseful but check cold impactMore rigid but heavierElectrical insulationGoodGoodGood, but formulation mattersThe VS comparison suggests that material selection should be application-led. If the ball must float in a tank at ambient temperature, HDPE or PP may be preferred. If the system needs a sinking, rigid plastic ball, PVC may be suitable. If the application sees hot chemical exposure, PP may deserve evaluation. If cold impact and toughness are priorities, HDPE is often a strong candidate.HDPE is a good electrical insulator and is non-magnetic. This makes 1 inch HDPE balls useful in applications where metal contamination, electrical conduction, or magnetic response must be avoided. They can be used in demonstration equipment, separation systems, low-voltage insulation spacing, float switches, non-conductive guides, and certain sensor environments. As always, buyers should not use generic HDPE balls in certified electrical safety devices without formal approval and testing.Floating applications are especially important. Because HDPE is less dense than water, it can act as a float, surface cover, level indicator, or buoyant valve component. In chemical tanks, balls may float on the liquid surface to reduce evaporation, odor, splashing, or heat loss. In agriculture, they can help in irrigation tanks and nutrient reservoirs. In marine and aquaculture settings, they may be used where saltwater resistance and low water absorption matter.For floating design, confirm the liquid density. A ball that floats in fresh water may behave differently in oils, solvents, brines, or concentrated chemical solutions. The ball diameter also affects visibility, lift force, and surface coverage. A 1 inch ball is compact and easy to pack, but larger balls may be more visible and provide more buoyancy per unit. Hollow balls can increase buoyancy but may introduce leakage risk if the shell is damaged.SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., supports global buyers that need dependable ball products and practical sourcing help. Founded in 1996 and based in Tai’an City, Shandong Province, China, the company has built its reputation in precision steel balls while also helping customers consolidate procurement of multi-material spheres, including plastic balls such as HDPE, PP, PVC, POM, nylon, PTFE, glass, ceramic, copper, and aluminum options.Manufacturing capability is the foundation of the company’s supply strength. SDBALLS operates multiple production facilities and has long experience in carbon steel balls, chrome steel balls, stainless steel balls, and lead-free steel shot. Its steel ball grades range from high-precision requirements to general industrial grades, supporting bearing, automotive, caster, sliding system, ball transfer, hardware, and grinding applications. This manufacturing background gives the team a strong understanding of diameter control, surface quality, inspection discipline, packaging, and international shipment expectations.Service capability is equally important for plastic ball buyers. A customer may begin with a simple request for “1 inch HDPE balls” but later need PP comparison, stainless steel alternatives, ceramic wear resistance, or mixed shipment consolidation. SDBALLS helps customers compare materials, confirm drawings, check tolerance feasibility, coordinate samples, and plan bulk orders. The company serves customers in more than 50 countries and is familiar with export documentation, sea freight, air freight, and buyer communication across time zones.Quality systems also support trust. SDBALLS maintains management certifications including IATF 16949, ISO 9001, and ISO 14001 for its manufacturing operations. While specific plastic ball certification depends on the product and supply route, the company’s quality culture helps global purchasers manage risk. Buyers can learn more through the company’s corporate background and manufacturing story, review available categories on the industrial ball product page, explore quality and technical support, and compare end uses through the application guide.What is the most important specification for a 1 inch HDPE ball? The most important specification is not only the diameter. Buyers should define diameter tolerance, solid or hollow construction, color, surface quality, operating liquid, temperature, chemical exposure, packing, and inspection standard.Can HDPE balls replace steel balls? Only in light-duty applications where low weight, corrosion resistance, and insulation are more important than hardness, compressive strength, and bearing precision. For bearings, grinding, high load, or high-speed rolling, steel, ceramic, or other engineering materials are usually better.Do 1 inch HDPE balls float? In most water-based liquids, yes, because HDPE density is typically below water. However, floating performance depends on liquid density, whether the ball is solid or hollow, temperature, and contamination.Are HDPE balls suitable for food or drinking water? They may be suitable only when made from compliant resin and produced under the required hygiene and regulatory conditions. Buyers must request the correct declaration or test documentation for food-contact or potable-water use.What industries use HDPE plastic balls? Common industries include water treatment, chemical processing, agriculture, marine equipment, aquaculture, packaging machinery, light mechanical systems, tank manufacturing, laboratory equipment, and educational demonstration devices.How should global buyers compare local suppliers? Compare more than price. Check whether the supplier understands tolerance, chemical compatibility, sample approval, export packaging, documentation, and repeatability. Buyers in North America, Europe, the Middle East, Southeast Asia, and South America often benefit from working with a sourcing partner that can consolidate several ball materials in one shipment.What are the main 2026 trends for HDPE and plastic balls? The market is moving toward better traceability, more recycled and recyclable resin discussions, stronger environmental documentation, lower-carbon logistics, digital inspection records, and application-specific material selection. Policy pressure on plastics is increasing in many regions, so buyers should expect more questions about resin origin, restricted substances, packaging waste, and end-of-life management.What is the best buying advice? Start with the application, not the material name. Tell the supplier what the ball must do, where it will be used, what liquid or gas it contacts, what temperature it sees, and what failure would mean. Then confirm samples before bulk purchasing. This approach reduces risk and helps the supplier recommend HDPE, PP, PVC, stainless steel, ceramic, or another material with confidence. -
8mm Steel Slingshot Ammo Guide for Global Market
For buyers, distributors, outdoor brands, and technical purchasers in the Global Market, 8mm steel balls remain one of the most popular slingshot ammunition sizes because they balance manageable weight, stable flight, affordable cost, and broad compatibility with common flat bands and tubular bands. This guide explains how to evaluate 8mm steel ball weight, diameter tolerance, material choices, kinetic energy, surface finish, safety, storage, and sourcing. It also compares 8mm balls with 6mm, 9mm, and 10mm alternatives so procurement teams can make informed purchasing decisions.The information below is written for lawful sporting, training, recreational target shooting, and outdoor product supply applications. Always follow local rules in your country, state, province, municipality, club, range, park, warehouse, port, or distribution center. Slingshot ammunition should be handled as a controlled impact projectile, stored responsibly, and used only in safe, approved environments.An 8mm steel slingshot ball typically weighs about 2.05 to 2.10 grams when made from standard carbon steel, chrome alloy bearing steel, or stainless steel with density around 7.75 to 7.90 g/cm³. The nominal diameter is 8.00mm, but commercial tolerance can vary widely depending on grade, from rough bulk ammunition to precision steel balls. For most recreational slingshot users, an 8mm ball is a practical middle-size option: lighter and faster than 9mm or 10mm balls, more stable and impactful than 6mm balls, and usually economical for high-volume practice.For purchasing in the Global Market, the best choice depends on the customer segment. Entry-level recreational kits often use carbon steel 8mm balls because they are cost-effective. Premium outdoor brands may choose chrome steel or stainless steel for improved hardness, finish, corrosion resistance, and consistency. Importers serving humid coastal areas such as Singapore, Rotterdam, Hamburg, Dubai, Santos, Los Angeles, Durban, or Manila should pay close attention to anti-rust packaging, oiling, plating, and stainless options. Buyers supplying strict retail channels should also confirm labeling, age restrictions, transportation classification, and local compliance requirements.Selection PointQuick RecommendationWhy It MattersTypical BuyerDiameter8.00mm nominalCommon size with broad slingshot compatibilityOutdoor brands, distributors, clubsWeightAbout 2.05–2.10g per ballBalances speed, trajectory, and band loadSport and training usersMaterialCarbon steel for value, stainless for corrosion resistanceControls cost, durability, and storage lifeRetailers and importersToleranceChoose grade based on accuracy needsMore consistent diameter improves repeatabilityPremium ammo suppliersFinishPolished, oiled, plated, or stainlessReduces rust and improves handlingCoastal and humid marketsSafetyUse with eye protection and safe backstopPrevents ricochet and accidental injuryAll users and sellersThe simple buying rule is this: select 8mm carbon steel balls for economical practice, chrome steel balls for better dimensional consistency and hardness, and stainless steel balls when corrosion resistance and clean retail presentation matter most. For global wholesale programs, request samples from the supplier, test them with your preferred band setup, verify packaging under local humidity conditions, and check compliance before mass shipment.The nominal diameter of an 8mm steel ball is 8.00 millimeters. Because a ball is a three-dimensional sphere, small diameter changes can influence volume, weight, flight consistency, pouch fit, and band loading. In practical use, a low-cost bulk ball may be acceptable for casual target practice, while a better-controlled precision ball can support more repeatable grouping for experienced users.The theoretical volume of an 8mm sphere is about 268.08 mm³. With steel density near 7.85 g/cm³, the calculated weight is about 2.10 grams. In real manufacturing, weight varies slightly with alloy composition, grinding process, surface coating, and tolerance grade. Stainless steel may weigh slightly differently depending on the exact grade, while plating adds a very small surface mass. For normal slingshot ammunition, these small changes are less important than roundness, surface smoothness, rust condition, and batch consistency.SpecificationTypical 8mm Steel Ball ValueLow-Cost AmmoPrecision-Oriented AmmoPractical ImpactNominal diameter8.00mmMay vary more by batchControlled closer to target sizeAffects pouch fit and groupingApproximate weight2.05–2.10gWider variationNarrower variationAffects trajectory and repeatabilityRoundnessDepends on gradeMay be visibly less uniformMore sphericalAffects flight stabilitySurface roughnessPolished or semi-polishedMay have more marksSmoother finishAffects corrosion and pouch releaseDimensional toleranceGrade-dependentUsually wider toleranceCan be G10 to G1000 depending needControls consistencyPackaging conditionOiled, dry, plated, or baggedBasic plastic bag or cartonMoisture-controlled packagingAffects shelf lifeDimensional tolerance is often misunderstood. A tighter grade is not always necessary for every slingshot market. For general outdoor retail, customers may prioritize price, clean appearance, and rust-free delivery. For clubs, competition-style target shooting, or premium branded ammunition, tighter diameter distribution can justify a higher price. When ordering, buyers should define the intended use: casual practice, training kit, outdoor sports accessory, retail blister pack, bulk refill jar, or precision target product.For importers shipping through global hubs such as Shanghai, Qingdao, Ningbo, Busan, Jebel Ali, Antwerp, Rotterdam, Long Beach, New York, or Felixstowe, it is also important to specify packing weight and carton strength. Steel balls are dense; a small carton can become very heavy. Strong inner bags, moisture barriers, reinforced cartons, pallet strapping, and clear labeling reduce damage during sea freight, air freight, rail, or truck transportation.Material choice is one of the most important decisions for 8mm steel slingshot balls. The three common options are carbon steel, alloy steel such as chrome bearing steel, and stainless steel. Each has a different balance of cost, hardness, corrosion resistance, magnetic response, surface finish, and market positioning.Carbon steel balls are widely used because they are affordable, available in high volume, and suitable for general recreational target shooting. They can be polished, oiled, blackened, zinc plated, nickel plated, or otherwise protected against rust. Carbon steel is a good choice for price-sensitive markets and high-consumption practice packs.Alloy steel balls, especially chrome steel balls used in bearing applications, usually provide higher hardness and better consistency when produced under precision standards. They are popular when buyers want a premium feel, smoother finish, and improved dimensional reliability. However, chrome steel still needs corrosion protection because it is not stainless.Stainless steel balls offer better corrosion resistance, cleaner appearance, and longer shelf life in humid or marine environments. They are usually more expensive, but they fit markets where rust complaints are costly, such as retail chains, e-commerce stores, and coastal distributors. Stainless steel is also attractive for branded outdoor kits where packaging presentation matters.MaterialMain AdvantageMain LimitationBest UseCarbon Steel vs Stainless Steel NoteCarbon steelLowest cost and high availabilityNeeds rust protectionBulk practice ammunitionCheaper than stainless but less corrosion resistantChrome alloy steelHigh hardness and good precision potentialCan rust without oil or coatingPremium target ammo and industrial crossoverHarder feel than many stainless grades304 stainless steelGood general corrosion resistanceHigher price than carbon steelRetail and humid marketsCleaner shelf appearance316 stainless steelBetter marine corrosion resistancePremium costCoastal and marine environmentsUseful near saltwater marketsPlated carbon steelImproved appearance at moderate costCoating can wear or scratchRetail packs and mid-range productsCost bridge between carbon and stainlessAnnealed steelLower hardness options possibleApplication-specific supplyMarkets with hardness requirementsMust be specified clearlyIn the Global Market, there is no universal best material. Buyers in dry inland regions may prefer cost-efficient carbon steel. Distributors in tropical climates such as Southeast Asia, Central America, West Africa, or northern Australia often choose enhanced anti-rust packaging or stainless steel. European and North American retailers may request stronger documentation, safer labeling, and consistent retail presentation. Large e-commerce sellers usually value rust resistance because customer reviews can be affected by surface staining during storage.SDBALLS Industry Corp has long experience producing carbon steel balls, chrome steel balls, and stainless steel balls for industrial and outdoor markets. Its technical capability includes precision grades from G10 to G1000, which allows customers to align tolerance and finish with actual product positioning rather than overpaying for unnecessary precision. More information about manufacturing and product categories is available through the company’s steel ball product range.Kinetic energy is often used to compare projectile performance. It is calculated as one half of mass multiplied by velocity squared. For an 8mm steel ball weighing about 2.10 grams, energy increases quickly as velocity rises. However, energy figures should be interpreted responsibly. They are useful for comparing ammunition size, band matching, and safe backstop requirements, not for unsafe or unlawful use.Velocity depends on band strength, draw length, pouch design, user technique, temperature, ball weight, and slingshot setup. A lightweight ball can be launched faster, while a heavier ball may carry more momentum at lower speed. The same slingshot band that works comfortably with 8mm steel may feel underloaded with 6mm balls or overloaded with 10mm balls. This is why testing is important before finalizing product kits.VelocityApproximate 8mm Ball EnergyPerformance ImpressionBackstop RequirementSafety Note40 m/sAbout 1.7 JLow-power practice levelSoft, controlled target areaEye protection still required50 m/sAbout 2.6 JCommon recreational speedReliable catch box recommendedCheck ricochet risk60 m/sAbout 3.8 JMore energetic target shootingDense backstop requiredUse only in safe direction70 m/sAbout 5.1 JHigh recreational energyPurpose-built backstopGreater rebound hazard80 m/sAbout 6.7 JAdvanced setup rangeStrong impact containmentStrict range discipline90 m/sAbout 8.5 JVery high for casual useProfessional-grade containmentNot for informal environmentsEnergy is only one part of ballistic performance. Accuracy also depends on consistent ball size, clean release, balanced band pull, stable pouch seating, and user skill. A highly polished 8mm steel ball with consistent diameter may produce better groups than a cheaper ball with uneven size distribution. Surface defects, rust spots, flattened areas, or foreign debris can disturb release and flight.Buyers building private-label slingshot kits should test ammunition and bands together rather than separately. If the band is too light for the ball, velocity may be low and trajectory may drop quickly. If the band is too heavy, users may struggle with control and safety. For target shooting sets sold online, a moderate band and 8mm steel ball pairing is often easier for general users than a heavy band with 10mm ammunition.The five key factors in selecting 8mm slingshot steel balls are band matching, accuracy, range, safety, and cost. These factors interact with each other. A low-cost ball may be acceptable for short-range practice, but poor tolerance or rust may reduce customer satisfaction. A premium ball may improve accuracy, but it may not be necessary for entry-level kits. A powerful band may increase speed, but it may also increase user fatigue and safety risk.Band matching means choosing ammunition that works efficiently with the slingshot’s elastic system. An 8mm steel ball is commonly compatible with many medium flat bands and tubular bands. It is not too light for most standard setups and not too heavy for average recreational users. Product developers should test the ball with the exact band thickness, taper, active length, pouch size, and draw length planned for sale.Accuracy comes from consistency. Diameter tolerance, roundness, surface finish, ball weight distribution, pouch release, and user form all matter. For distributors targeting training clubs or skilled hobbyists, a higher-grade ball may be worth the added cost. For casual markets, a clean, rust-free, visually uniform ball is usually more important than ultra-tight precision.Range depends on velocity, launch angle, drag, ball weight, and wind. An 8mm steel ball offers practical short-to-medium recreational target range. Compared with 6mm balls, it generally holds energy better. Compared with 10mm balls, it may shoot flatter with moderate bands because it is lighter. For safe target use, sellers should encourage customers to shoot only in controlled areas with a backstop.Safety is a commercial requirement, not just a user responsibility. Retailers should include clear warnings, age guidance where required, eye protection recommendations, and safe-use instructions. Steel balls can ricochet from hard surfaces such as stone, concrete, metal, glass, or dry hardwood. A safe setup uses a suitable target box, soft capture material, and a clear downrange area.Cost includes more than the unit price per kilogram. It includes rust claims, packaging failure, freight damage, customer reviews, customs delays, compliance checks, and inventory losses. A slightly higher-grade ball with better packaging may reduce total cost for e-commerce and retail brands. Bulk distributors may still prefer economical carbon steel if they have fast inventory turnover and dry storage.FactorLow-Cost StrategyPremium StrategyRisk if IgnoredRecommended Buyer ActionBand matchingUse standard 8mm with medium bandsTest multiple bands and pouch sizesPoor speed or difficult drawRun sample shooting testsAccuracyAccept wider tolerance for practiceSpecify better grade and finishInconsistent groupingMeasure diameter and roundnessRangePosition for short-range practiceOptimize ball and band pairingCustomer disappointmentState realistic use distanceSafetyBasic warning labelDetailed safe-use instruction kitInjury, claims, bad reviewsAdd eye protection and backstop guidanceCostBulk carbon steel packagingRetail-ready coated or stainless productHidden logistics and rust costsCompare total landed costComplianceGeneral export documentsMarket-specific labeling and recordsCustoms or sales restrictionsCheck local law before shipmentFor global buyers, a practical development process is to request three sample options: economical carbon steel, plated or polished carbon steel, and stainless steel. Test them in the same slingshot, same band, same target setup, and same humidity condition. Then compare accuracy, rust resistance, appearance, packing quality, and total landed cost. This approach is more reliable than choosing by price alone.Different ammunition sizes serve different customer needs. The 6mm steel ball is light, fast, economical, and suitable for lower-power practice. The 8mm ball is a balanced mainstream size. The 9mm ball provides more mass and impact but requires stronger band matching. The 10mm ball is heavier and typically used by experienced users with suitable equipment and strict safety discipline.SizeApproximate Steel Ball WeightSpeed PotentialImpact PotentialBest Market Position8mm VS Other Sizes6mmAbout 0.88gHigh with light bandsLowerYouth training where legal, low-power target kits8mm is heavier and more stable7mmAbout 1.41gFast and easy to shootModerate-lowEntry-level target practice8mm carries more energy8mmAbout 2.10gGood with medium bandsBalancedMainstream recreational target ammoMost balanced option9mmAbout 3.00gModerateHigherExperienced hobbyists8mm is easier for general users10mmAbout 4.11gLower unless strong bands are usedHighAdvanced controlled target setups8mm has lower fatigue and flatter feel12mmAbout 7.10gLow with normal bandsVery highSpecialized uses only8mm is safer and more retail-friendlyFor retailers, 8mm is often the easiest size to stock because it suits a wide audience. It is large enough to handle easily, affordable enough for repeat purchases, and compatible with many standard slingshot designs. In contrast, 6mm balls may be too small for some pouches and easier to spill, while 10mm balls can be too heavy for casual users and may raise safety concerns if sold without clear instructions.For distributors offering a full product range, a good assortment could include 6mm for light practice, 8mm as the core SKU, 9mm for users seeking a heavier option, and 10mm for advanced target setups. Each size should have distinct packaging, warning labels, and use recommendations to reduce confusion.Surface finish affects appearance, handling, rust resistance, pouch release, and customer perception. A bright polished ball looks clean and premium, but if it is carbon steel without proper protection, it can still rust during ocean freight or warehouse storage. A lightly oiled ball resists corrosion, but retail customers may dislike oily residue if the product is not packed properly. Plated balls can improve appearance and corrosion resistance, while stainless steel offers inherent rust resistance under many normal conditions.Common surface options include polished carbon steel, anti-rust oiled carbon steel, zinc-plated steel, nickel-plated steel, blackened steel, chrome steel with protective oil, and stainless steel. The correct choice depends on market climate, packaging method, shelf life expectation, and retail positioning.In humid trade routes, corrosion protection deserves special attention. A shipment from East Asia to Europe, North America, South America, Africa, or the Middle East may spend weeks in containers with changing temperatures. Condensation can occur during sea freight, especially when cargo moves between tropical and temperate climates. Desiccants, sealed inner bags, vapor corrosion inhibitor packaging, and pallet wrapping can reduce risk.Buyers should define acceptable surface condition in the purchase agreement. Terms such as “bright,” “polished,” or “anti-rust” can be interpreted differently unless supported by samples, photos, inspection standards, and packaging specifications. If the product will be sold through online marketplaces, visual consistency is especially important because customers often judge quality from appearance.Finish or CoatingCorrosion ResistanceAppearanceCost LevelBest ForVS Stainless SteelPlain polished carbon steelLow without protectionBright when newLowFast-turnover bulk marketsCheaper but less durable in humidityOiled carbon steelModerateSlight oil filmLow to moderateWholesale cartons and refill bagsLower cost but may feel oilyZinc plated steelModerate to goodBright or matte silverModerateRetail packsGood value but coating can wearNickel plated steelGoodSmooth and premiumModerate to highBranded ammunitionAttractive but not inherent stainlessBlackened steelDepends on process and oilDark tactical lookModerateSpecial product linesStyle advantage, not always better corrosionStainless steelGood to excellent by gradeClean metallic finishHighHumid, coastal, and premium marketsHigher cost but stronger shelf stabilityFor sustainability in 2026 and beyond, buyers are increasingly asking for coatings with lower environmental burden, cleaner packaging, and reduced oil leakage. Suppliers that can offer efficient process control, recyclable packaging options, and stable quality documentation will have an advantage in global retail channels.Steel balls are simple products, but they require professional storage and transportation planning. They are heavy, dense, and capable of damaging weak packaging. They can also rust if exposed to moisture. For global logistics, the practical priorities are weight distribution, moisture control, carton strength, pallet stability, clear labeling, and legal compliance.Storage areas should be dry, ventilated, and protected from direct water exposure. Cartons should not be placed directly on wet floors. In coastal warehouses near ports such as Qingdao, Shanghai, Singapore, Rotterdam, Hamburg, Jebel Ali, Los Angeles, Vancouver, Santos, or Cape Town, humidity control is especially important. Long-term storage may require sealed bags, desiccants, or periodic inspection.Transportation planning should account for the density of steel. A small package may exceed courier weight limits. For e-commerce sellers, 500g, 1kg, and 2kg packages are common because they are easier for customers and fulfillment centers to handle. For wholesale shipments, 20kg or 25kg cartons may be practical, but carton strength and worker safety should be considered.Local regulation compliance is essential. Slingshots and slingshot ammunition may be treated differently around the world. Some places allow recreational target use, while others restrict sale, possession, import, public carrying, or use in parks and urban areas. Importers should consult local authorities, customs brokers, legal advisers, and retail platform policies before placing orders. Product descriptions should avoid unsafe claims and should clearly position the balls for lawful target practice or approved outdoor sporting use.Compliance AreaWhat to CheckGlobal Market ExampleBuyer ResponsibilityRisk Reduction StepImport rulesCustoms classification and restrictionsEU, US, UK, Canada, Australia, GCCConfirm before shipmentUse experienced customs brokerRetail saleAge limits and platform policiesAmazon, local sporting goods chainsFollow marketplace rulesAdd clear product labelingPublic useLocal laws on slingshotsCities, parks, schools, public landWarn end usersInclude safe-use instructionsTransportationWeight, packaging, and documentationSea, rail, truck, courierPrevent cargo damageUse reinforced cartonsStorageHumidity and rust preventionCoastal warehousesMaintain product conditionUse sealed bags and desiccantsEnvironmental rulesPackaging and coating requirementsEU sustainability policiesMeet local standardsChoose cleaner packaging optionsIn 2026, policy trends are expected to emphasize product responsibility, traceable supply chains, safer retail listings, and more sustainable packaging. Buyers should prepare for stronger documentation requests from distributors, customs officials, and online platforms. Clear batch records, material declarations, packaging specifications, and quality inspection reports can help reduce delays.SDBALLS Industry Corp, also known as Shandong SDBALLS Industry Corp Ltd., is a professional precision steel ball manufacturer and integrated supply partner based in Tai’an City, Shandong Province, China. With manufacturing experience dating back to 1996, the company serves customers in more than 50 countries and supports both industrial and outdoor product markets.From a technological capability perspective, SDBALLS focuses on controlled steel ball production across carbon steel, chrome steel, and stainless steel materials. The company offers grades from G10 to G1000, allowing buyers to select the right tolerance level for bearing components, mechanical systems, general hardware, grinding applications, and outdoor steel shot products. Its quality systems are supported by IATF 16949, ISO 9001, and ISO 14001 certifications. Buyers interested in quality control methods can review the company’s quality and technical capabilities.From a manufacturing capability perspective, SDBALLS operates three production facilities with annual capacity exceeding 5,000 tons. This scale supports stable supply for global distributors, private-label brands, industrial users, and high-volume buyers. The company manufactures carbon steel balls, chrome steel balls, stainless steel balls, and lead-free steel shot solutions for hunting and outdoor markets, including annealed and plated shot options that can meet defined hardness requirements for regulated markets.From a service capability perspective, SDBALLS works as more than a single-product factory. It also helps buyers consolidate sourcing for multi-material spheres such as plastic, glass, ceramic, copper, and aluminum balls. This integrated supply model can simplify procurement for importers and OEM customers that need multiple spherical components from one coordinated partner. To understand the wider scope of fields served, buyers can explore the company’s application solutions.For global steel ball sourcing, reliable communication and long-term consistency matter as much as unit price. SDBALLS supports international customers through a dedicated sales team and overseas business support, helping buyers coordinate specifications, samples, packing, inspection, and logistics. More background is available on the company’s corporate profile.An 8mm steel ball usually weighs about 2.05 to 2.10 grams, depending on material density, tolerance, and coating. Carbon steel, chrome steel, and stainless steel versions are all close in weight, though exact values vary slightly by alloy.Yes. For lawful recreational target shooting, 8mm is a balanced size. It is heavier and more stable than 6mm, easier to use than 10mm for many people, and compatible with many medium bands.Carbon steel is usually better for low-cost bulk practice. Stainless steel is better when corrosion resistance, clean appearance, and long shelf life are important. Plated carbon steel can be a useful middle option.They can improve consistency, especially for skilled users and premium target products. However, band setup, pouch release, user technique, and surface condition also strongly affect accuracy.Carbon steel and chrome steel balls can rust if exposed to moisture. Anti-rust oil, plating, sealed packaging, desiccants, and dry storage help reduce corrosion. Stainless steel provides better resistance in many environments.For bulk shipment, strong inner bags, reinforced cartons, moisture protection, pallet wrapping, and clear weight labels are recommended. For retail, sealed jars, pouches, or blister packs should protect against rust and handling damage.No. Laws differ by country and local area. Some places restrict slingshots or ammunition sales, possession, carrying, or use. Buyers and users should check local regulations before importing, selling, or using the product.Retail labels should include size, material, quantity or weight, safety warnings, eye protection advice, age guidance where required, intended lawful target-use positioning, batch information, and supplier details.Compare material, diameter tolerance, surface finish, rust protection, packaging strength, sample consistency, certifications, production capacity, communication quality, and total landed cost rather than only the lowest unit price.Important trends include more sustainable packaging, cleaner coatings, better traceability, stronger marketplace compliance, improved automated inspection, and demand for stable suppliers that can support global logistics and documentation.